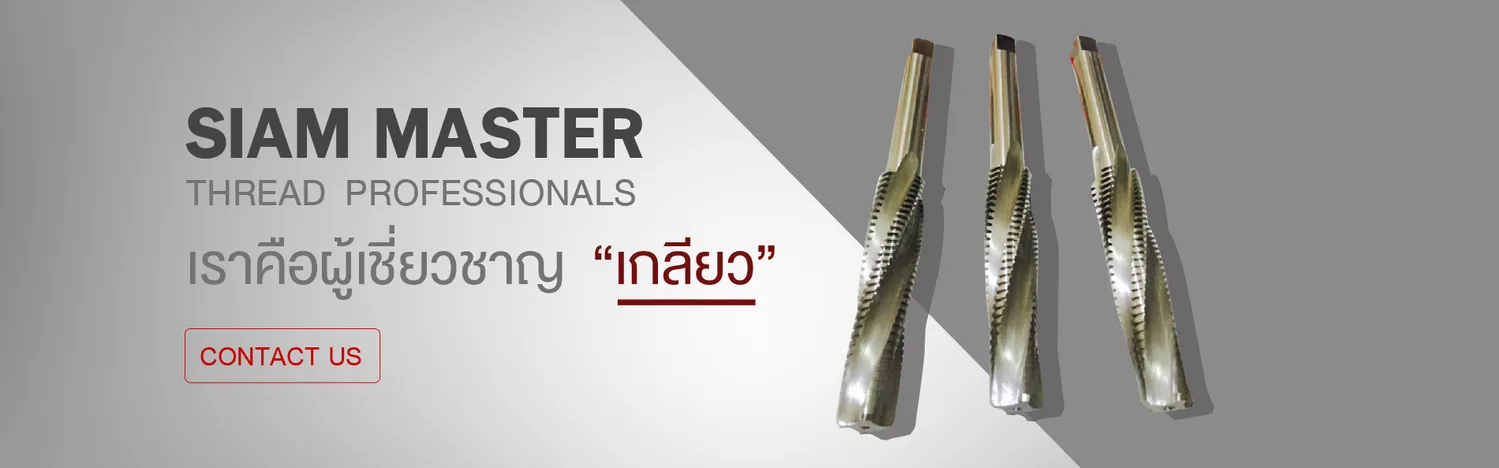
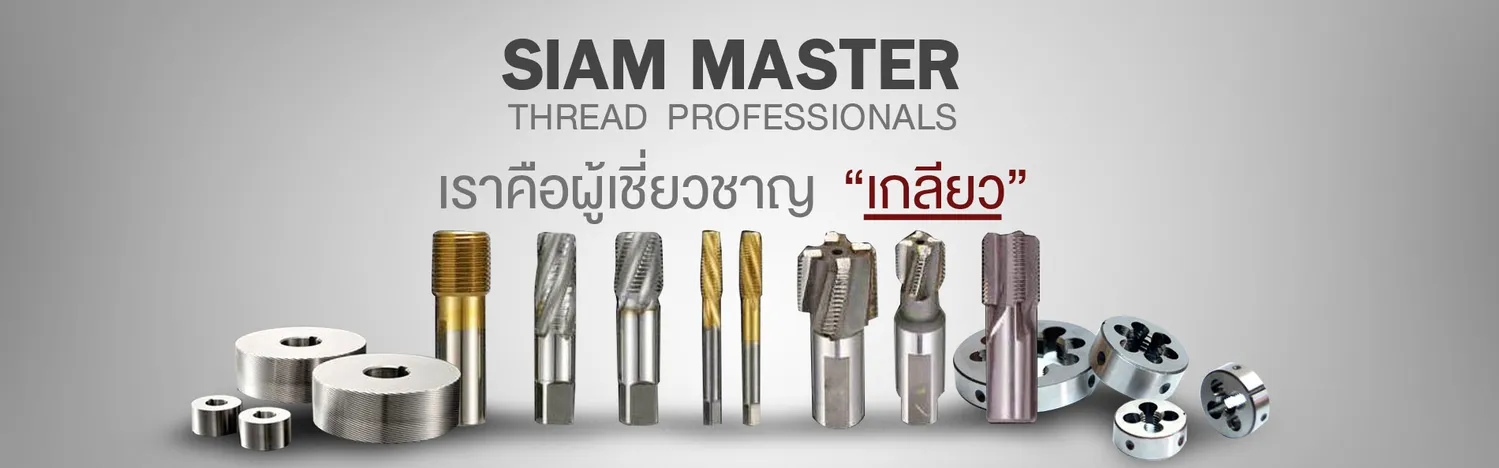
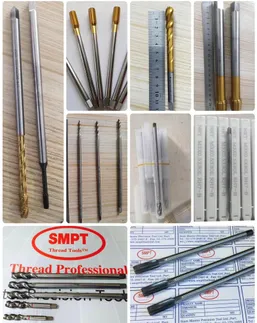
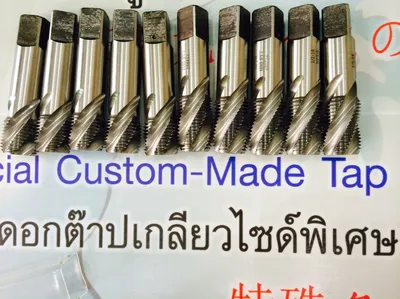
ผลิต-จำหน่าย ดอกต๊าปเกลียว ขนาดตามสั่ง Custom-Made Tap
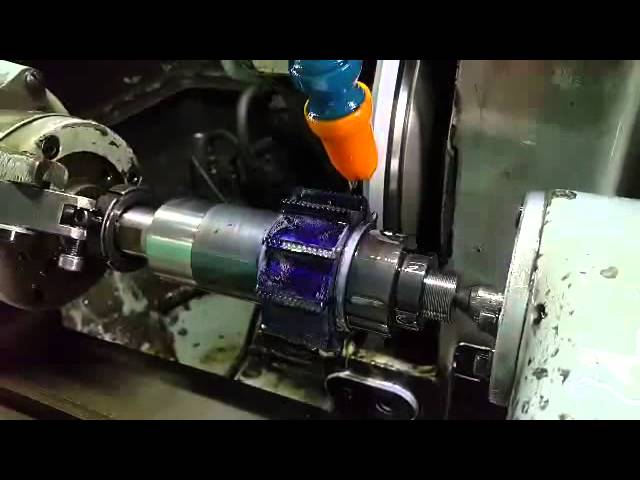
Grinding Machine: Special Taps Custom-Made Taps manufacturer in Thailand
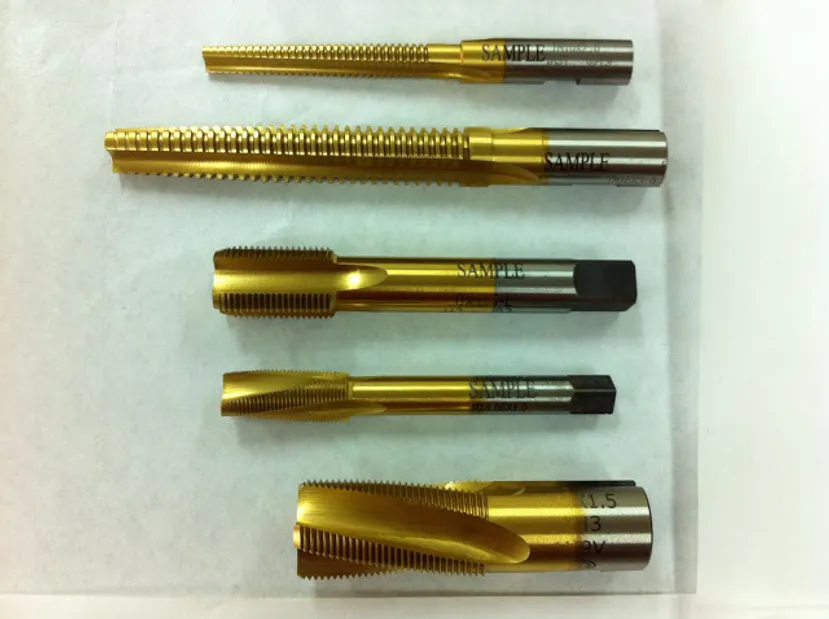
ดอกต๊าปเกลียวคุณภาพสูง HI-Quality Premium Material
(ทนทาน เหมาะสำหรับชิ้นงานเหล็กแข็ง)
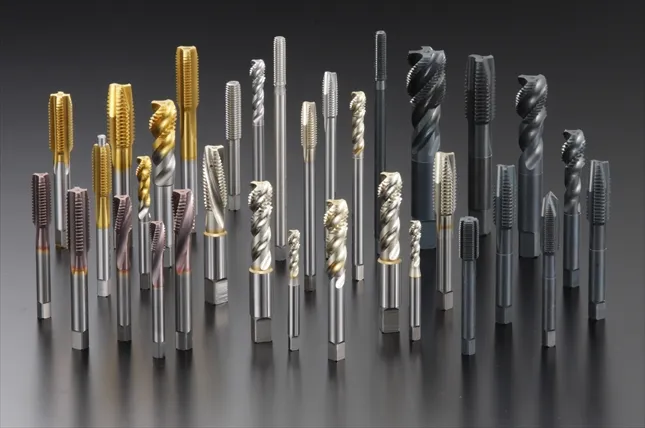
Special Taps (ISO JIS DIN )ผลิตดอกต๊าปเกลียวทุกรุ่นทุกขนาด ตามสั่ง เกลียวมิล เกลียวนิ้ว เกลียวท่อ เกลียวพิเศษ Material : Carbide , HSSe, AISI M42, JIS SKH59 DIN 1.3343,SKH-9 (Special Taps | Custom Taps)
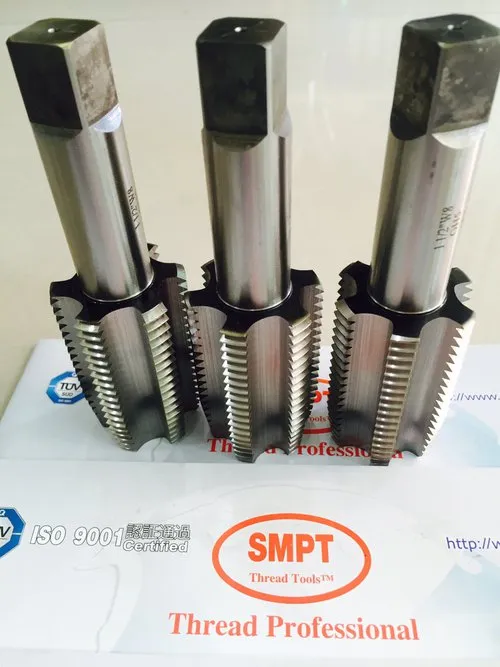
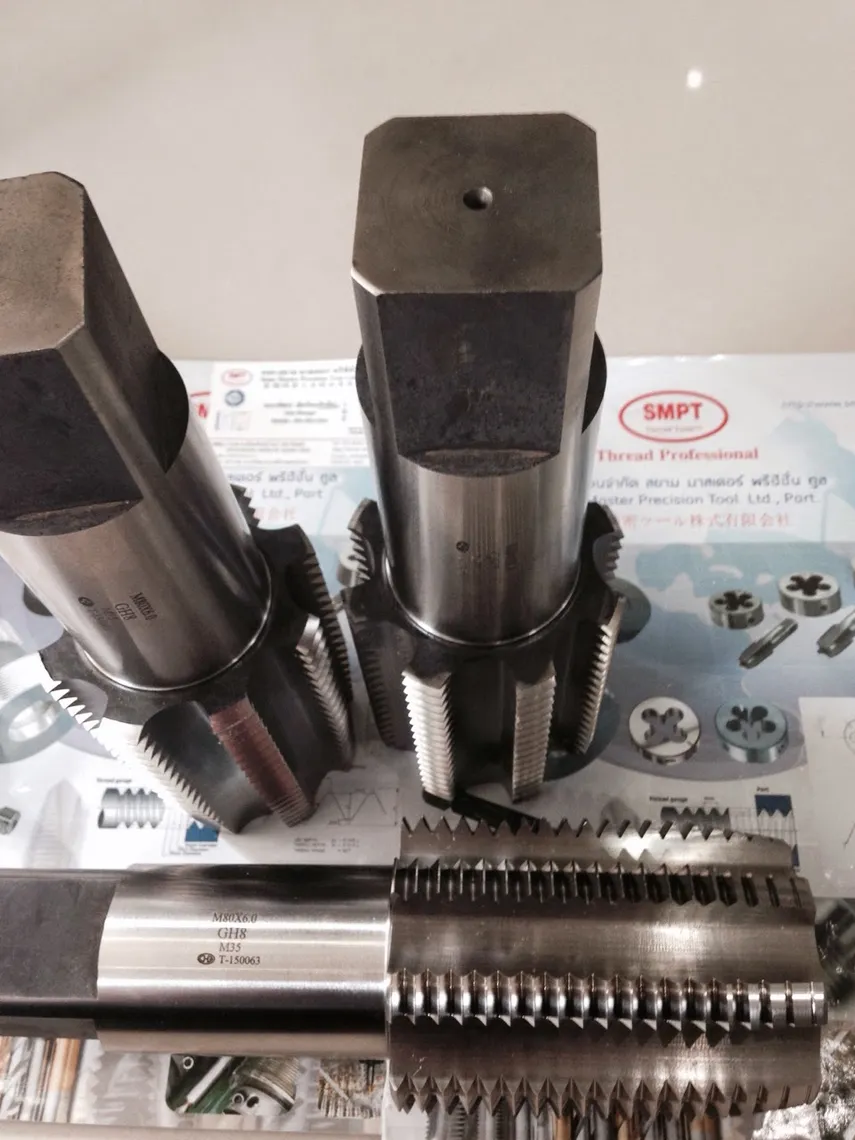
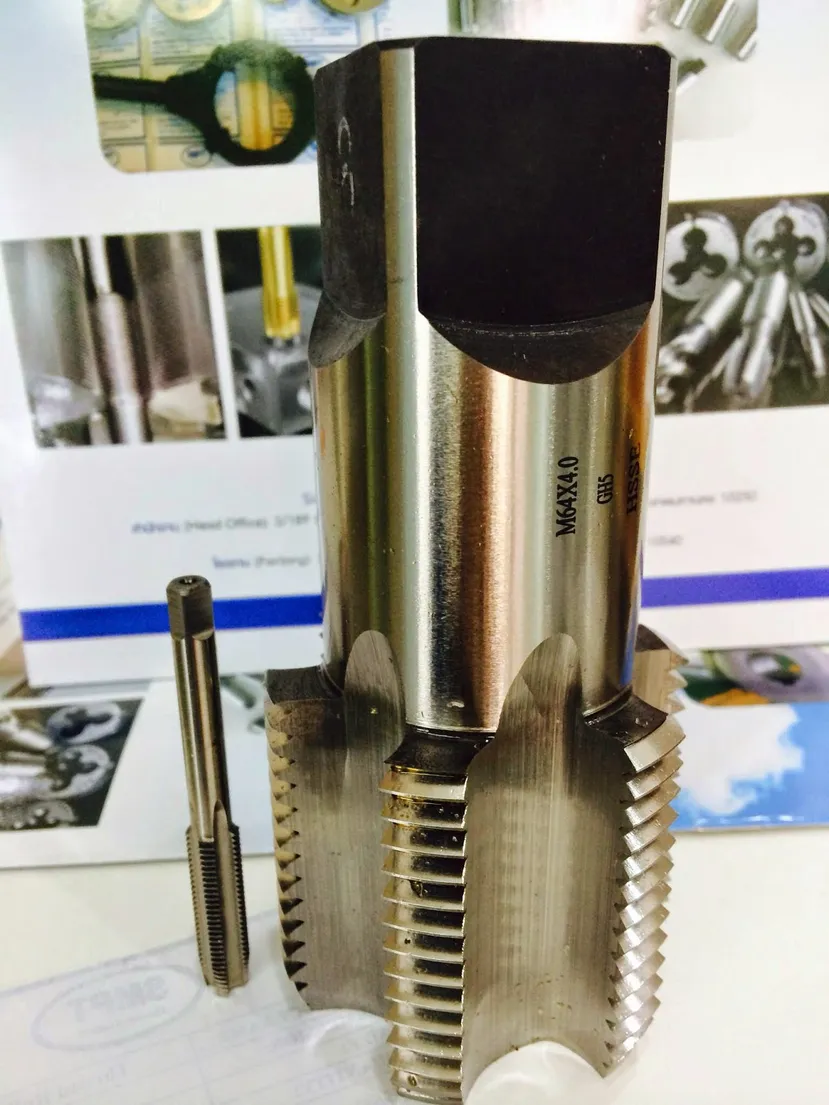
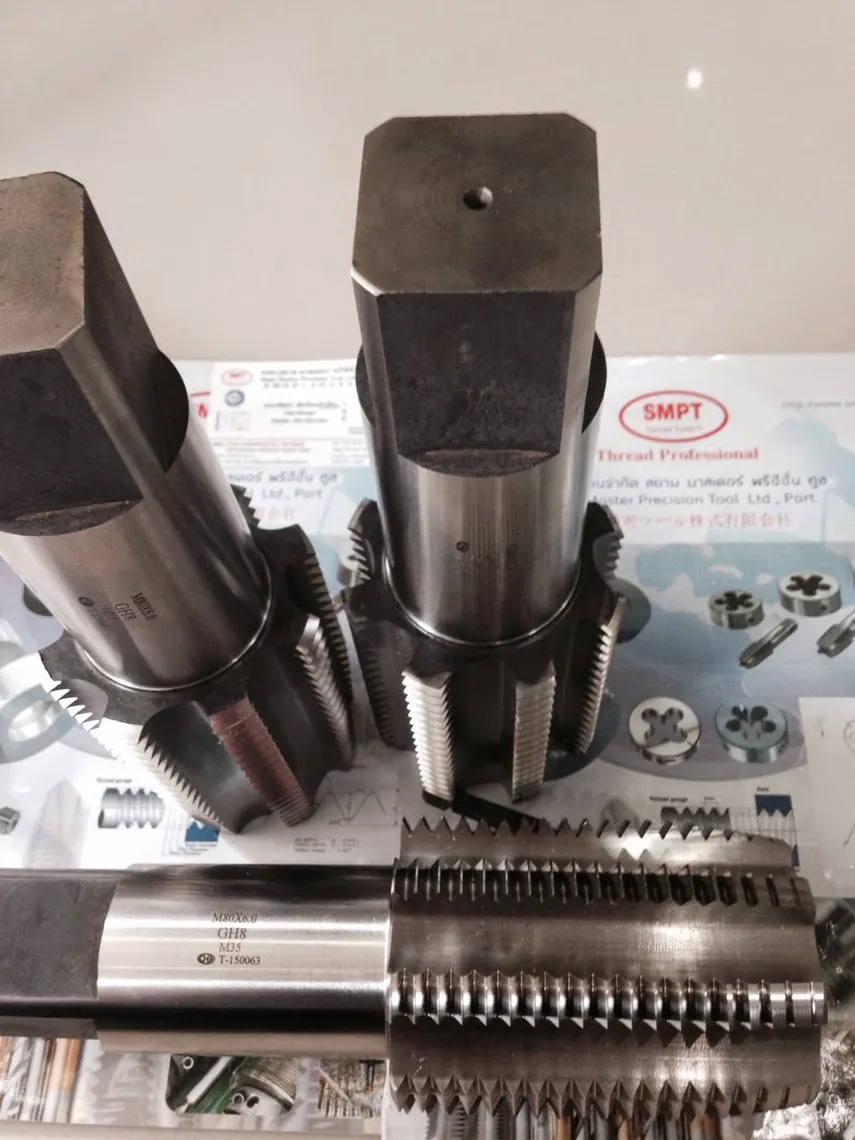
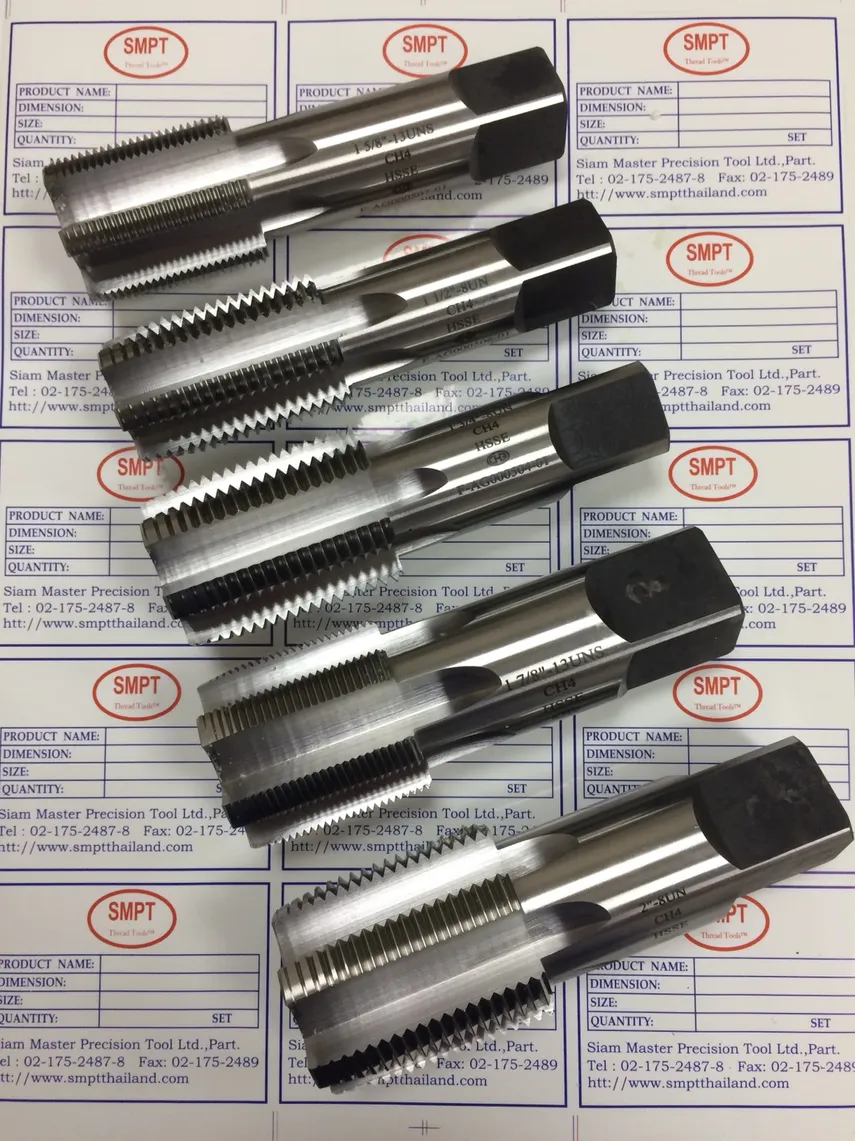
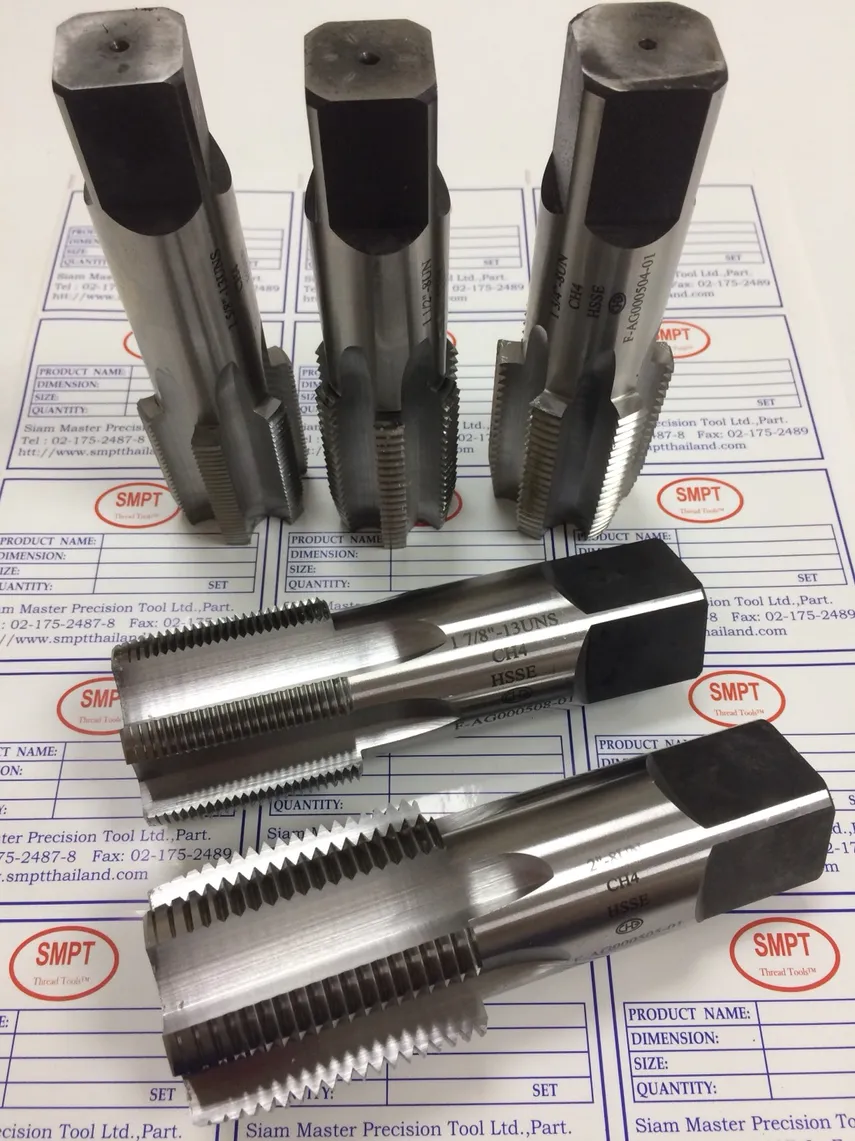
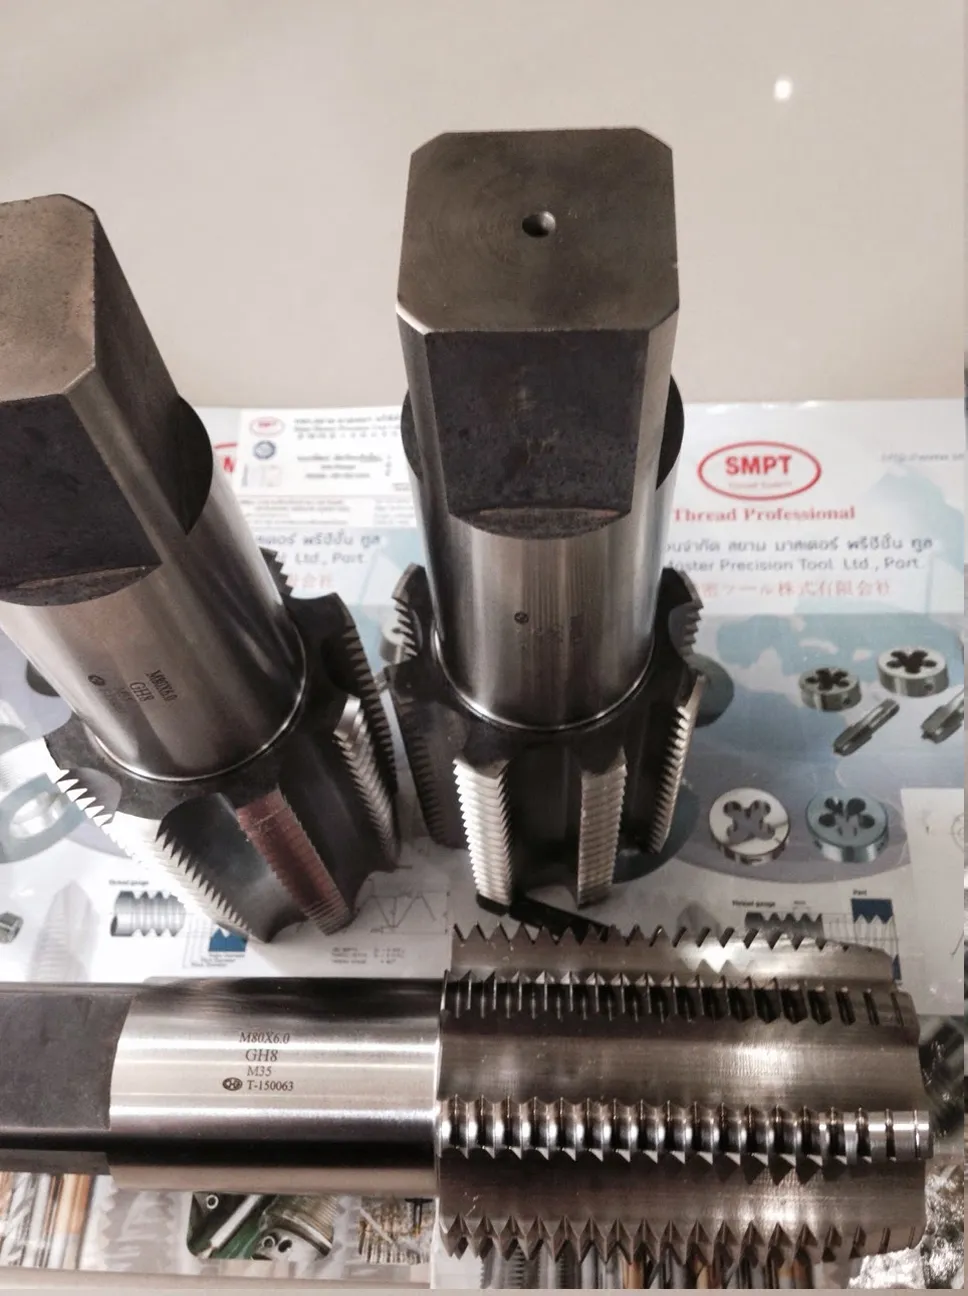
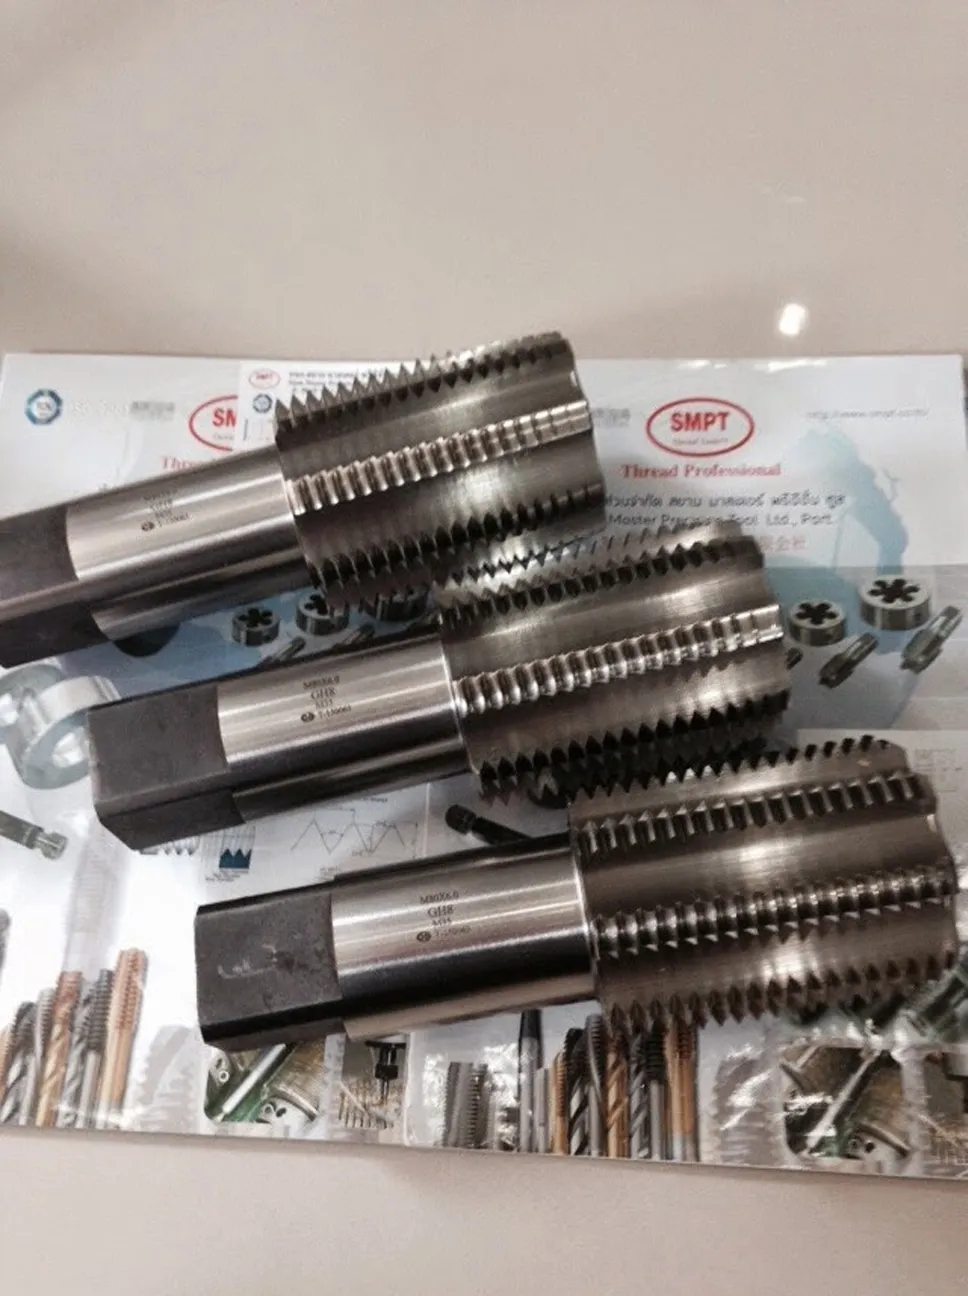
Large Size Small Size Extension Longshank Oversize Undersize Special Size Thread Taps Special Taps | Custom Taps World-class performance in large diameter taps with standard or non-standard thread forms Special Taps Large diameter taps, over size in diameter, are used to tap new holes and clean rough or rusty threads
Standard: ISO DIN JIS GB BS ANSI
ดอกต๊าปเกลียวพิเศษ สั่งทำ เกลียวโอเว่อร์ไซด์ เกลียวใหญ่ เกลียวแปลกๆ ดอกต๊าปเกลียวซ้าย ที่ไม่มีในท้องตลาด เกลียวพิเศษ
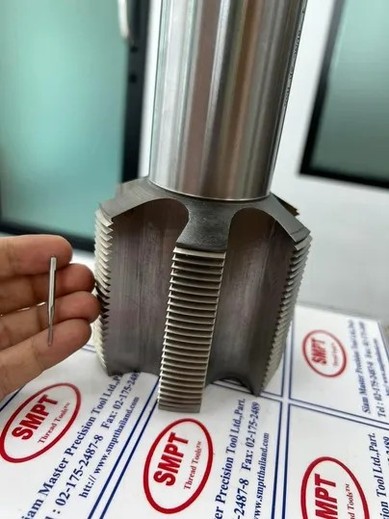
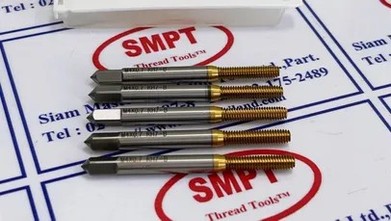
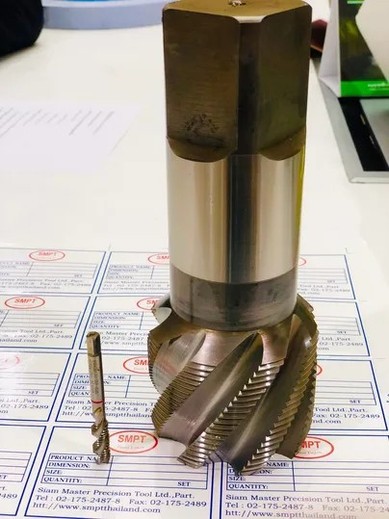
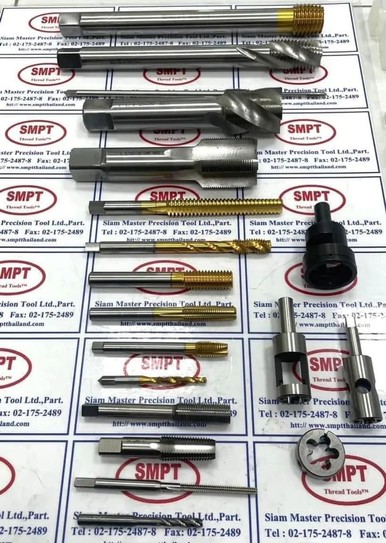
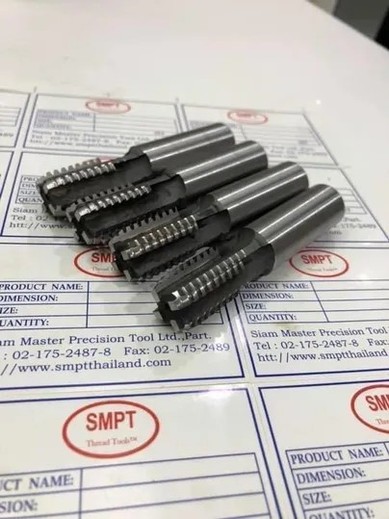
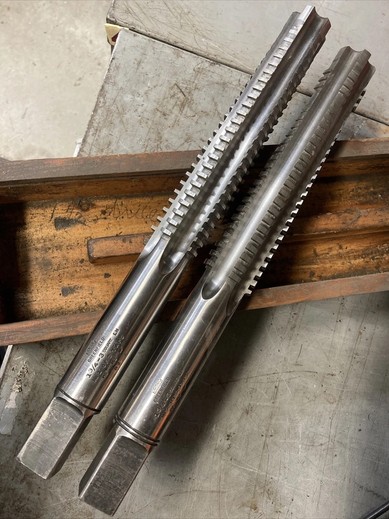
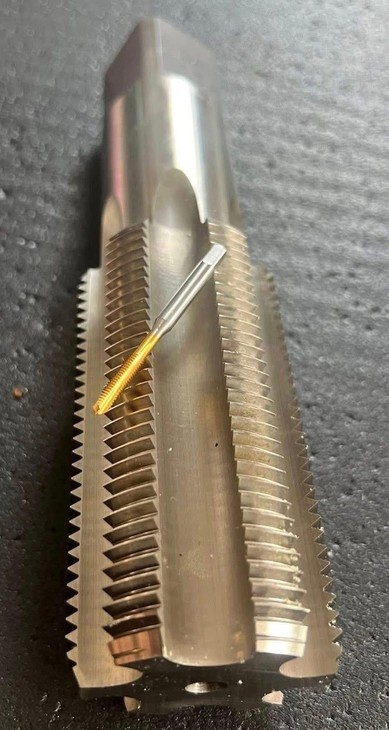
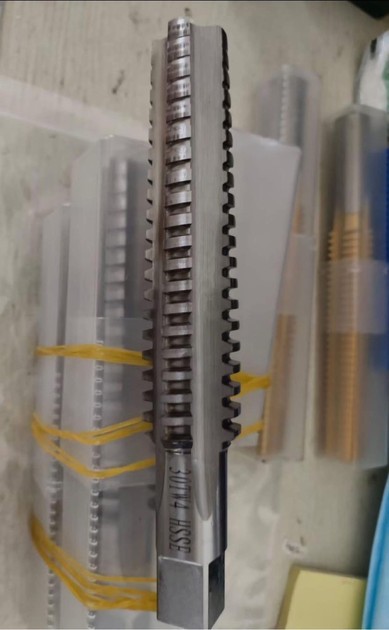
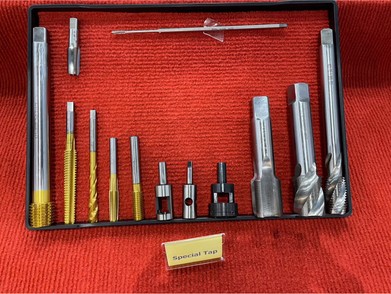
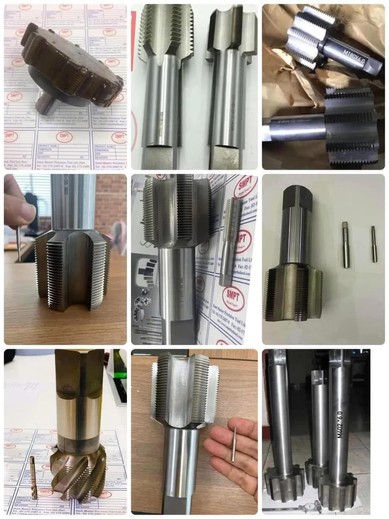
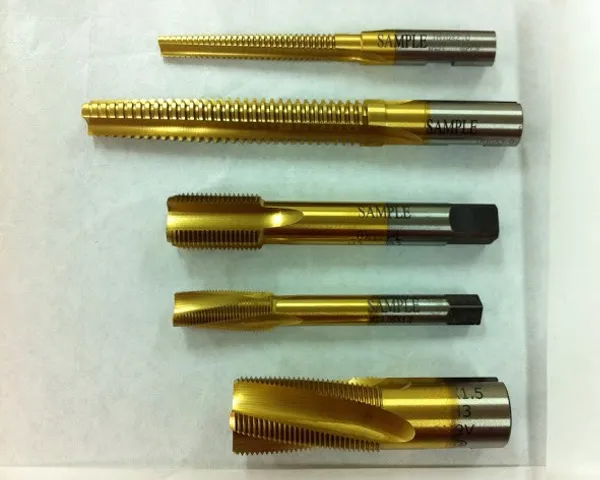
ดอกต๊าปเกลียวพิเศษตามสั่ง
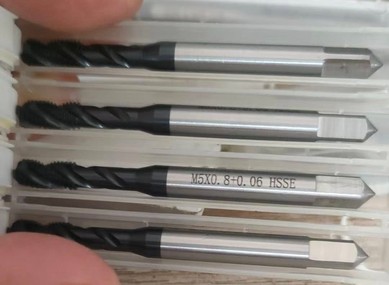
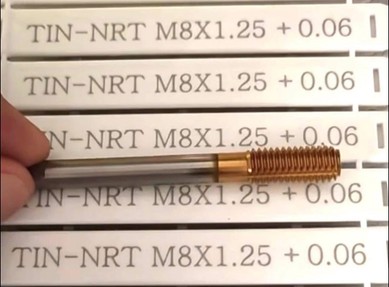
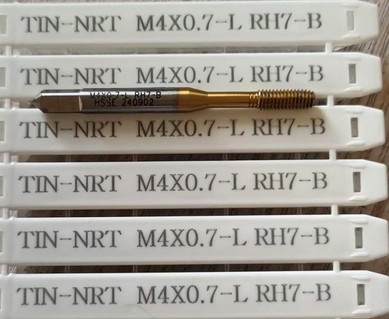
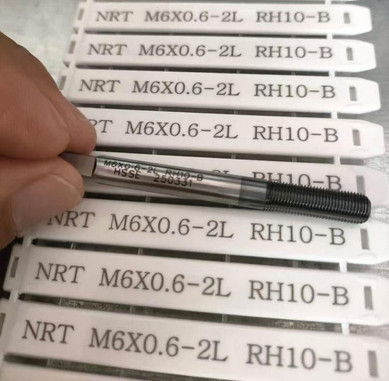
ดอกต๊าปเกลียวประเทศไทย SMPT OSG YAMAWA Thailand Taps Thread Spiral Taps
✅ Oversize Pitch Diameter Taps
สำหรับงานที่ต้องการขนาดเกลียวใหญ่พิเศษ เช่น งานชุบหรืออบความร้อนหลังการต๊าป
✅ Double Lead Taps
เพิ่มประสิทธิภาพการต๊าปด้วยเกลียว2 ปาก เพื่อให้เกลียวหมุนเร็ว2 เท่า
✅ Left Helix Taps
ดอกต๊าปเกลียวซ้าย
✅ Special Custom-Made Taps
ผลิตตามแบบ Drawing หรือชิ้นงานตัวอย่าง รองรับทุกขนาด ทุกวัสดุ ทั้ง Carbide, HSSe, M42
รับผลิตตามสั่ง | คุณภาพระดับสากล | มาตรฐาน ISO / DIN / JIS
📞 Tel: 02-175-2487
🌐 www.smptthailand.com
📧 Email: rollingdie@gmail.com
คุณสมบัติของดอกต๊าปเกลียวคุณภาพสูง
1. วัสดุเกรดพรีเมียม: HSSe หรือสูงกว่า
• HSSe (High-Speed Steel with Cobalt) มีความแข็งแรงและทนความร้อนสูง
• เหมาะสำหรับงานต๊าปที่ต้องการความแม่นยำและทนต่อแรงเสียดสี
2. ผ่านกระบวนการชุบแข็งคุณภาพสูง
• ความแข็งระดับ HRC 64–65 เป็นมาตรฐานที่ทำให้ดอกต๊าปสามารถตัดเกลียวได้แม้ในโลหะที่แข็ง
• ต้องควบคุมอุณหภูมิและเวลาอย่างแม่นยำ เพื่อไม่ให้เกิดความเปราะ
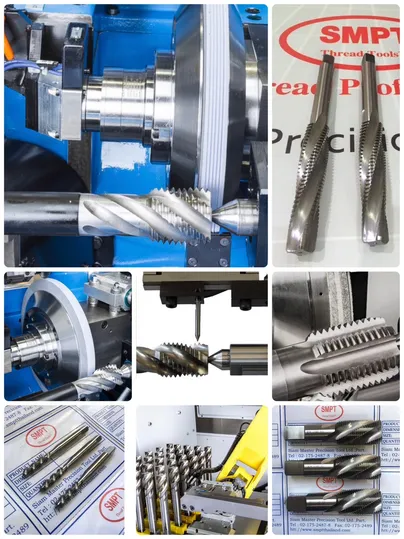
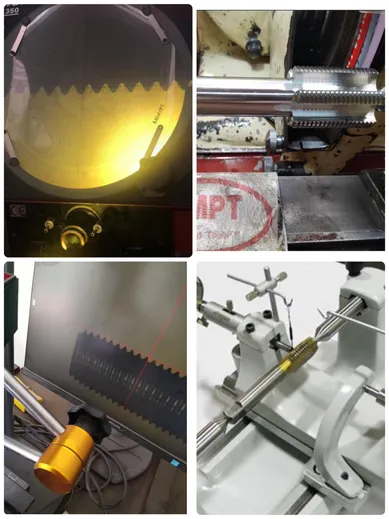
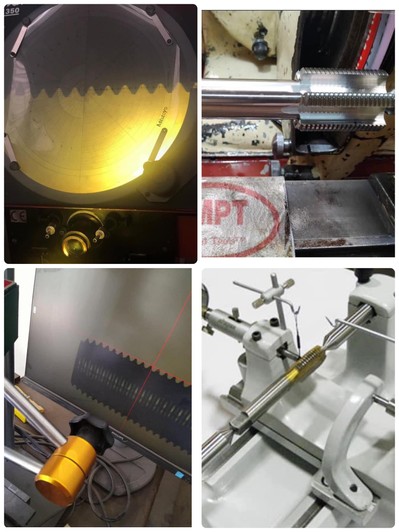
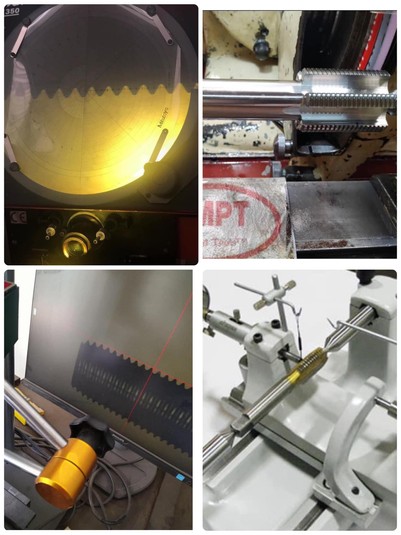
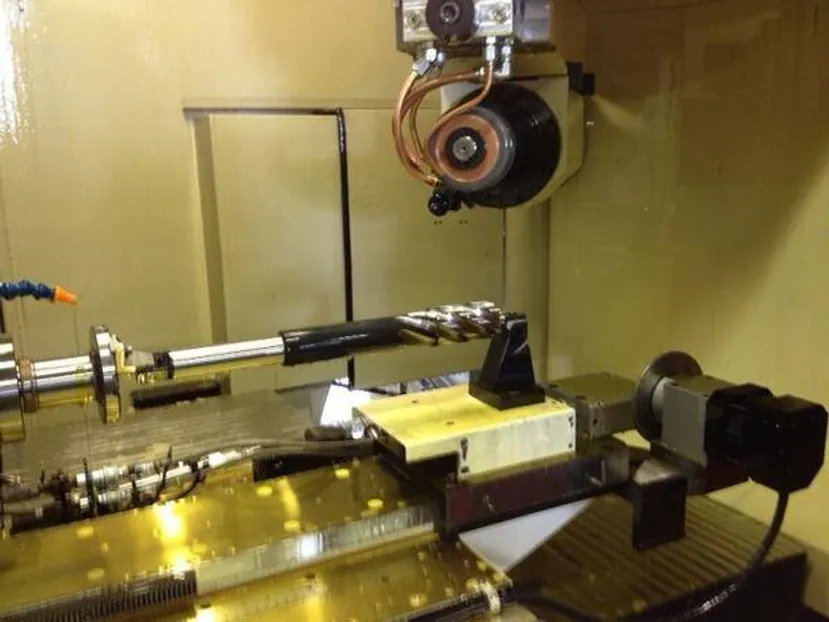
3. เจียรผิวและเกลียวด้วยเครื่องเจียรพิเศษ
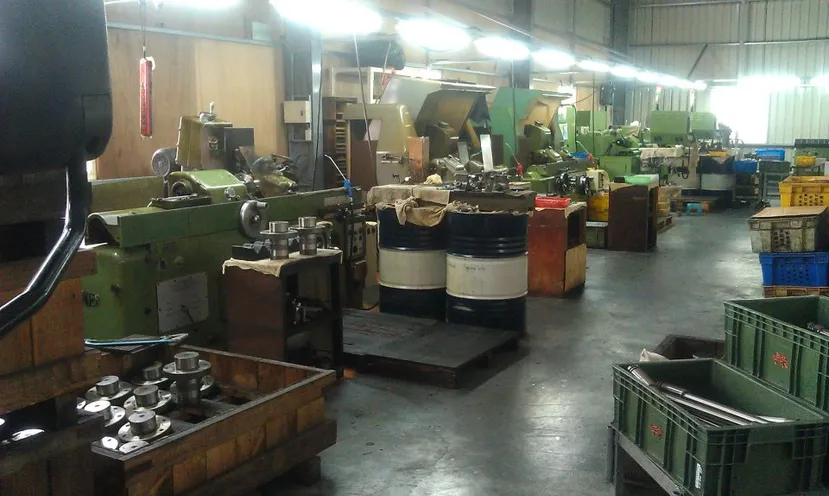
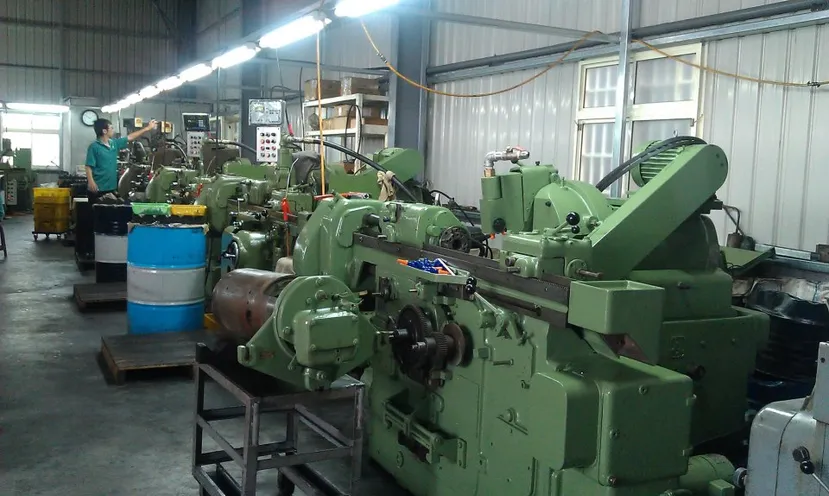
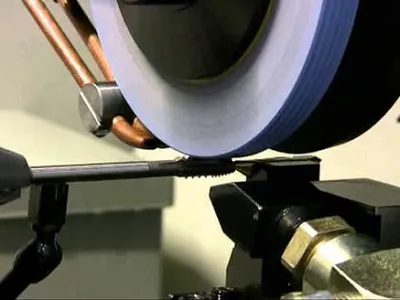
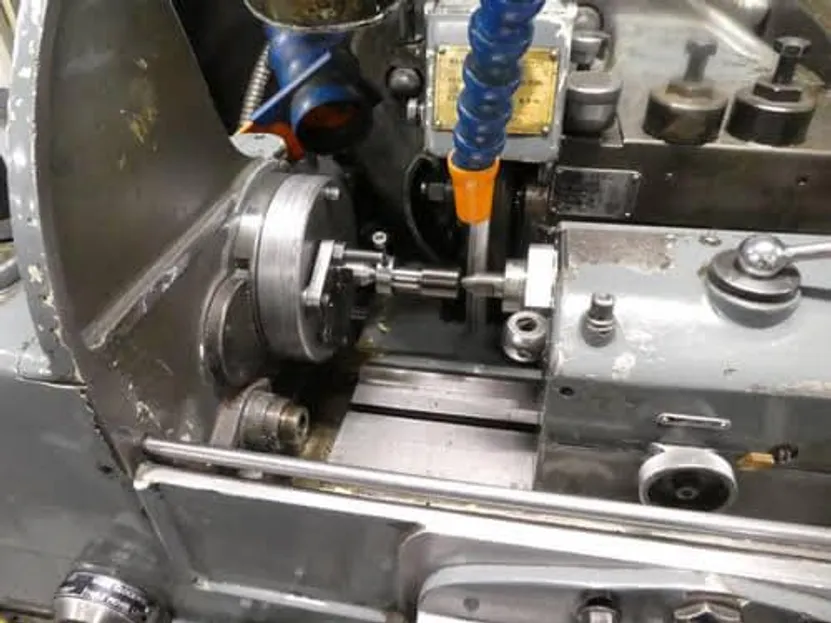
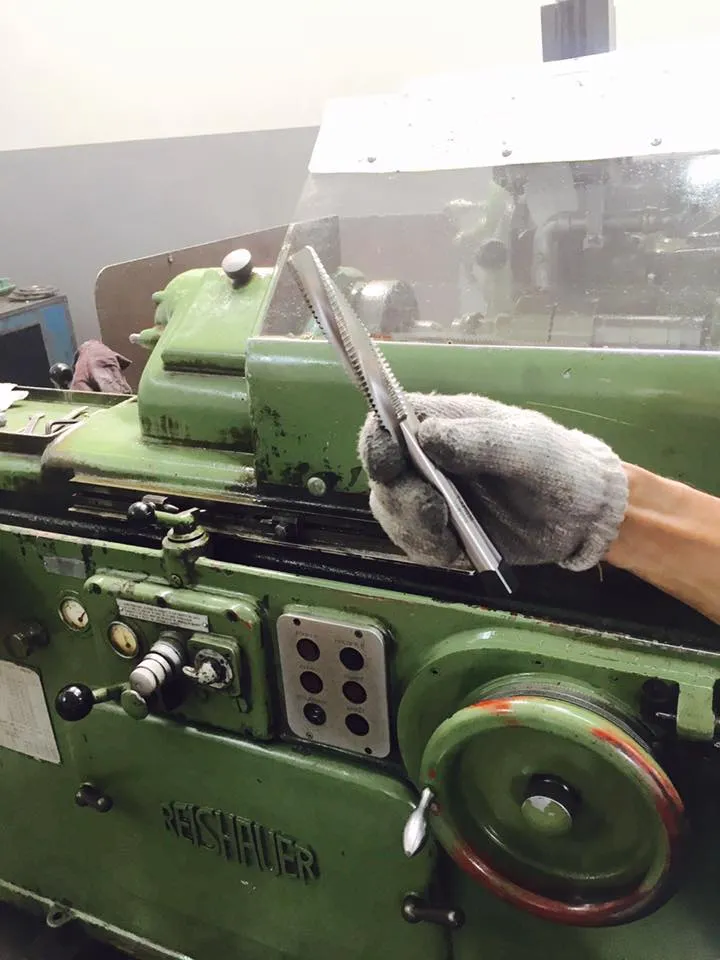
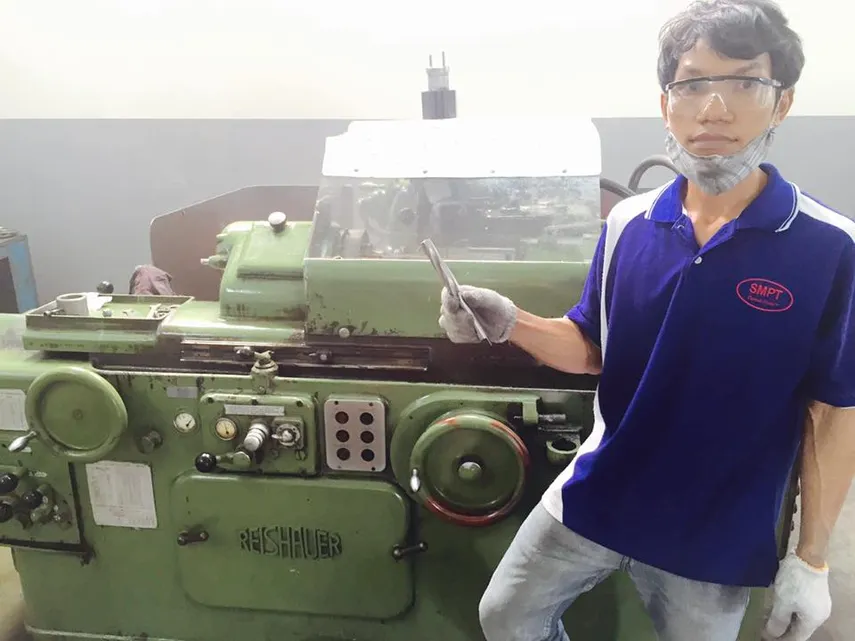
• ใช้เครื่องเจียรเกลียวระดับโลก เช่น Reishauer NRK, MATRIX 46 จากสวิตเซอร์แลนด์และอังกฤษ
• ทำให้เกลียวคม เรียบ และมีความแม่นยำสูง ลดแรงต้านขณะต๊าป
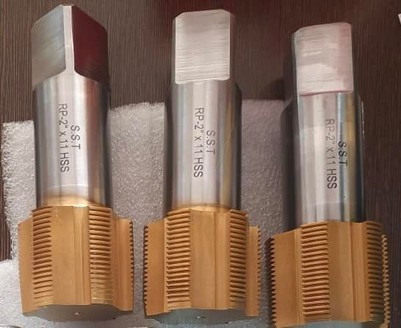
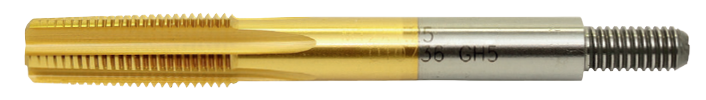
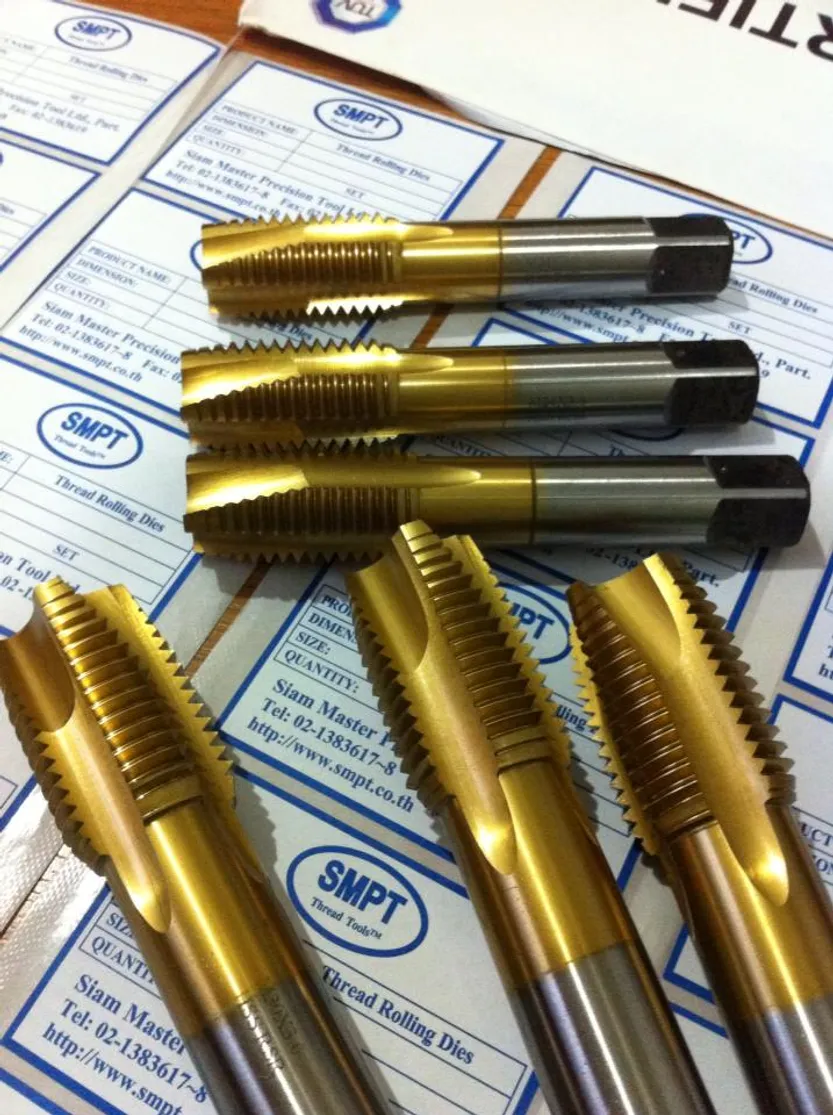
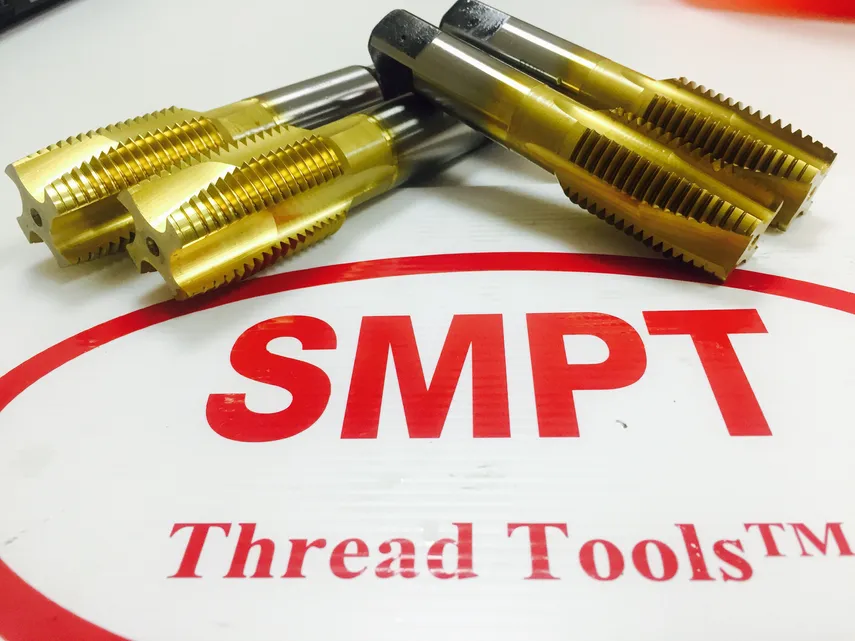
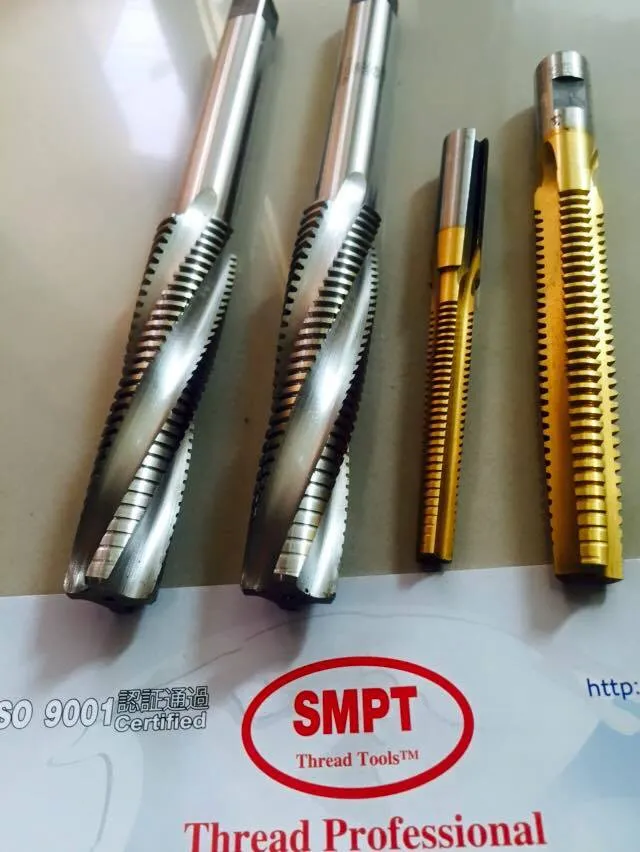
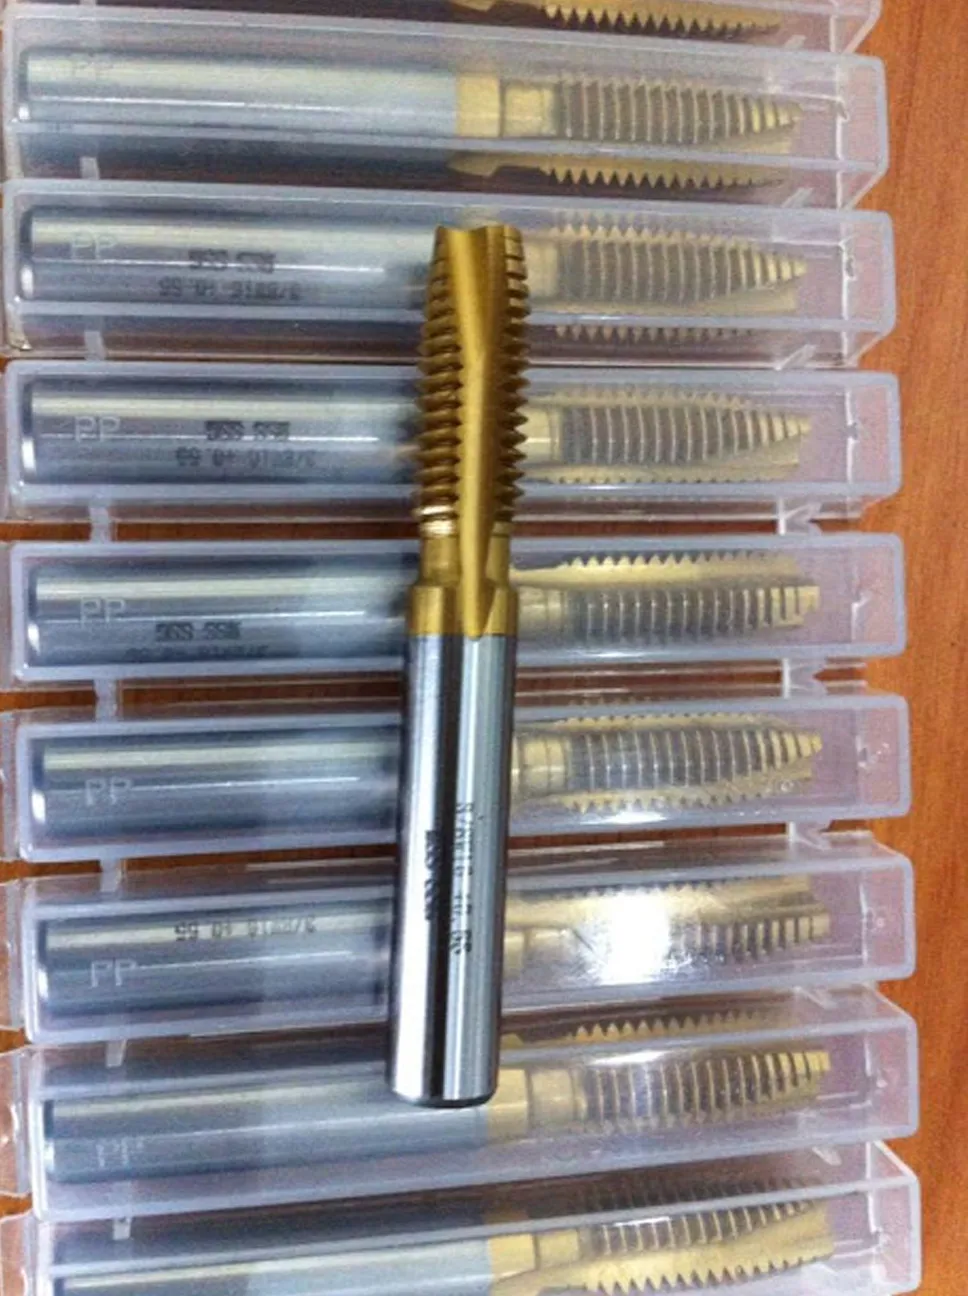
4. เคลือบไทเทเนียม (TiN Coating)
• เพิ่มความทนทานต่อการสึกหรอ
• ลดแรงเสียดทาน ทำให้ต๊าปได้ลื่นขึ้น
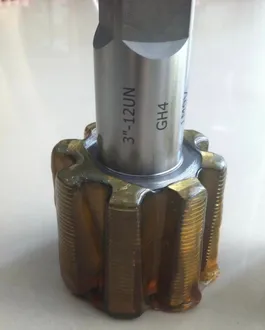
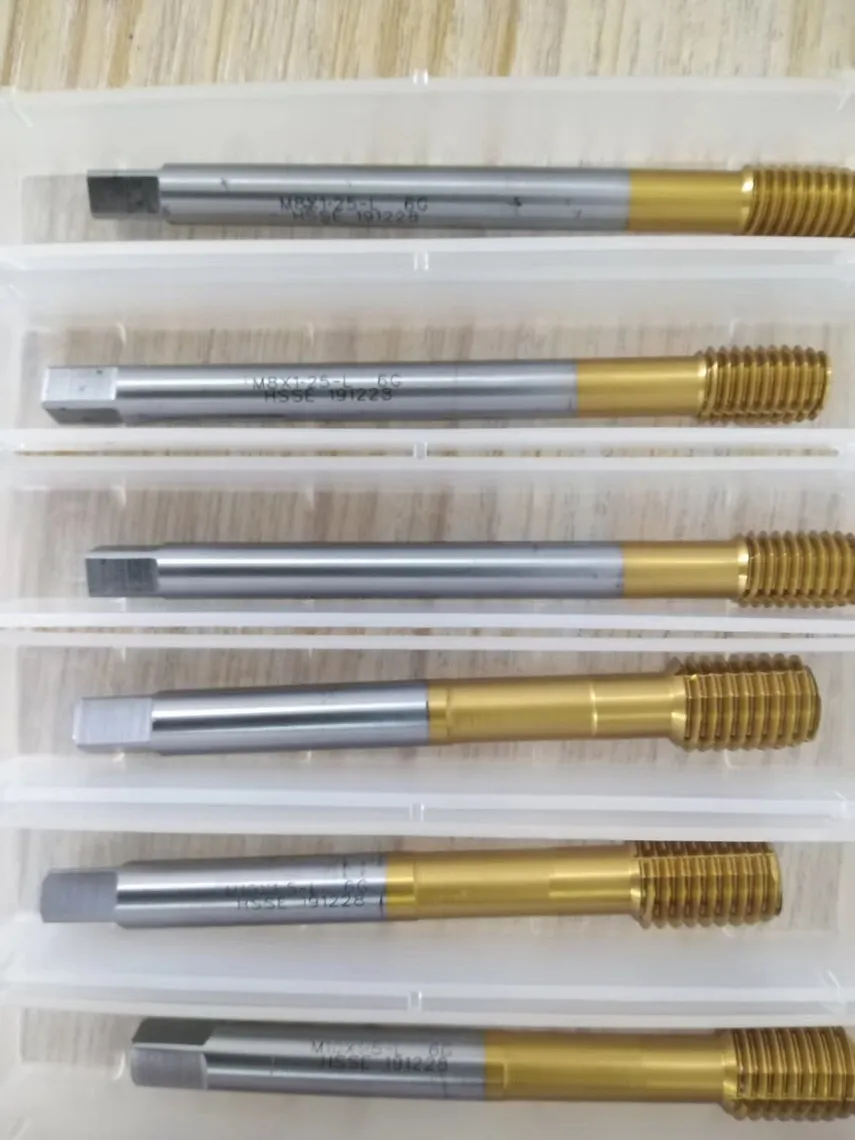
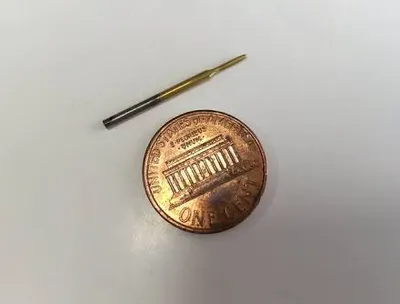
• สีทองที่เห็นเป็นผลจากการเคลือบไทเทเนียม B
5. สามารถสั่งผลิตขนาดพิเศษ (Custom-Made)
• เกลียวซ้าย เกลียวใหญ่ เกลียวแปลกที่ไม่มีในท้องตลาด
2. REISHAUER UL Thread Grinders (Switzerland)
3. REISHAUER US Thread Grinders (Switzerland)
4. MATRIX Universal thread grinder MATRIX 46 (UK)
Large Diameter Taps or Extended Length Taps
Custom-made Taps
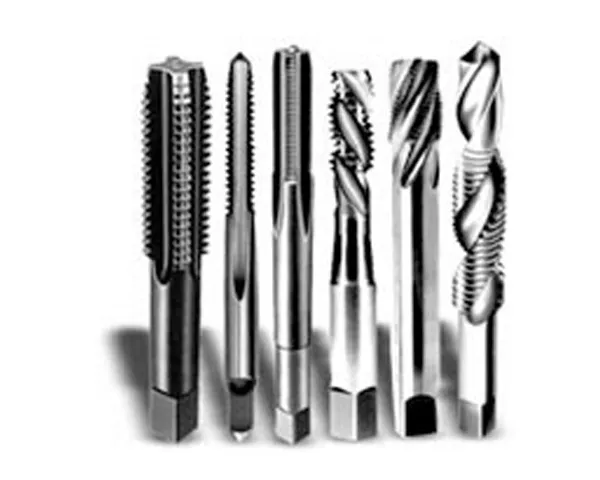
1.ต๊าปร่องเลื้อย (Spiral Flute Taps)2. ต๊าปร่องเฉียงปลาย (Gun Point Tap)3.ต๊าปร่องตรง (Straight Flute Taps)4.ต๊าปไร้เศษ (Roll Taps)
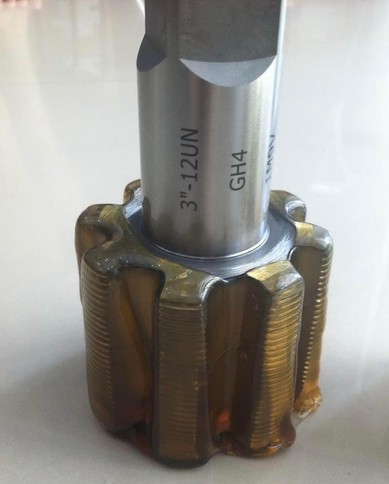
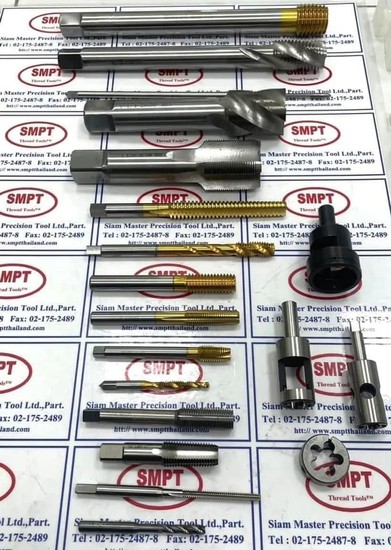
ดอกต๊าปเกลียว (Taps) คืออะไร ดอกต๊าปเกลียว (Tapping) หรือ ดอกต๊าป เป็นอุปกรณ์ที่ใช้สำหรับการสร้างเกลียวให้กับชิ้นงานด้วยกระบวนการต๊าป โดยการตัดเกลียวในภายในรูของชิ้นงาน
(ทางเรารับผลิตดอกต๊าปเกลียว ทุกรุ่นทุกขนาด วัสดุ Carbide /HSSe/ HSS/M2/ 3343 /Coating TiN เพียงแค่มี Drawing หรือตัวอย่างชิ้นงาน)
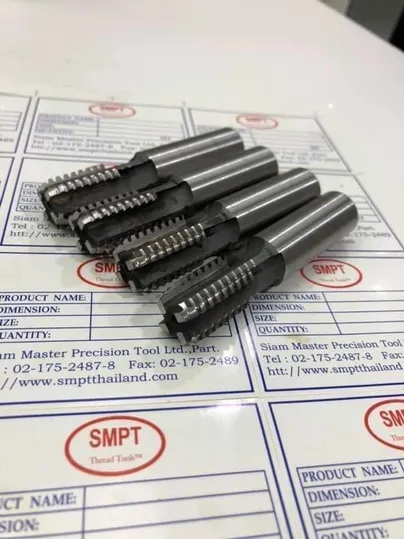
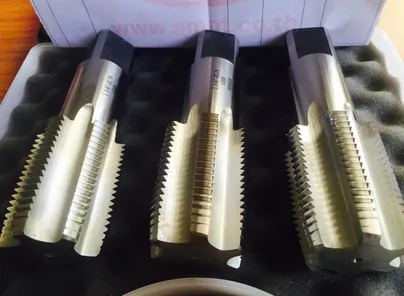
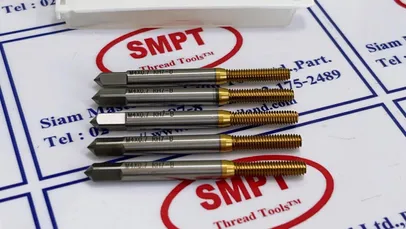
Special spiral tap, made to order, overside spiral, large spiral, strange spiral, left-hand spiral tap That is not available in the market, special thread (just have a drawing or sample) Material : Carbide , HSSe, AISI M42, JIS SKH59 DIN 1.3343,SKH-9
taps, spiral taps Drill thread tap Spiral tap, hand tap, tap for solid tap, hand tap, machine tap, hi-speak tap, 3 taps, tap set, machine tap, tap HSS. left-hand thread tap, hand tap, machine tap, machine tap, threaded tap, brass joint brass threaded fitting Internal thread, external thread, inch thread, oblique tapered thread Threading tap for tapping brass joints Brass Fitting Tap
ดอกต๊าปเกลียวประเทศไทย SMPT OSG YAMAWA Thailand Taps Thread Spiral Taps
ดอกต๊าปเกลียว ( Tap) อุปกรณ์ชนิดหนึ่งที่ทำให้เกิดรูหรือเกลียวบนวัสดุ โดยมักจะเรียกว่า การต๊าปเกลียว (Tap) เป็นกระบวนการที่รับความนิยมอย่างมากเพราะทำได้ง่ายและมีประสิทธิภาพสูง โดยดอกต๊าปทำมาจากเหล็กกล้าผสมคาร์บอนและเหล็กกล้าความเร็วรอบสูงผ่านกระบวนชุบและอบคืนตัว ทำให้มีคุณสมบัติที่แข็งมากแต่จะแตกหักง่าย ดังนั้นจึงควรเลือกดอกต๊าปให้เหมาะสมกับการใช้งานและประเภทของวัสดุ
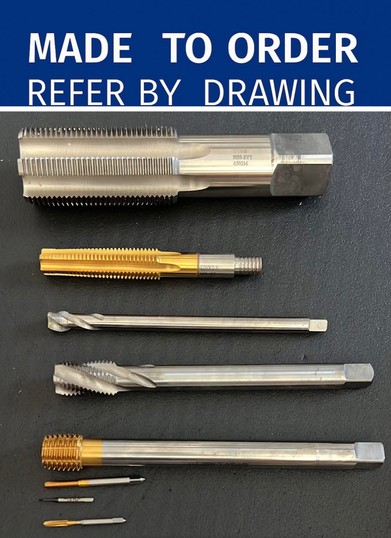
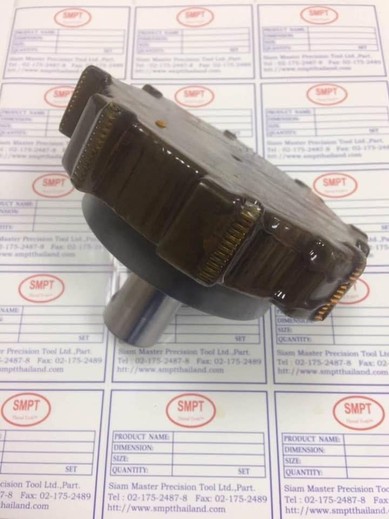
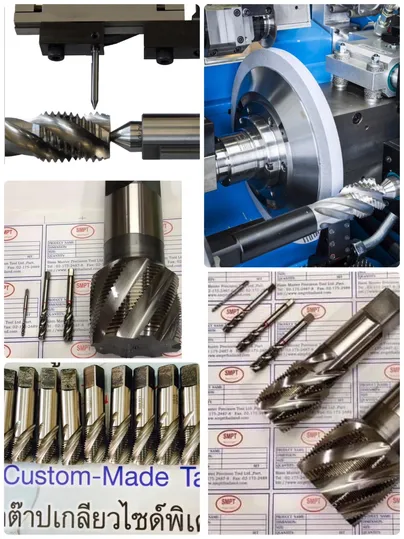
ลูกค้าที่ให้ความไว้ใจในการสั่งทำดอกต๊าปเกลียวพิเศษ

- kundenspezifische Spezialgewindebohrer
- специальные резьбовые метчики
- özelleştirilmiş özel dişli vida muslukları
- 맞춤형 특수 나사산 나사 탭
- tarauds filetés spéciaux personnalisés


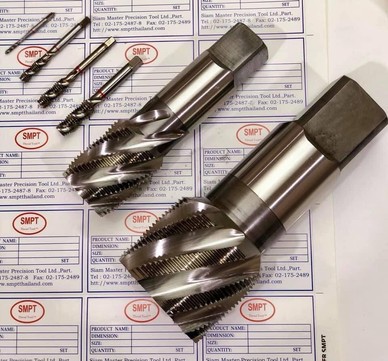
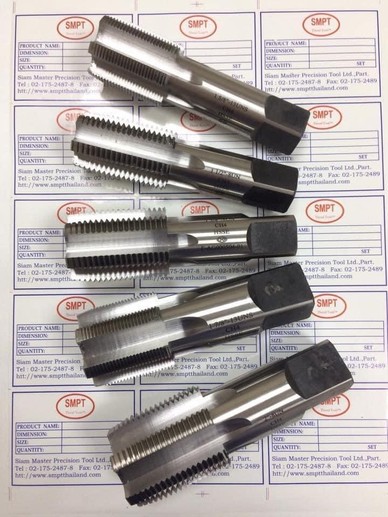
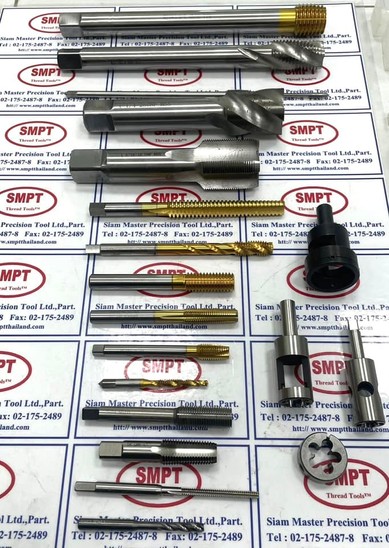
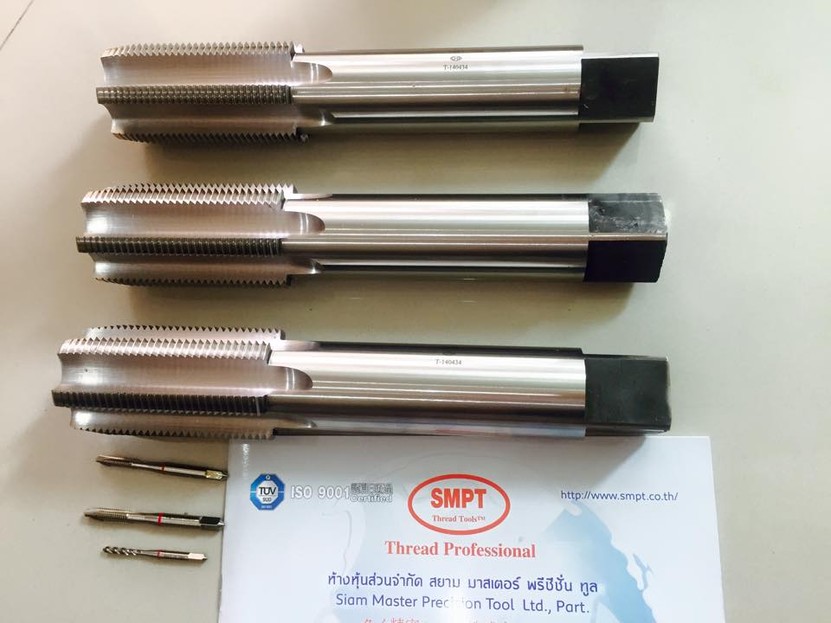
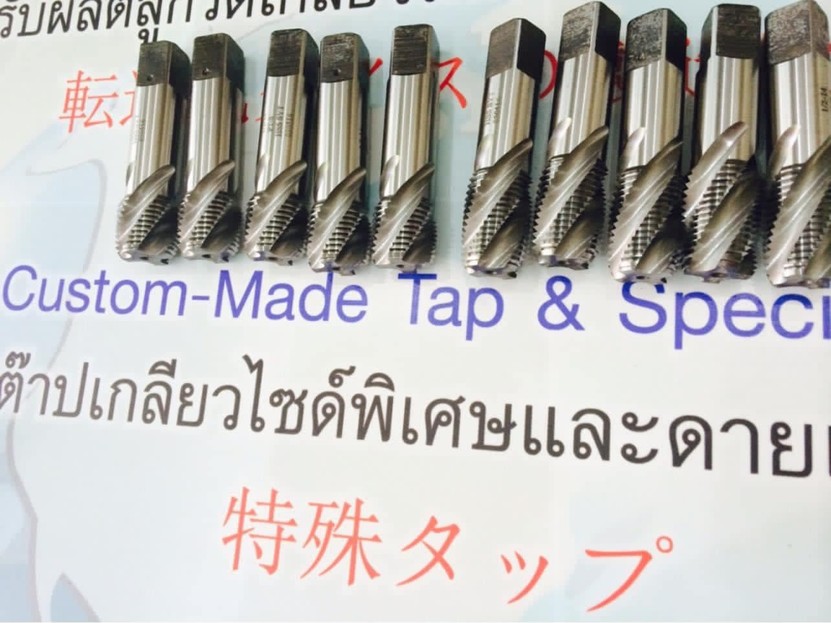
ดอกต๊าปเกลียวพิเศษ
โรงงานทางเราเน้นผลิตดอกต๊าปเกลียวที่เป็นไซด์พิเศษ ขนาดพิเศษ เกลียวพิเศษ ที่ไม่มีในท้องตลาด
>>> คลิก Inquiry Form Quotationดาวน์โหลดแบบฟอร์มเพื่อกรอกข้อมูลขอราคา



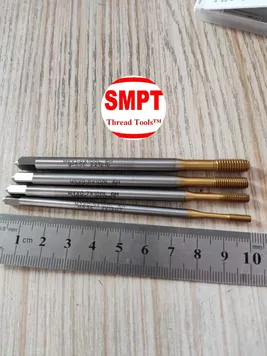
แต่ถ้าเป็นขนาดมาตรฐานทั่วไปไม่ใช่ขนาดพิเศษ ทางเราก็มีผลิตจำหน่าย โดยสามารถคลิกสั่งซื้อได้》》》CLICK》》》
ハンドタップ , スパイラル ポイントタップ,スパイラルタップดอกต๊าปเกลียวพิเศษ สั่งทำ เกลียวโอเว่อร์ไซด์ เกลียวใหญ่ เกลียวแปลกๆ ดอกต๊าปเกลียวซ้าย ที่ไม่มีในท้องตลาด เกลียวพิเศษ (เพียงแค่มี Drawing หรือตัวอย่างชิ้นงาน) Material : Carbide , HSSe, AISI M42, JIS SKH59 DIN 1.3343,SKH-9
ดอกต๊าป , ดอกต๊าปเกลียวหุน ดอกต๊าปเกลียวสว่าน ดอกต๊าปเกลียวมิล ดอกต๊าป Hand Tap ดอกต๊าปสำหรับต๊าปรูตัน ดอกต๊าปมือ แมชชีนต๊าป ดอกต๊าปไฮสปีค ดอกต๊าป 3 ตัวชุด ดอกต๊าปชุด ดอกต๊าปเครื่อง ดอกต๊าป HSS.ดอกต๊าปเกลียวซ้าย ดอกต๊าปมือ แมชชีนต๊าป Machine Tap ดอกต๊าปเกลียวข้อต่อทองเหลือง เกลียวข้อต่อทองเหลือง เกลียวในเกลียวนอก เกลียวนิ้ว เกลียวเฉียงเตเป่อร์ ดอกต๊าปเกลียวสำหรับต๊าปเกลียวข้อต่อทองเหลือง ดอกต๊าปเกลียวข้อต่อทองเหลือง (Brass Fitting Tap )
Special Tap : Metric Taps, Metric fine tap, BSW ,BSF,UNC,UNF,UNEF,UNS
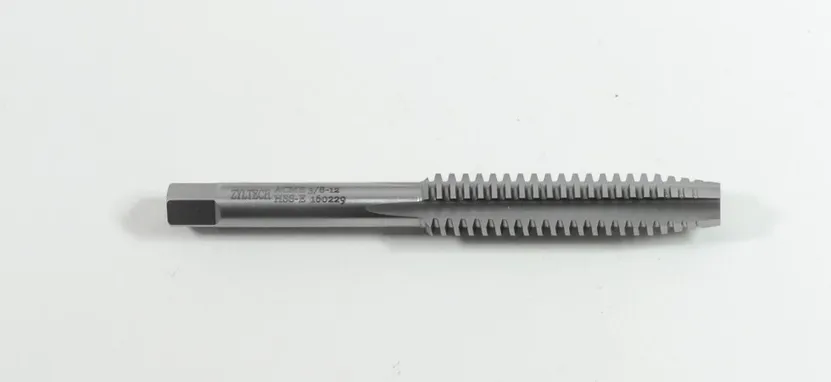
Special Left Hand Tap. Acme Taps Special Acme Taps UNC, UNF, BSW, Metric, ACME, ball screw, thread. Metric (M),BSW,UNC,UNF, TW,BS, PT,NPT,PS,NPS,Sewing Machine(SM).Bicycle (BC),NGT,NGO
Siam Master Precision Tool LTD. standards, ISO, ANSI, DIN, DIN/ANSI and JIS. DIN and ISO is common world-wide HELICOIL AMECOIL VCOIL STI REPAIR THREAD
OVERSIZE TAP customized tap
ต๊าปเกลียวโอเว่อร์ไซด์ สำหรับชิ้นงานชุบกาวาไนซ์
hot dip galvanized coating galvanized
For workpiece to Coating
Special spiral tap, made to order, overside spiral, large spiral, strange spiral, left-hand spiral tap That is not available in the market, special thread (just have a drawing or sample) Material : Carbide , HSSe, AISI M42, JIS SKH59 DIN 1.3343,SKH-9
taps, spiral taps Drill thread tap Spiral tap, hand tap, tap for solid tap, hand tap, machine tap, hi-speak tap, 3 taps, tap set, machine tap, tap HSS. left-hand thread tap, hand tap, machine tap, machine tap, threaded tap, brass joint brass threaded fitting Internal thread, external thread, inch thread, oblique tapered thread Threading tap for tapping brass joints Brass Fitting TapACME Taps - Special
Extension Taps - Special
Extension Pipe Taps - Special
Forming Taps
Long Series - Special Taps
Nut Taps - Special
Pipe Taps - Special
Popular Special Taps and Dies (Inches)
Popular Special Taps and Dies (Metric)
Short Series - Special Taps
Spiral Flute Tandems - Special
Spiral Flute Taps - Special
Straight Flute Tandems Taps - Special
Type: Straight Flute, Spiral Flute, Spiral Point, and Forming thread taps.
Material: HSS, HSS-CO, HSS-E, HSS-PM, etc.
Coating: Balzers TiN, TiALN, TiCN coating
Workpiece: Suitable for steel, stainless steel, cast iron, aluminum, and hardened steel.
Both standard and custom products are available
Dies
Cone Dies
Hexagon Pipe Dies
Popular Special Dies ( Inch)
Popular Special Taps and Dies (Metric)
Round Adjustable Split Dies
Special Round Adjustable Dies
ดอกต๊าปเกลียวประเทศไทย SMPT OSG YAMAWA Thailand Taps Thread Spiral Taps
ดอกต๊าปเกลียว คืออุปกรณ์ที่ใช้ในการสร้างเกลียวให้กับชิ้นงาน ไม่ว่าจะเป็นเกลียว(M)metric ,เกลียว G ,เกลียว R และเกลียวชนิดอื่นๆ อีกมากมาย ซึ่งเกลียวที่เกิดจากการต๊าปนั้นล้วนมีทั้งเกลียวใน และเกลียวนอก ในบทความนี้เราจะมาดูในส่วนของวิธีการต๊าปเกลียวด้านในกันครับ
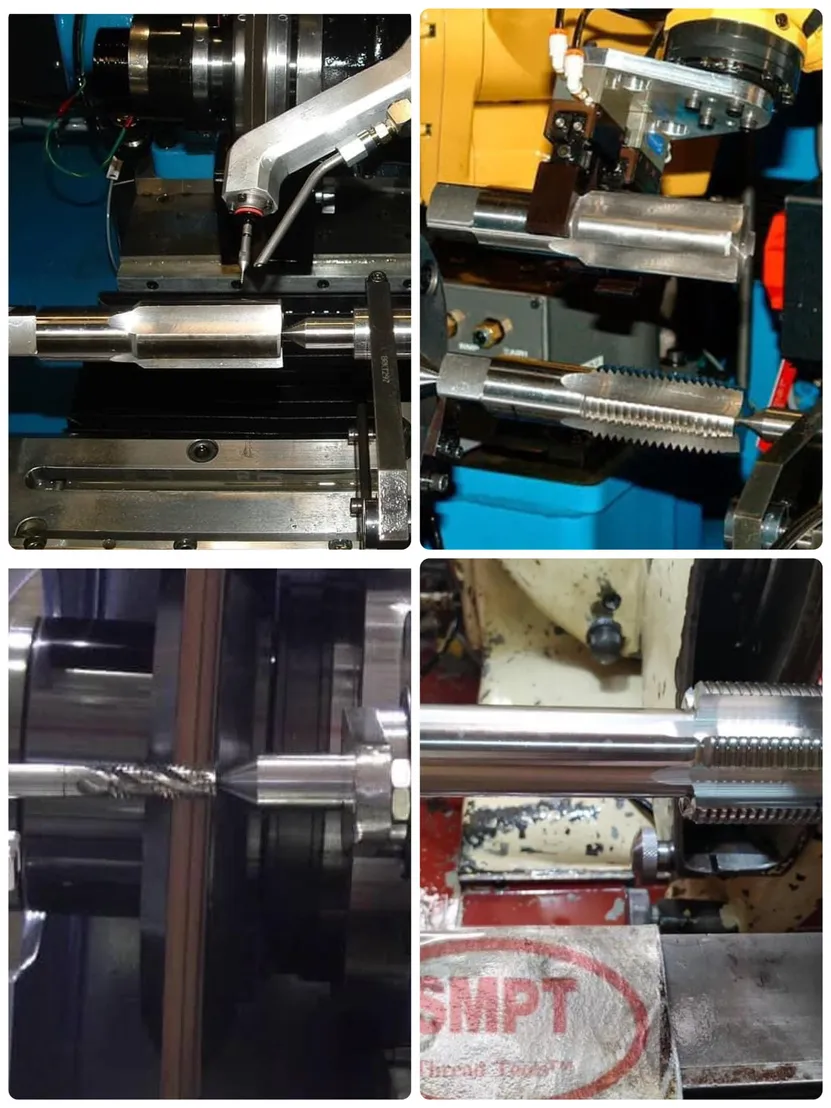
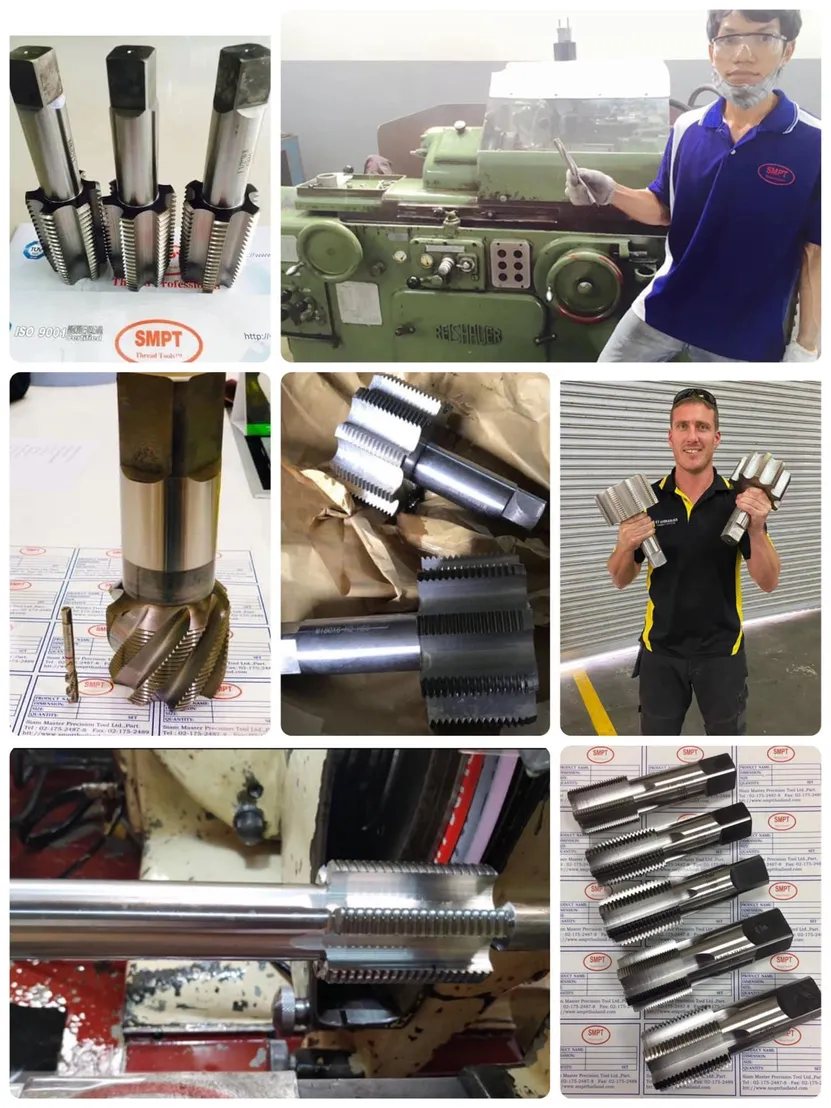
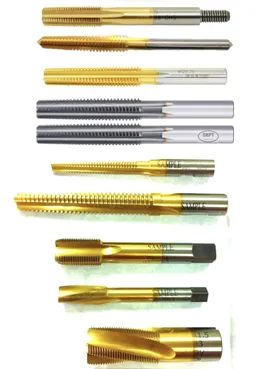
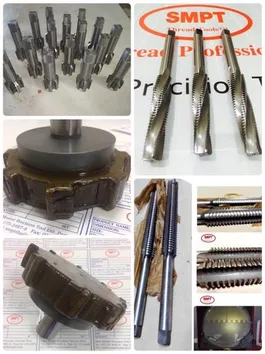
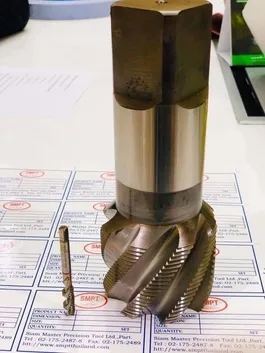
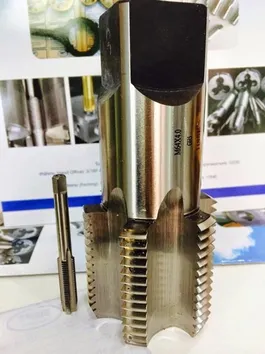

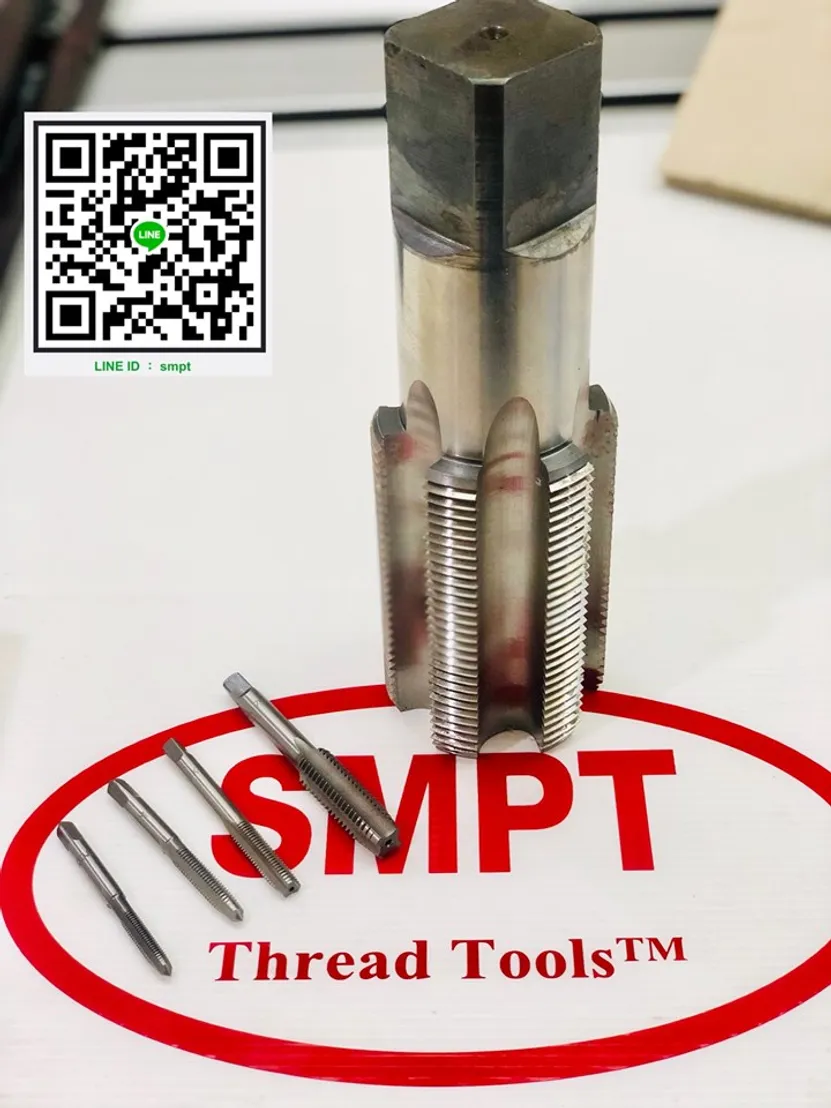
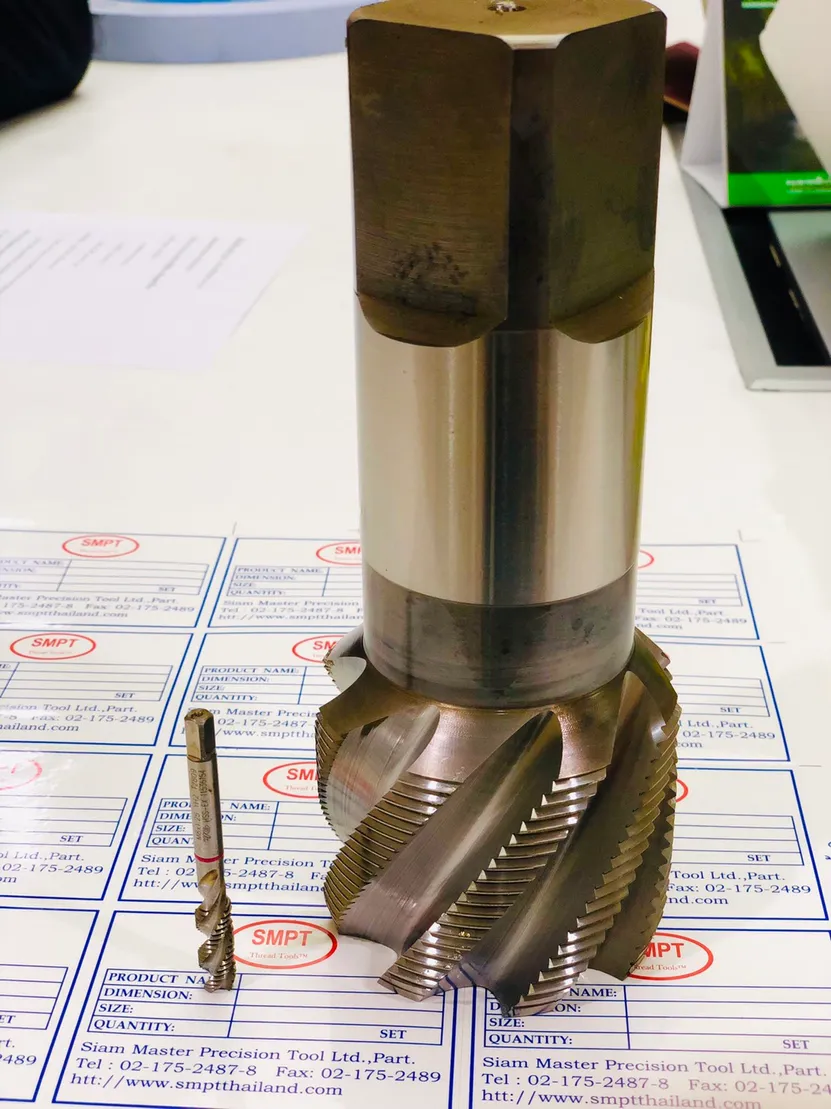
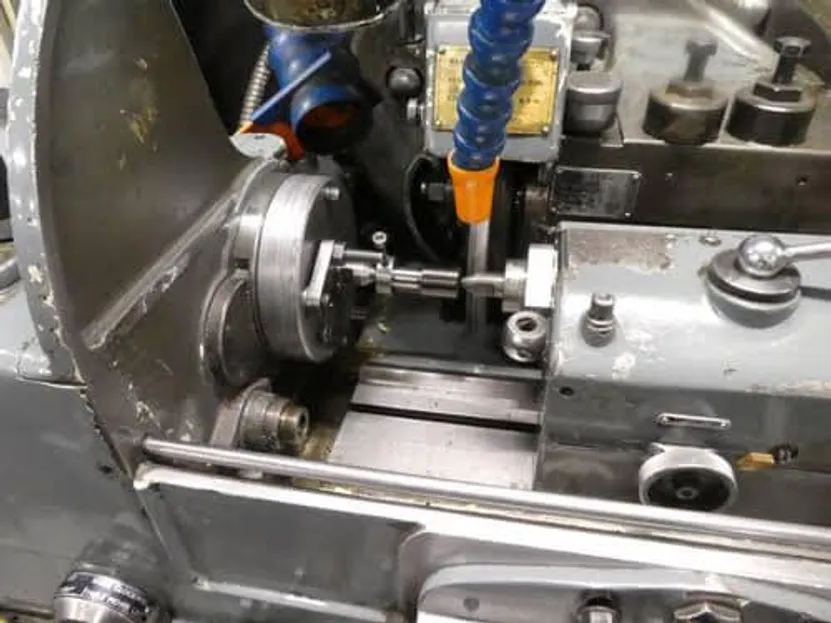
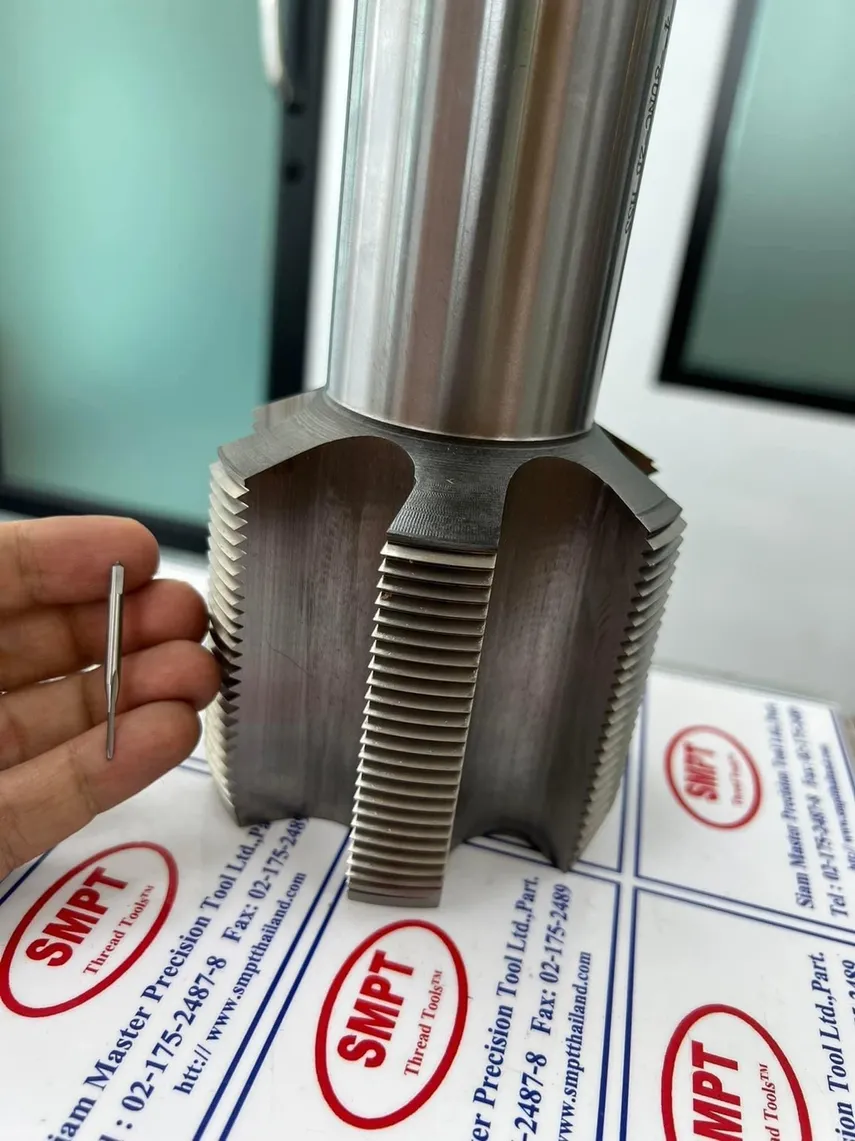
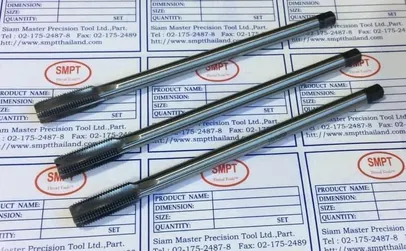
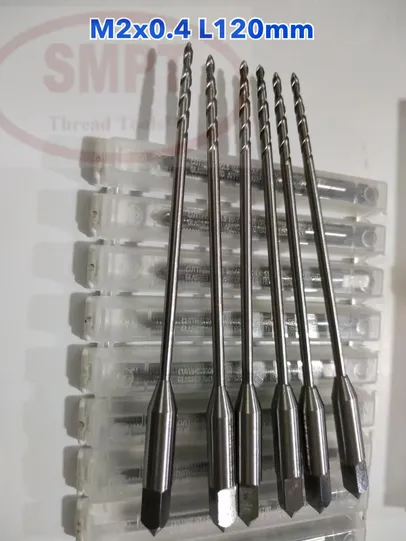
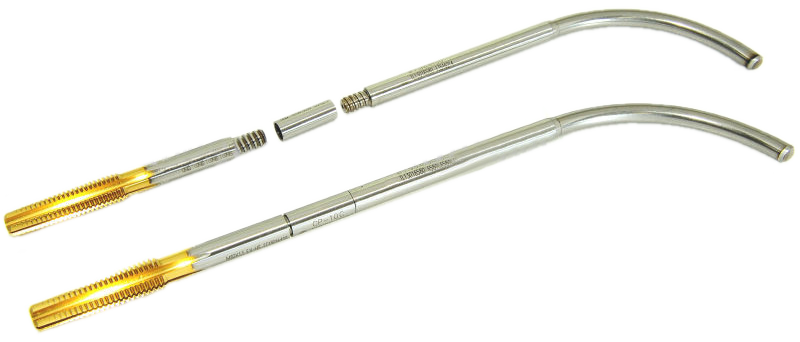
#Longshanktap #ต๊าปด้ามยาว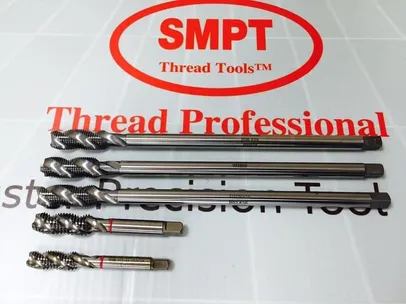
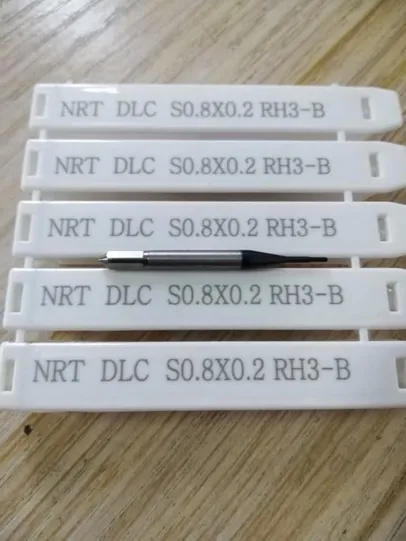
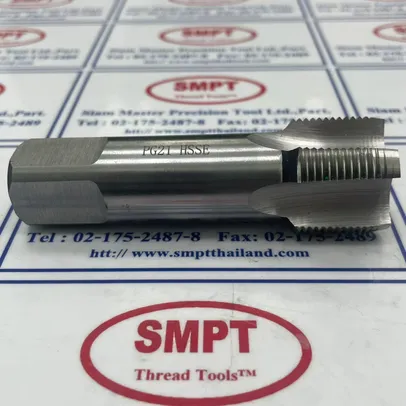
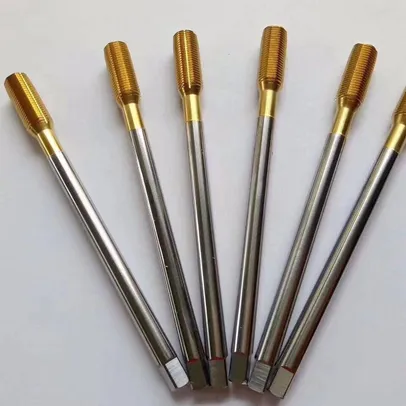
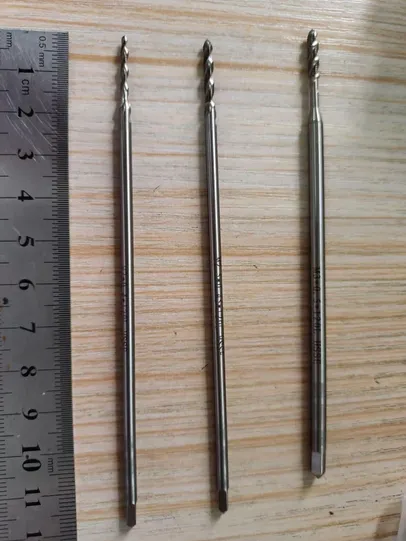
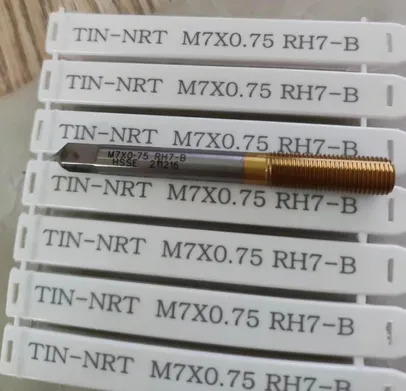
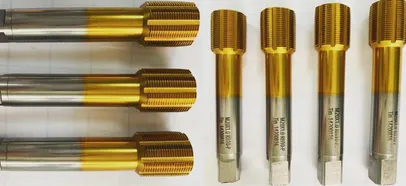
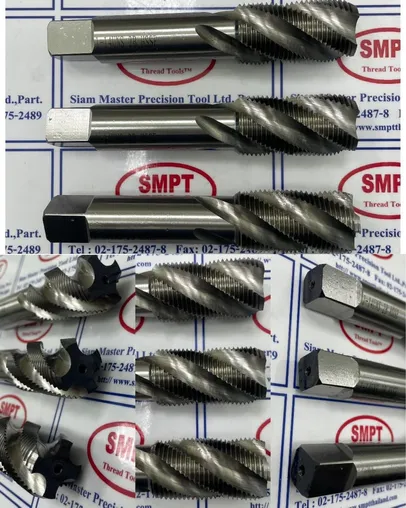

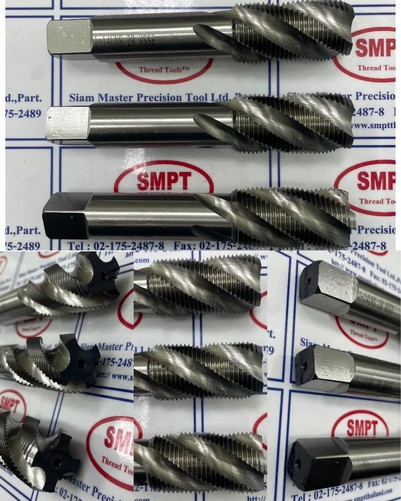
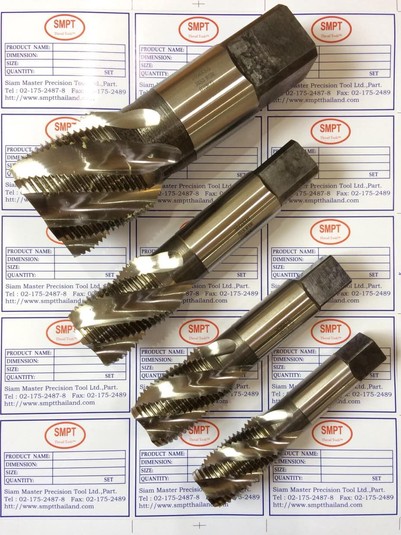
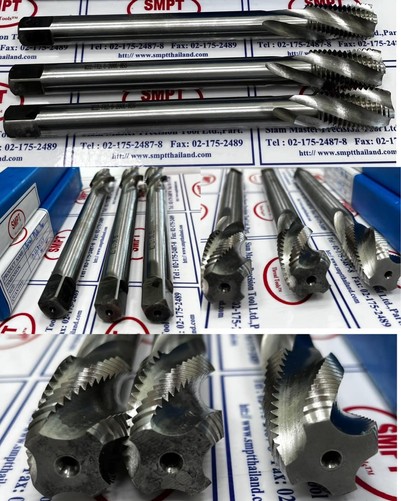
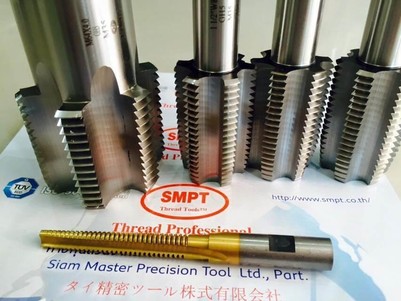
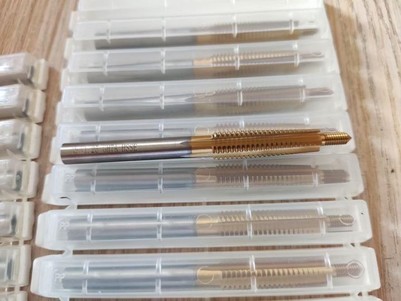
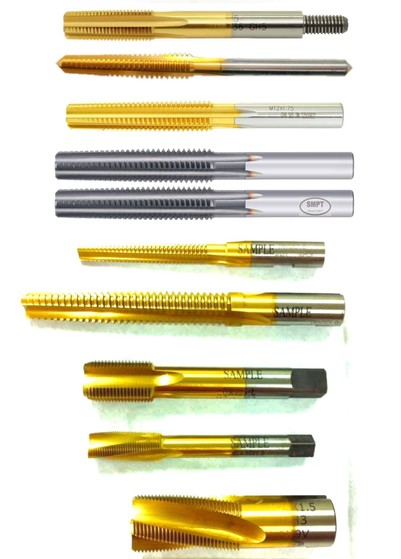

ดอกต๊าปพิเศษ เกลียวพิเศษ สั่งทำ
รับทำดอกต๊าปพิเศษ ตามแบบ Drawing
BSW, BSF, BSP, BSCON, BS, CY, BSB, BA, ME, BSPT, UNF, UNC, UNEF, UNS, NPT
Thread cutting Tap, Special Screw tap,
Special Custom-Made Tap Special Custom-Made Tap
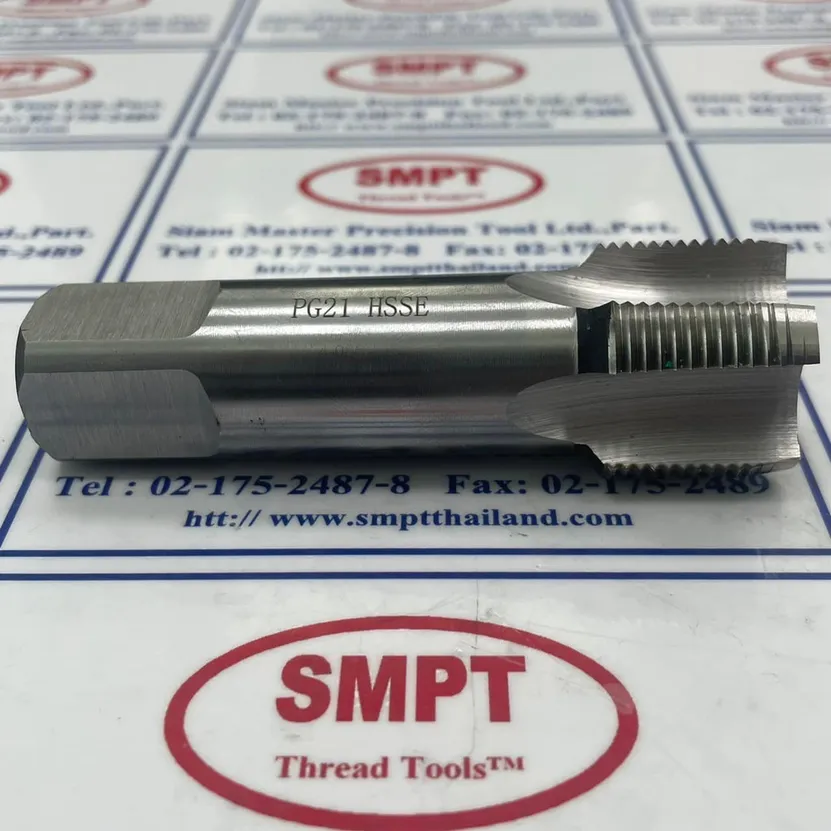
Through hole/ Blind hole. PG gland thread sizes
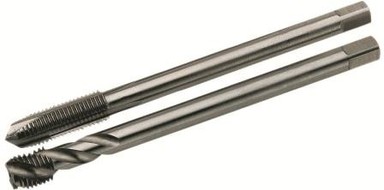
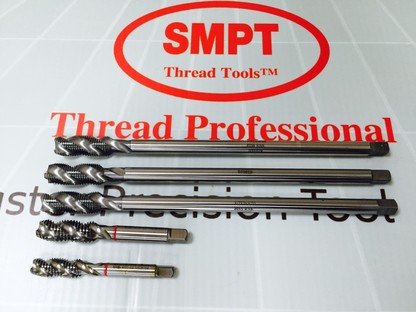
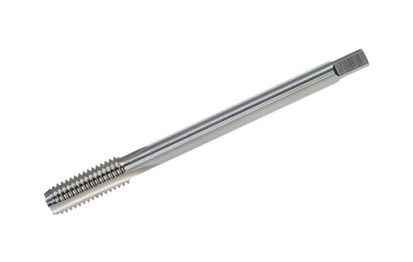
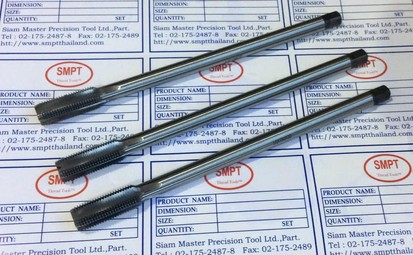
Special Taps HSS, HSSE, and Carbide
Special Tap designed to your unique specification….
Our Special taps can be used to cut a wide range of materials and are available in various Thread forms, the following is a list of those well know: -
ACME,ANPT,BA,G,ISO,METRIC,KNUCKLE,MJ,NPS,NPSF,NPSI,NPSM,NPT,NPTF,PG,RADIUS,RC,RP,STUB,TRAPEZOIDAL,,UNIFIED,UNJ,WHITWORTH.
切削タップは、めねじを加工する工具で、ハンドタップをはじめスパイラルタップ、スパイラルポイントタップ、管用タップ、ナットタップなどあります。PG gland thread sizes
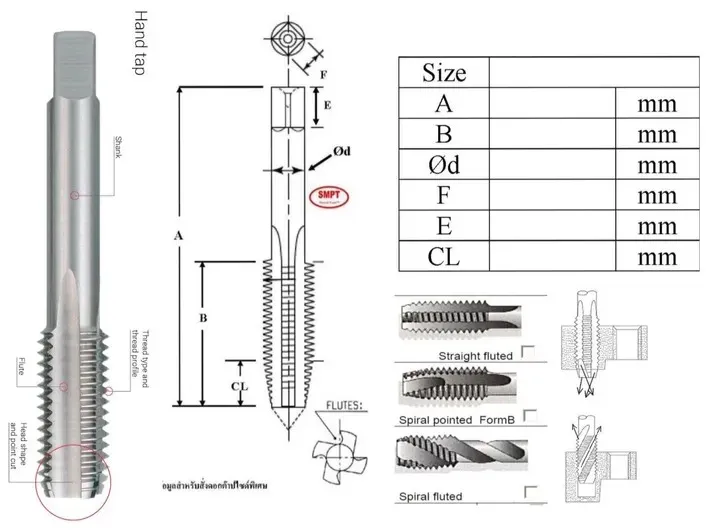
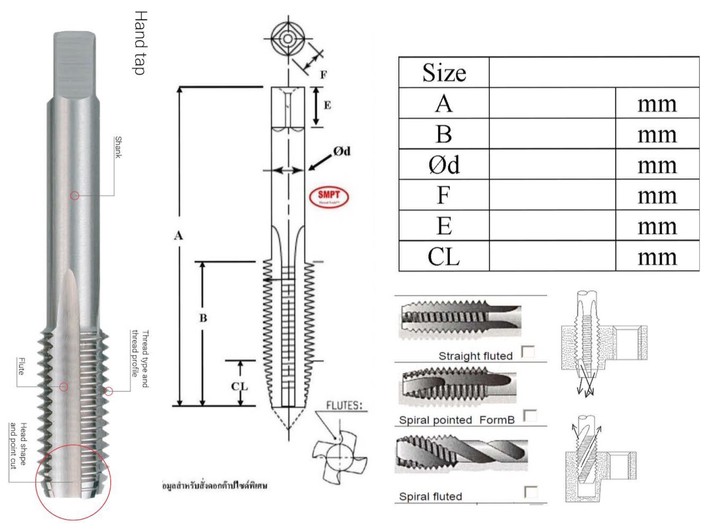
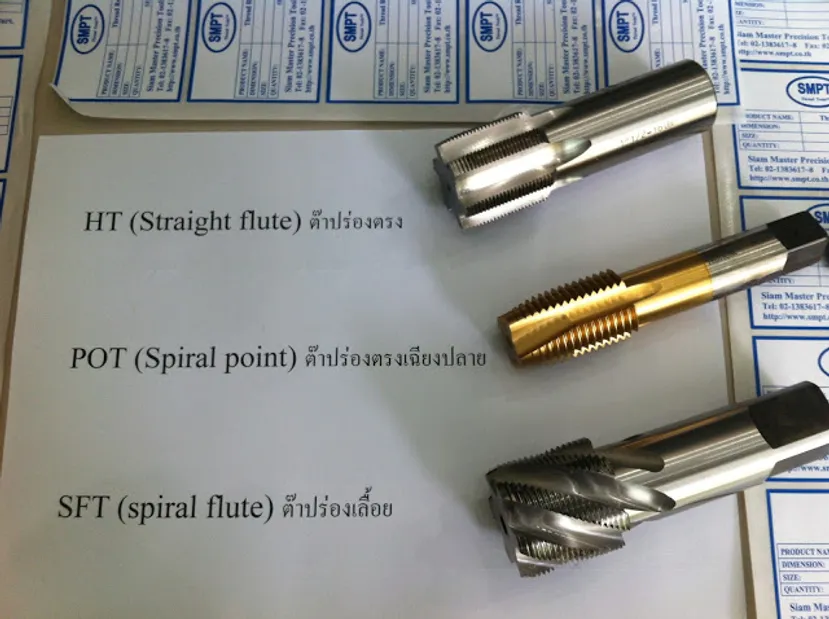
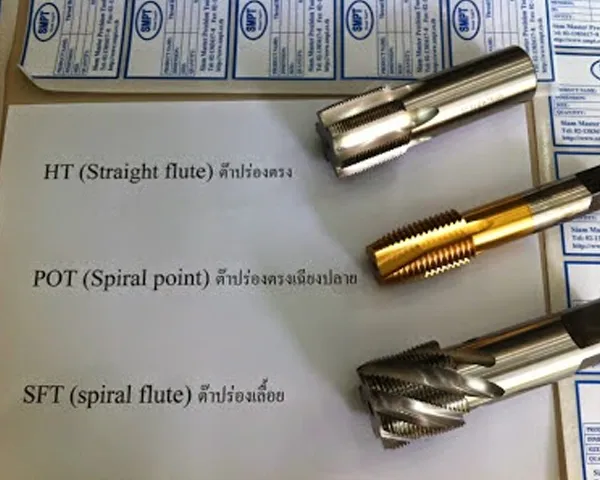
Hand Tap & Machine Tap ดอกต๊าปจะแบ่งหลักๆ ได้3 ชนิด คือ HT(straight flute) , POT(spiral point) SFT(spiral flute)
ดอกต๊าปเกลียว (Taps) คืออะไร มีการใช้งานอย่างไร
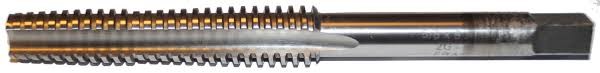
1.- M/C & HT (Straight flute) HT(ハンドタップ) = 1SET = 3 Pcs (No.1,No.2,No.3) ต๊าปร่องตรง สามารถประยุกต์ใช้งานได้ทั้งรูทะลุและรูตันโดยทั่วไปมักใช้กับวัสดุที่แข็ง
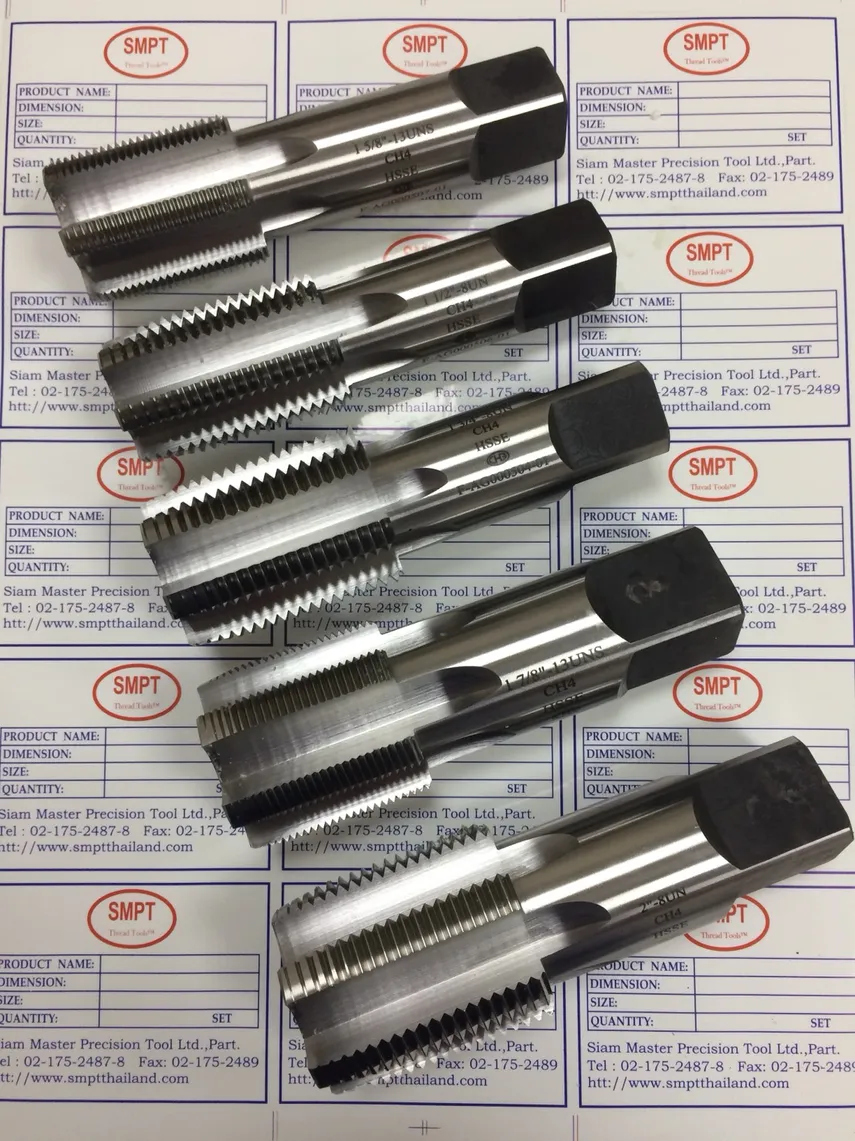
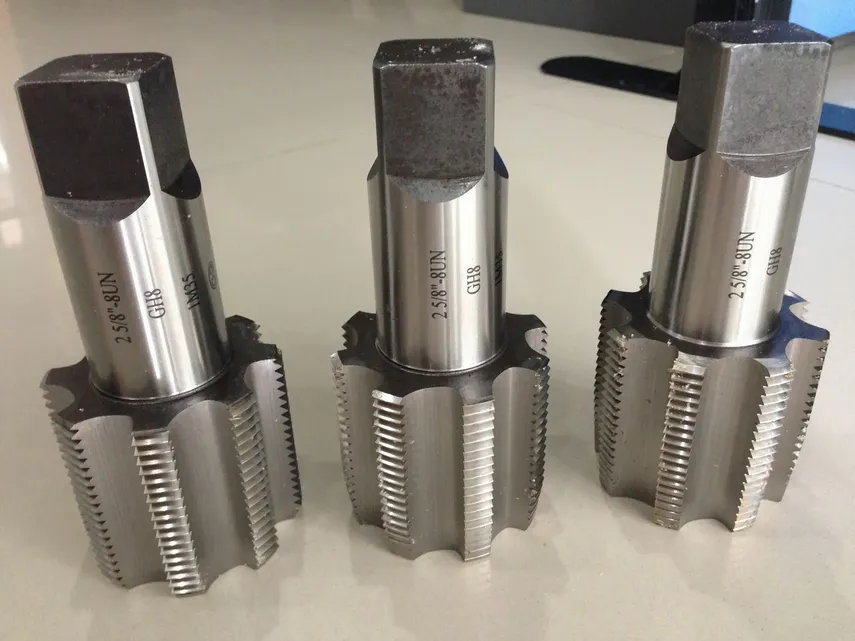
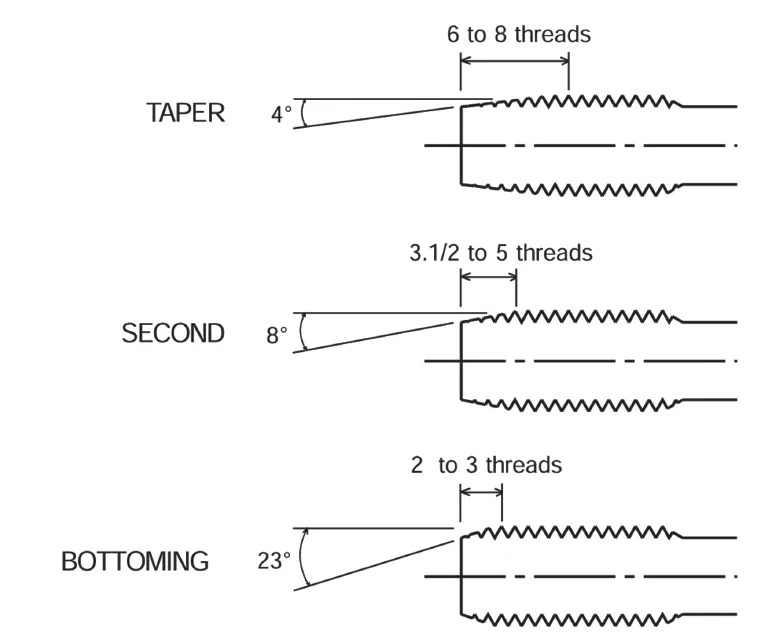
Tap No.1 = TAPER TAPS have a lead of 7-10 threads at 5 degrees per side. The taper lead distributes the cutting force over a large area, and the taper shape helps the thread to start. They can therefore be used to start a thread prior to use of second or
bottom leads, or for through holes.
Tap No.2 =SECOND TAPS have a lead of 3-5 threads at 8 degrees per side. They are the most popular and can be used for through holes, or blind holes where the thread does not need to go right to the bottom.
Tap No.3 =BOTTOM TAPS have a chamfer (lead) of 1–2 threads, the angle of the lead being around 18 degrees per side. They areused to produce threads close to the bottom of blind holes.
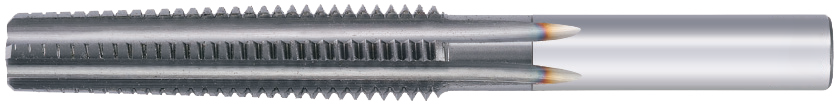
2.POT (Spiral point) POT(ポイントタップ)の特徴 ใช้งานได้เฉพาะรูทะลุ ต๊าปชนิดนี้ร่องเลื้อยที่แคบและเป็นแบบพิเศษ ทำให้โครงสร้างที่ค่อนข้างแข็งแรง
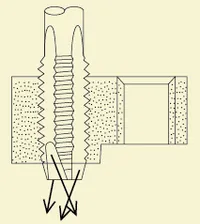
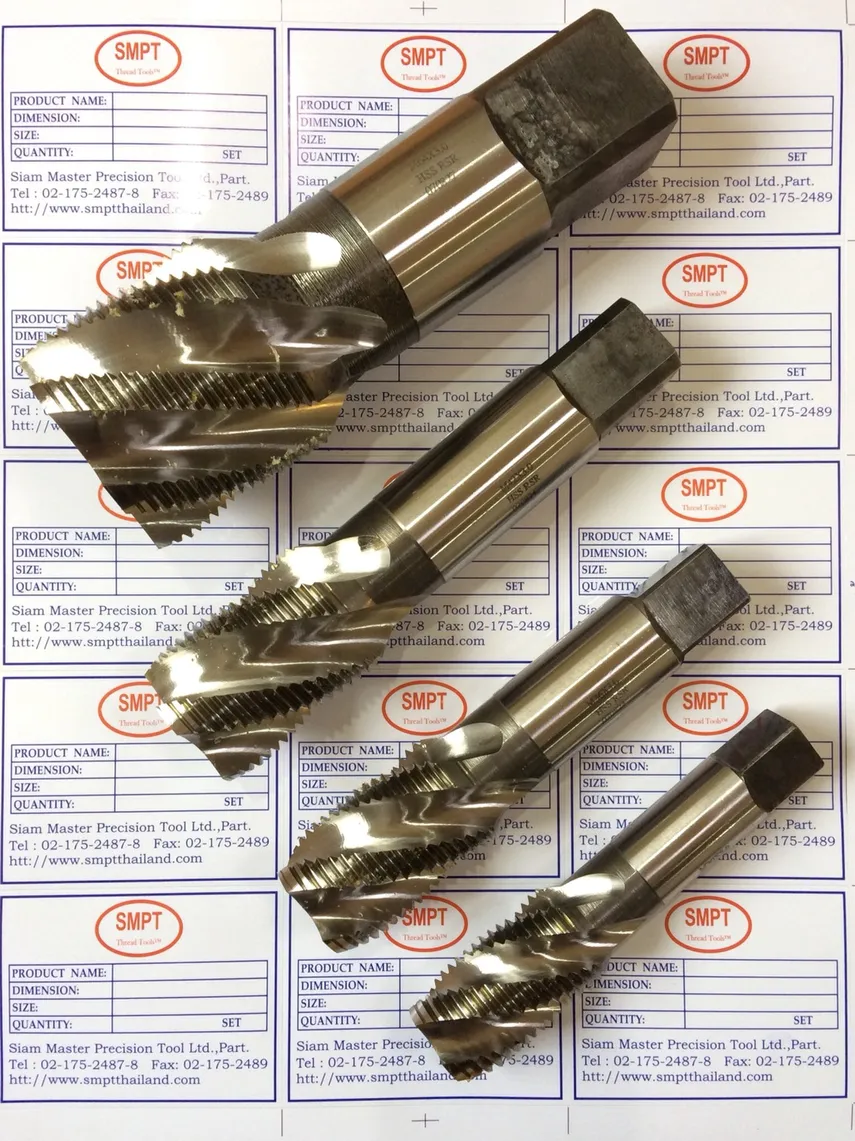
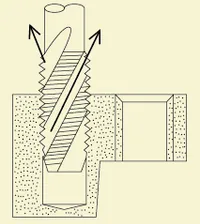
3.SFT (spiral flute)SFT(スパイラルタップ)の特徴ต๊าปร่องเลื้อยใช้งานได้กับรูตัน ต๊าปชนิดนี้ทำให้เกิดแรงบิดน้อยกว่าเศษที่คายออกมาไหลออกมาในทิศทางตรงข้าม Spiral Fluted Tap For Blind Hole,Spiral Flute Tap for Through hole (With LH Spiral Fluted)
กับทิศทางของการต๊าป
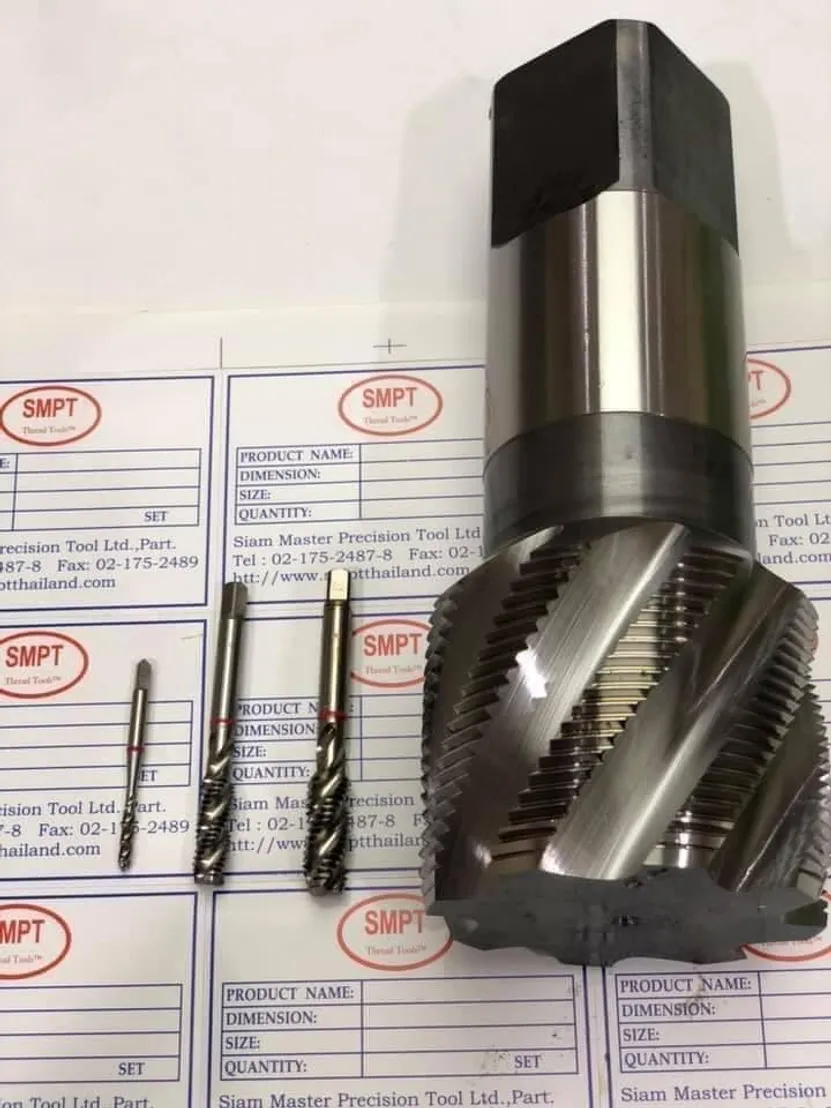
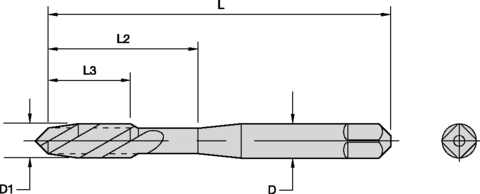
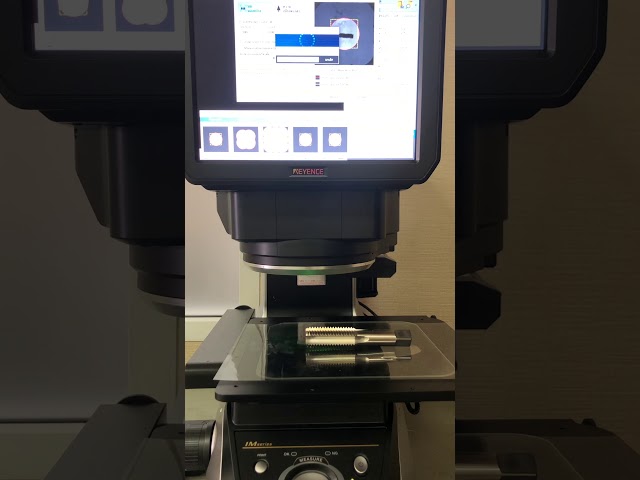
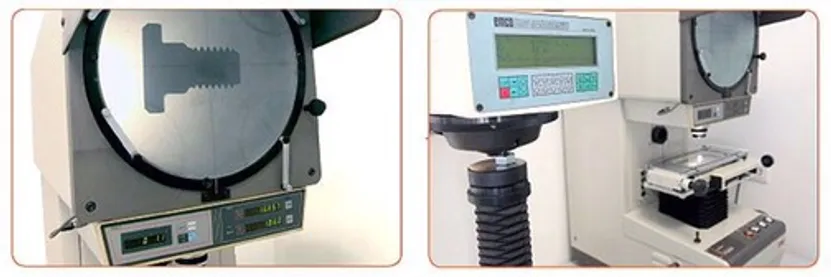
ดอกต๊าปเกลียวพิเศษ สั่งทำ เกลียวโอเว่อร์ไซด์ เกลียวใหญ่ เกลียวแปลกๆ ดอกต๊าปเกลียวซ้าย ที่ไม่มีในท้องตลาด เกลียวพิเศษ (เพียงแค่มี Drawing หรือตัวอย่างชิ้นงาน) ทางเราจะวัดค่าจะชิ้นงาน เพื่อผลิตดอกต๊าปเกลียวพิเศษ
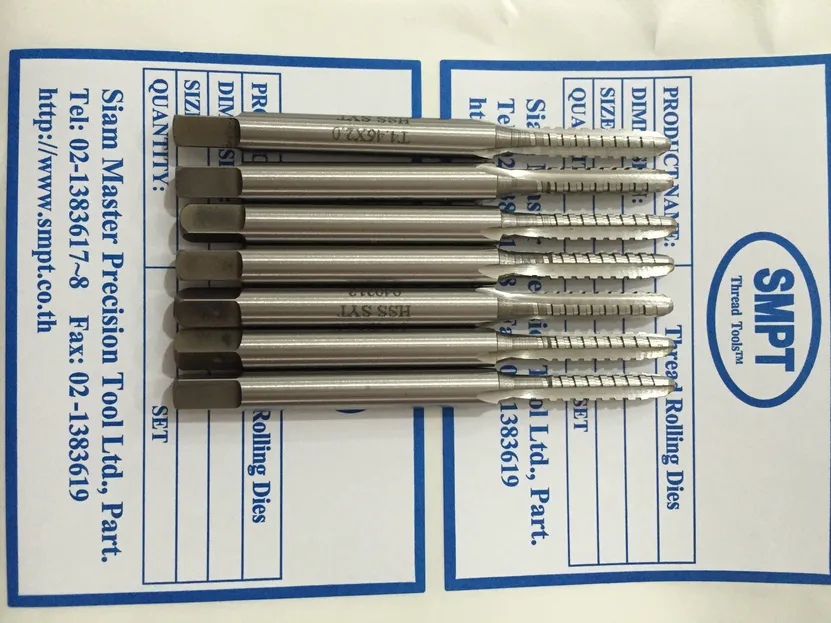
4.ต๊าปไร้เศษ ต๊าปรีดเกลียว Roll Taps Forming Tap Fluteless Taps เกลียวไส้กรองน้ำมัน #Forming Tap
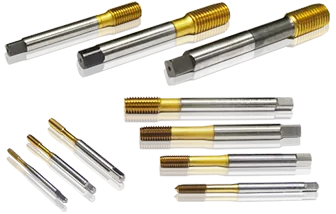
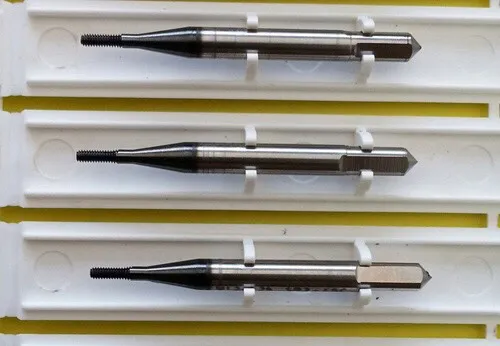
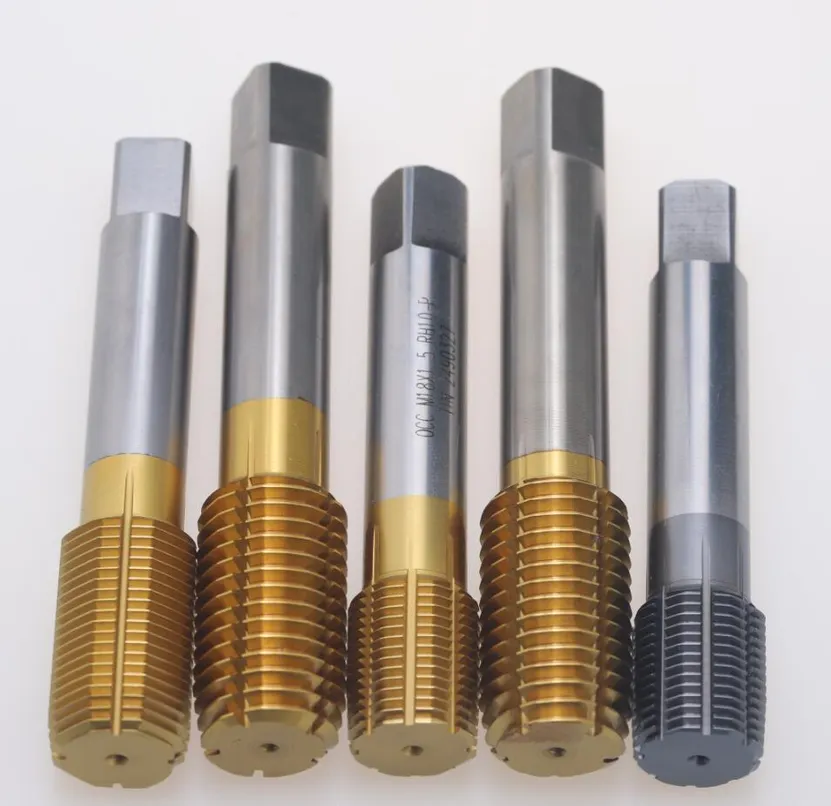
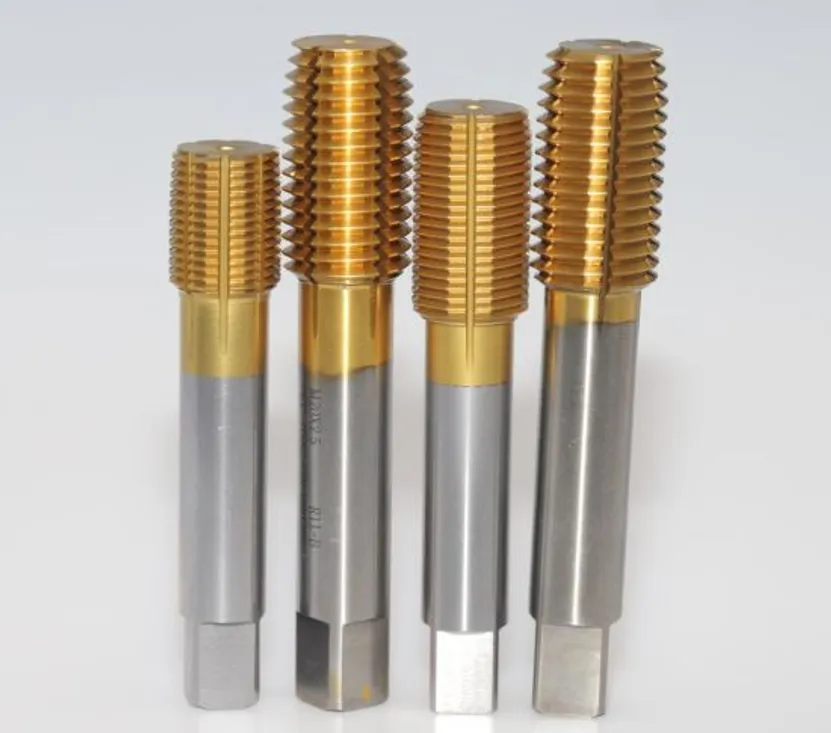
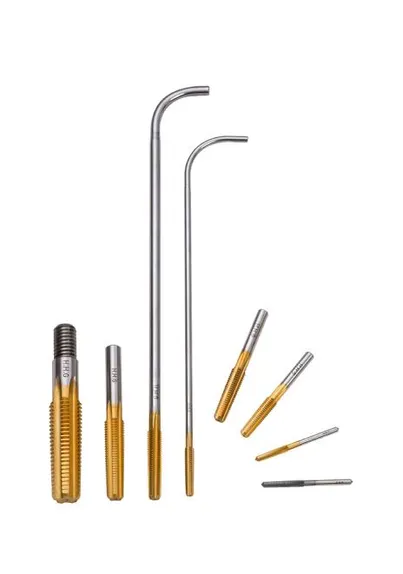
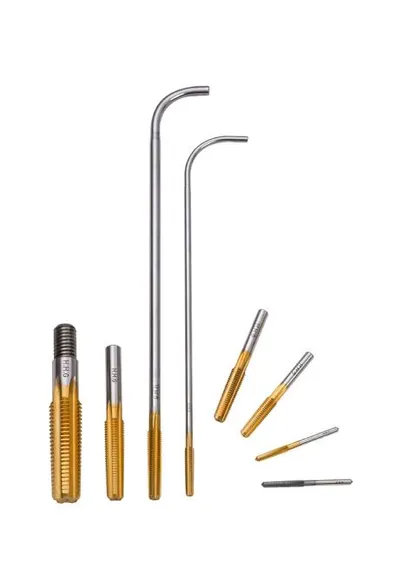
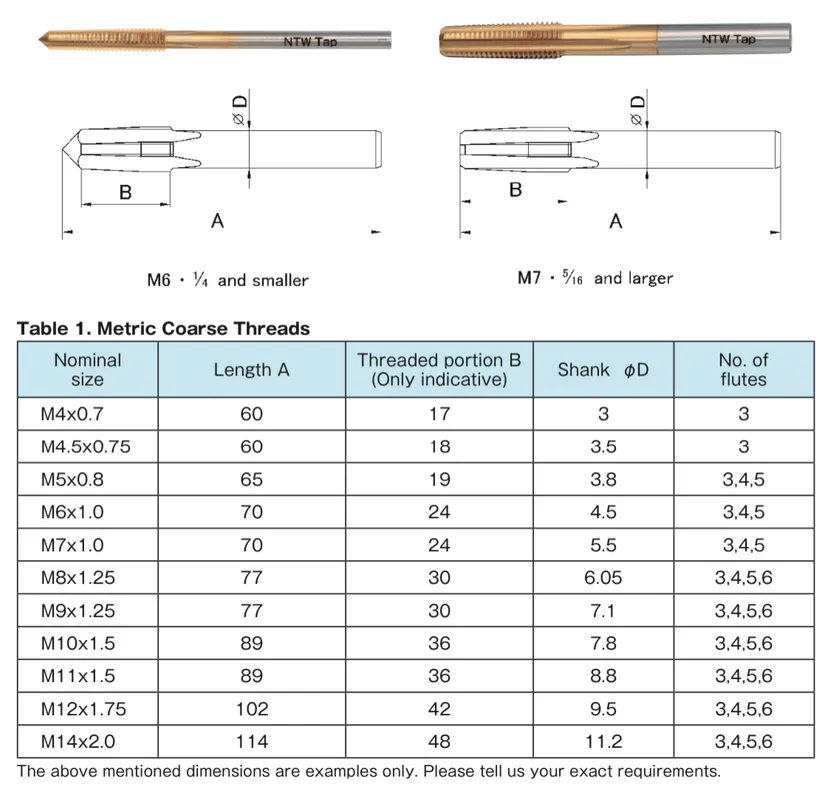
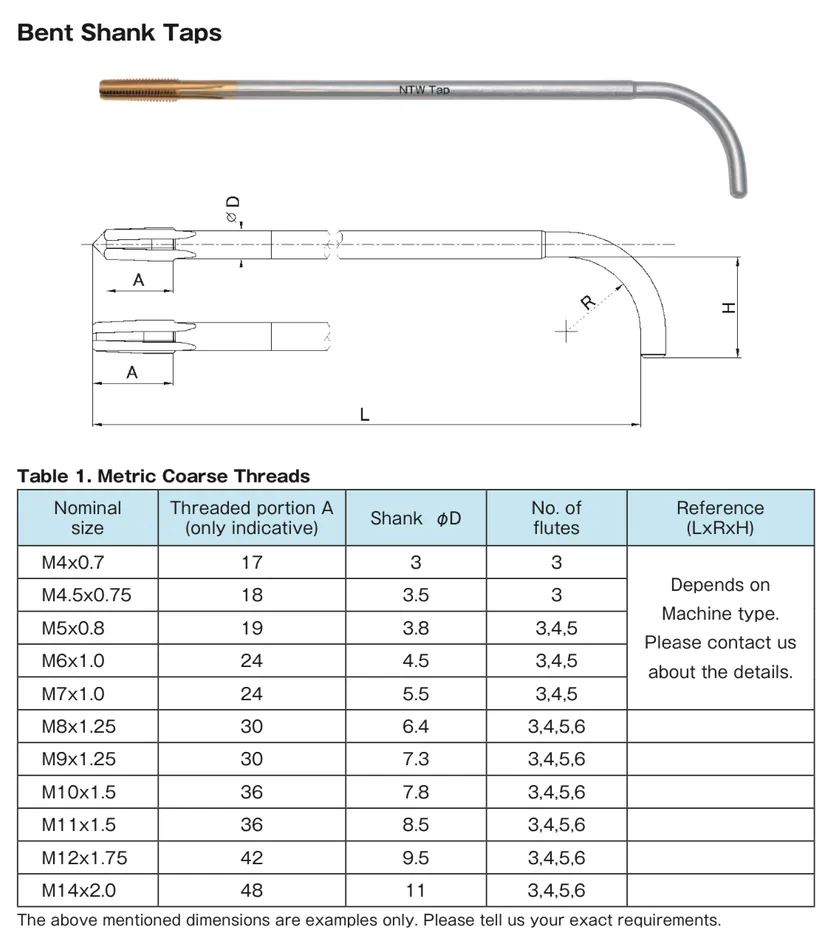
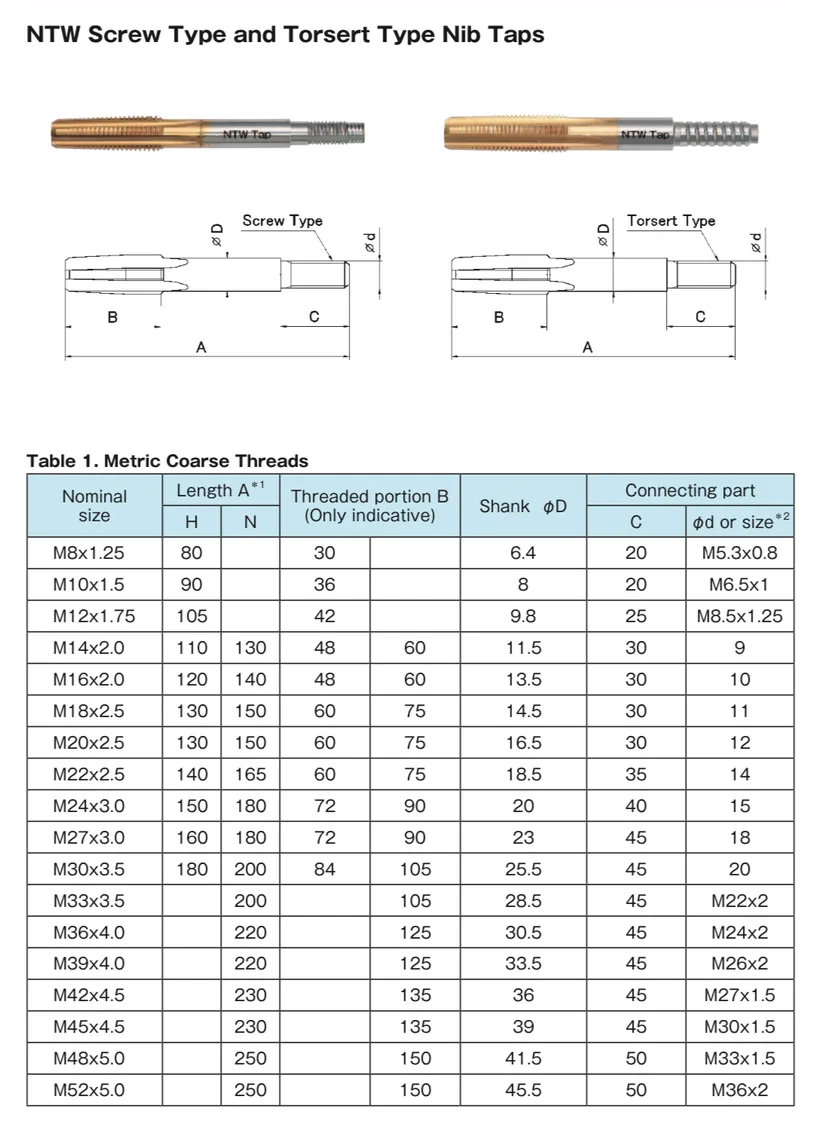
5. Nut Tap Tapped nuts automatically pass through bent shank portion and nuts can be tapped continuously without reverse and machine stop. Automatic nut tapping Machine Tap
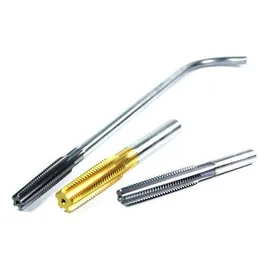
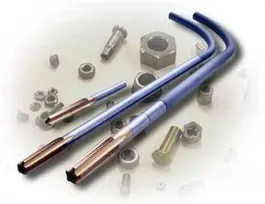
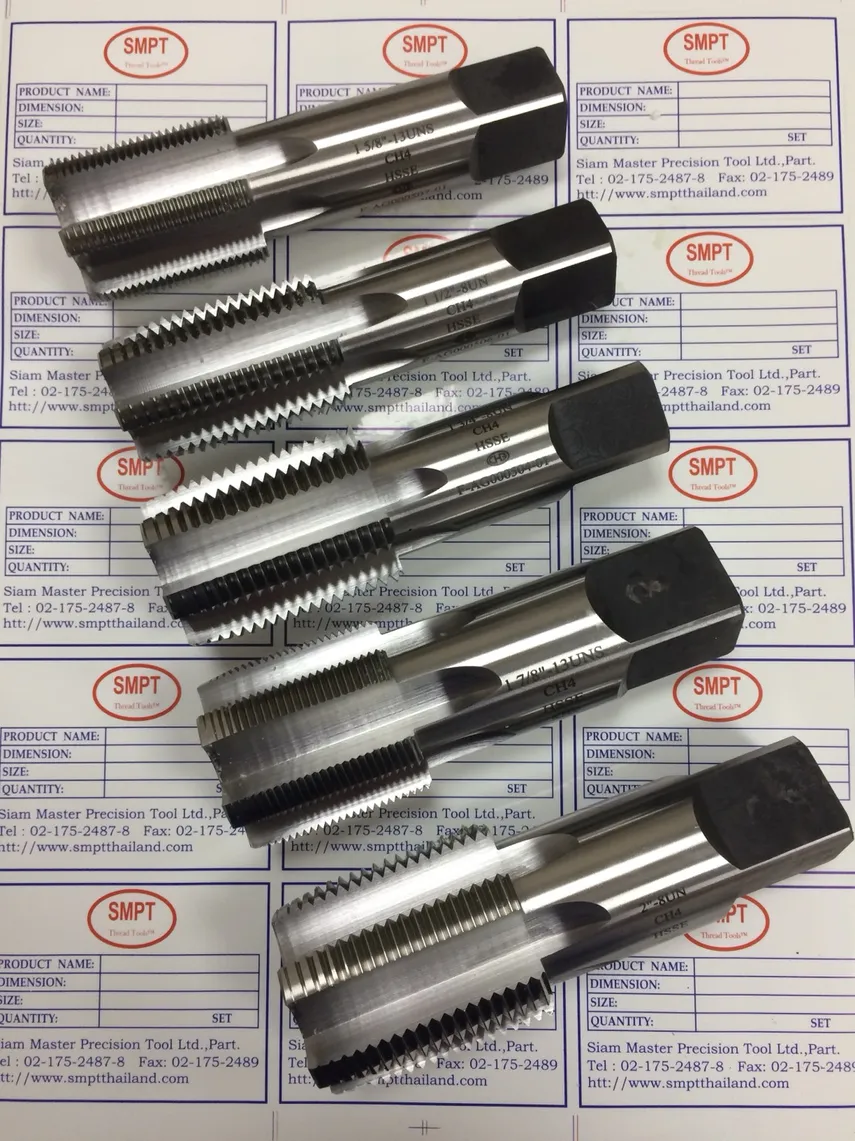
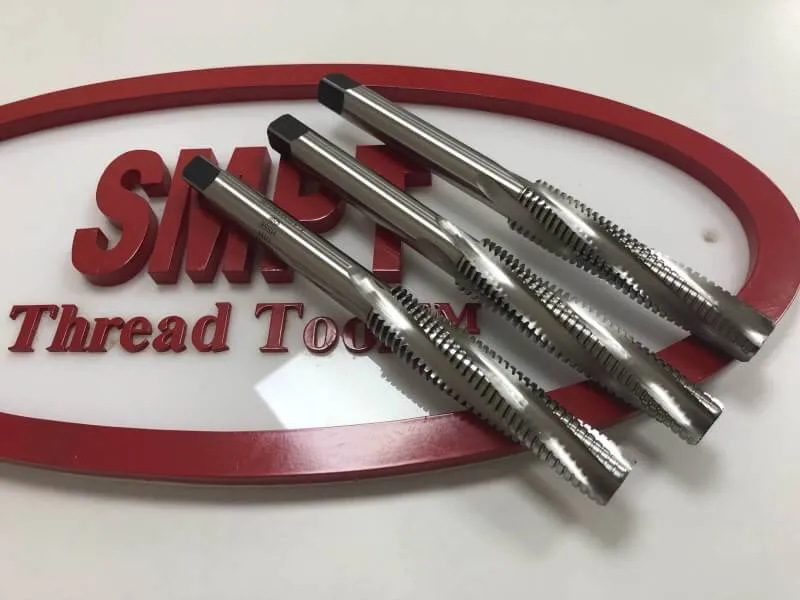
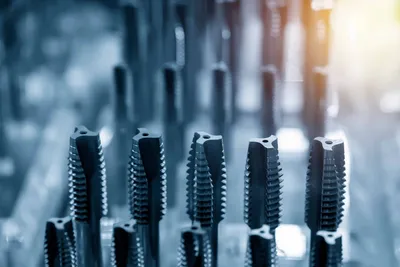

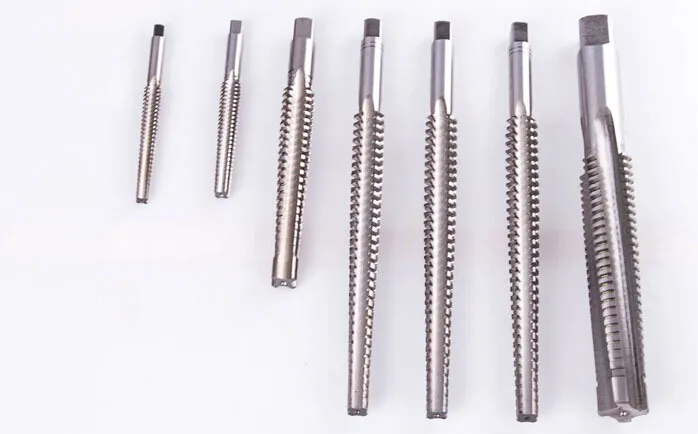
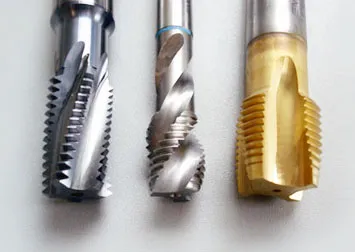


標準タップシリーズは<HT(ハンドタップ)>、<SP(スパイラルタップ)>、<PO(ポイントタップ)>の3種類の形状をラインアップしております。幅広いご要求におこたえできるよう、メートルねじはもちろんのことユニファイねじ、ウイットねじまで充実した寸法範囲となっております
HT(ハンドタップ)の特徴
切りくず収納を考慮したストレート溝を有した切削タップです。
食付き部の長さ(山数)により(先)タップ、(中)タップ、(上)タップの種類があります。
切りくずをタップ進行方向に排出するようにポイント溝が施してある切削タップで、通り穴ねじの加工に最適です。
切りくずの障害が少ないため切削トルクが低いのが特徴です。
SFT(スパイラルタップ)の特徴
切りくずをタップ進行方向とは逆(手前)に排出するように溝がねじれた切削タップで、止り穴ねじの加工に最適です。
切削性が良好なため、粘い材料にも適しております。
ดอกต๊าปเกลียว คืออะไร
ดอกต๊าปเกลียว (Tapping) หรือที่เรียกกันสั้นๆ ว่า “ดอกต๊าป” คืออุปกรณ์สำหรับสร้างรูเกลียวในวัสดุต่างๆ เพื่อเชื่อมต่อวัสดุที่ต้องการด้วยการหมุนเกลียวให้เข้ากันได้อย่างพอดี ดอกต๊าปมีการใช้งานในอุตสาหกรรมการผลิตอยู่มาก ไม่ว่าจะเป็นผู้ผลิตขนาดเล็กหรือขนาดใหญ่ ขึ้นอยู่กับว่าผู้ใช้งานนั้นต้องการสร้างชิ้นงานแบบไหน
การใช้งานดอกต๊าปได้ถูกชนิดและถูกวิธี จะช่วยขนาดของรูเกลียวที่ได้เป็นขนาดมาตรฐาน สามารถใช้งานได้ง่าย ทั้งนี้ผู้ใช้งานควรสังเกตวัสดุที่เหมาะสมกับดอกต๊าปนั้นๆ เพื่อยืดอายุการใช้งานอุปกรณ์และทำให้ดำเนินงานได้อย่างมีประสิทธิภาพ
มุมพิตช์ (PITCH) สิ่งที่ควรรู้จักก่อนใช้ดอกต๊าป
รูปมุมพิตซ์ ภายในบทความ ดอกต๊าปเกลียว
มุมพิตช์เป็นระยะจากสันเกลียวหนึ่งไปยังอีกสันเกลียวหนึ่งบนดอกต๊าป และวัสดุอื่นๆ ที่เป็นเกลียว ซึ่งจะมีขนาดมาตรฐาน เมื่อทำเกลียวในที่ได้มุมพิตช์ที่ถูกต้องก็จะสามารถสวมน๊อตหรือนำอุปกรณ์ที่ได้รับการดายส์ (ทำเกลียวนอก) ได้อย่างพอดีตามขนาดมาตรฐาน
การทำงานของดอกต๊าปเกลียว
ดอกต๊าปมีหลักการทำงานเพื่อกัดขึ้นรูปเกลียวในวัสดุที่ต้องการให้เกิดเกลียวขึ้นมาไม่ว่าจะเป็นเกลียวแบบทะลุหรือเกลียวแบบรูตัน โดยเริ่มจากการใช้สว่านเจาะรูบนวัสดุที่ต้องการต๊าปเกลียว เพื่อทำให้ดอกต๊าปสามารถทำงานได้ง่ายขึ้น
รูปที่2 ภายในบทความ ดอกต๊าปเกลียว
การควบคุมการหมุนของการทำเกลียวไม่ว่าจะเป็นการทำด้วยมือ (hand tap) หรือการทำด้วยเครื่อง ต้องสามารถหมุนไปและหมุนกลับได้ด้วยความเร็วที่ถูกควบคุมอย่างดี เพื่อป้องกันแรงกดที่มากเกินไปจนทำให้ดอกต๊าปแตกเสียหาย
ขณะที่ดอกต๊าปกำลังกัดเกลียวภายใน เศษของวัสดุจะหลุดออกมา โดยเศษของวัสดุจะมีความแตกต่างกันตามเนื้อของวัสดุ ทำให้ดอกต๊าปถูกผลิตขึ้นมาให้มีปลายคมตัดหลายลักษณะ เพื่อให้สามารถกัดเกลียวกับวัสดุที่เหมาะสมและมีการระบายเศษที่ดีขึ้น
5 รูปแบบของดอกต๊าปเกลียว
สำหรับดอกต๊าปเกลียวที่ยกมาในบทความนี้จะนำเอา 5 รูปแบบของดอกต๊าปเกลียวที่นิยมใช้ในตลาดการผลิต
1. ดอกต๊าปร่องตรง (Straight Flute Tap)
ดอกต๊าปร่องตรง (Straight Flute Tap)
ดอกต๊าปร่องตรงเป็นดอกต๊าปแบบมาตรฐานที่ถูกผลิตมาเพื่อการทำเกลียวได้ทั้งเกลียวแบบทะลุและแบบรูตัน โดยสามารถทำเกลียวได้ดีบนวัสดุที่ทำมาจากเหล็กหล่อ ทำให้ดอกต๊าปชนิดนี้ถูกใช้ในการผลิตขนาดเล็กได้อย่างเหมาะสม
แต่มีข้อจำกัดคือระบายเศษได้ไม่ดี ทำให้มีเศษติดอยู่ในร่องที่ทำเกลียวสำหรับรูตัน จึงต้องทำการเป่าเอาเศษวัสดุออกจากรูหลังจากการต๊าป ถ้าเป็นวัสดุที่ไม่สามารถเป่าเอาเศษออกมาได้ เศษจะติดขัดอยู่ภายในทำให้เมื่อขันเกลียวน๊อตหรือวัสดุที่ต้องการประกอบเข้าไปจะไม่ได้ขนาดที่พอดี
2. ดอกต๊าปร่องเกลียว (Spiral Flute Tap)
ดอกต๊าปร่องเกลียว (Spiral Flute Tap)
ดอกต๊าปร่องเกลียวถูกออกแบบให้ระหว่างแต่ละเกลียวตัดมีร่องระบายเศษอยู่ โดยในขณะที่ทำการต๊าปเศษของวัสดุจะถูกดันกลับออกมาตามร่อง ซึ่งเกลียวจะมีองศาที่แตกต่างกันเพื่อให้เหมาะสมกับความเร็วรอบในการใช้งาน โดยแบ่งเป็นความเร็วต่ำมุมเกลียวจะอยู่ที่ 18-30 องศา และความเร็วสูงมุมเกลียวจะอยู่ที่ 45-52 องศา
สำหรับความเร็วสูง มุมเกลียวจะอยู่ที่ 45 องศาหรือมากกว่า เหมาะสำหรับวัสดุที่มีความอ่อนตัว เช่น อลูมิเนียม หรือทองแดง ถ้านำไปใช้กับวัสดุประเภทอื่นจะมีผลต่อร่องเกลียวที่ได้ไม่สมบูรณ์แบบ
มุมเกลียวที่ 38-42 องศา เหมาะสำหรับวัสดุที่มีความแข็งระดับกลาง เช่น เหล็กคาร์บอน หรือสแตนเลส
มุมเกลียวที่ 25-35 องศา เหมาะสำหรับโลหะผสม (Free Machining Steel) ที่มีความเปราะแตกง่าย
มุมเกลียวที่ 05-20 องศา เหมาะสำหรับวัสดุที่แข็งมากหรือเหนียวมาก เช่น สแตนเลสบางชนิด ไทเทเนียม หรือ โลหะผสมนิกเกิล
3. ดอกต๊าปปลายร่องเฉียง (Spiral Point Tap)
ดอกต๊าปปลายร่องเฉียง (Spiral Point Tap)
ดอกต๊าปปลายร่องเฉียงจะมีลักษณะคล้ายกับดอกต๊าปแบบร่องตรง แต่มีความพิเศษตรงที่บริเวณปลายของดอกจะมีร่องที่ช่วยในการดันเศษวัสดุไปด้านหน้าทำให้เศษไม่ติดอยู่ในรูที่ทำการต๊าป เหมาะกับการใช้งานที่ต้องใช้ความเร็วในการต๊าปสูงแต่ใช้พลังในการกดน้อย
4. ดอกต๊าปมือ (Hand Tap)
ดอกต๊าปมือ (Hand Tap)
ดอกต๊าปมือทำมาจากเหล็กกล้าผสมคาร์บอน หรือเหล็กกล้าความเร็วรอบสูง เมื่อถูกนำไปขึ้นรูปให้กลายเป็นดอกต๊าปที่พร้อมสำหรับการใช้งานแล้วจะมีความแข็งมาก จึงเหมาะกับการใช้ทำเกลียวกับวัสดุที่มีความแข็ง แต่ในระหว่างการต๊าปต้องมีการควบคุมการหมุนของดอกต๊าปให้ดี เพราะดอกต๊าปแม้ว่าจะมีความแข็งสูงแต่ก็หักง่ายเช่นกัน
ดอกต๊าปมือมีหัวเกลียว 3 แบบ
4.1 ตัวเรียว (Taper Tap) เป็นตัวทำเกลียวตัวแรกหลังจากที่ใช้ดอกสว่านเจาะรูแล้ว โดยส่วนปลายเกลียวจะมีความเรียวอยู่ประมาณ 6-7 ฟัน
4.2 ตัวตาม (Plug Tap) ถ้าเกลียวที่ต้องการมีความหนามากขึ้นและตรงปลายมีความเรียวอยู่ที่ 3-4 ฟัน หลังจากใช้เกลียวตัวแรกแล้วก็ใช้เกลียวตัวตามต่อเพื่อสร้างเกลียวให้มีขนาดที่ต้องการได้ และเกลียวนี้สามารถใช้แทนเกลียวตัวแรกได้เลยหากวัสดุที่ต้องการทำเกลียวนั้นไม่แข็งจนเกินไป
4.3 ตัวสุดท้าย (Bottoming Tap) เกลียวตัวนี้จะไม่มีส่วนที่เรียวเลย จึงใช้เป็นตัวสุดท้ายเพื่อทำให้เกลียวที่ต้องการต๊าปนั้นสมบูรณ์
5. ดอกต๊าปรีดเกลียว (Forming Tap)
ดอกต๊าปรีดเกลียว (Forming Tap)
ดอกต๊าปรีดเกลียวสร้างเกลียวด้วยการรีดหรืออัดขึ้นรูปวัสดุภายในรู ทำให้ในระหว่างการทำเกลียวจะไม่มีเศษเกิดขึ้นเลย เนื่องจากเศษถูกอัดเข้าไปในเนื้องาน ทำให้ข้อดีของดอกต๊าปชนิดนี้คือไม่สร้างเศษในระหว่างทำเกลียว และวัสดุที่ถูกสร้างเกลียวก็ยังมีความแข็งแรงขึ้นเนื่องจากเศษวัสดุได้อัดเข้าไปในเนื้อวัสดุ
ดอกต๊าปรีดเกลียวเหมาะกับการสร้างเกลียวให้กับวัสดุประเภทที่ไม่มีความแข็งมาก จึงเหมาะกับวัสดุ เช่น เหล็กคาร์บอนต่ำ หรืออลูมิเนียม
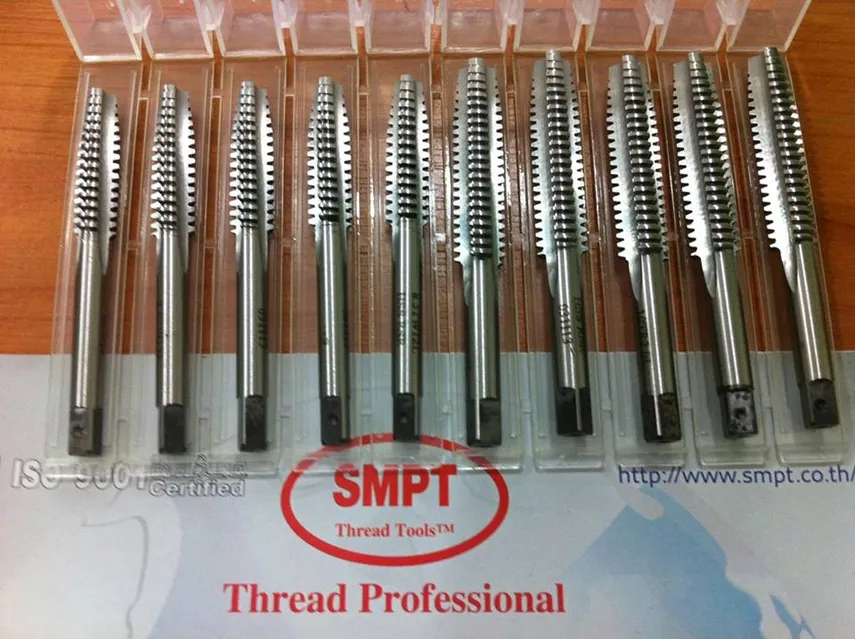

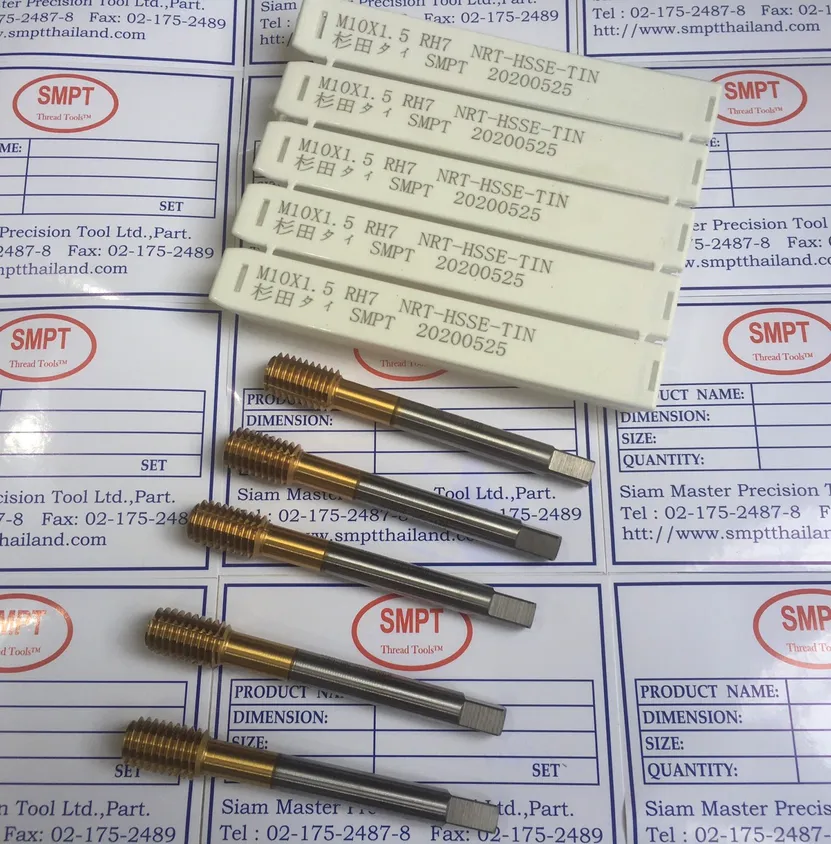
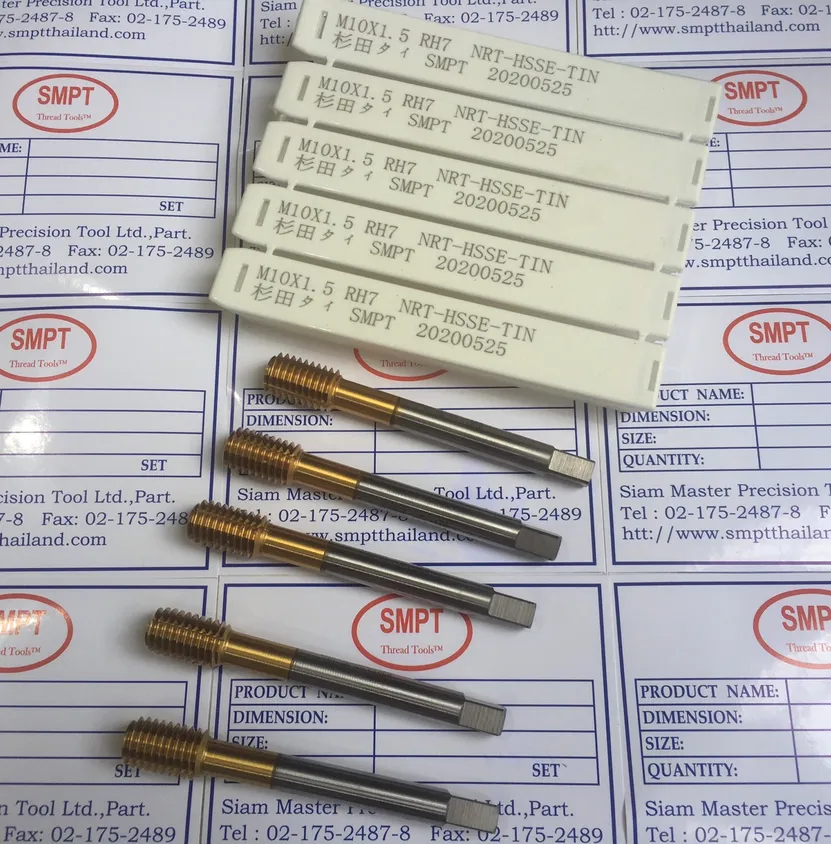
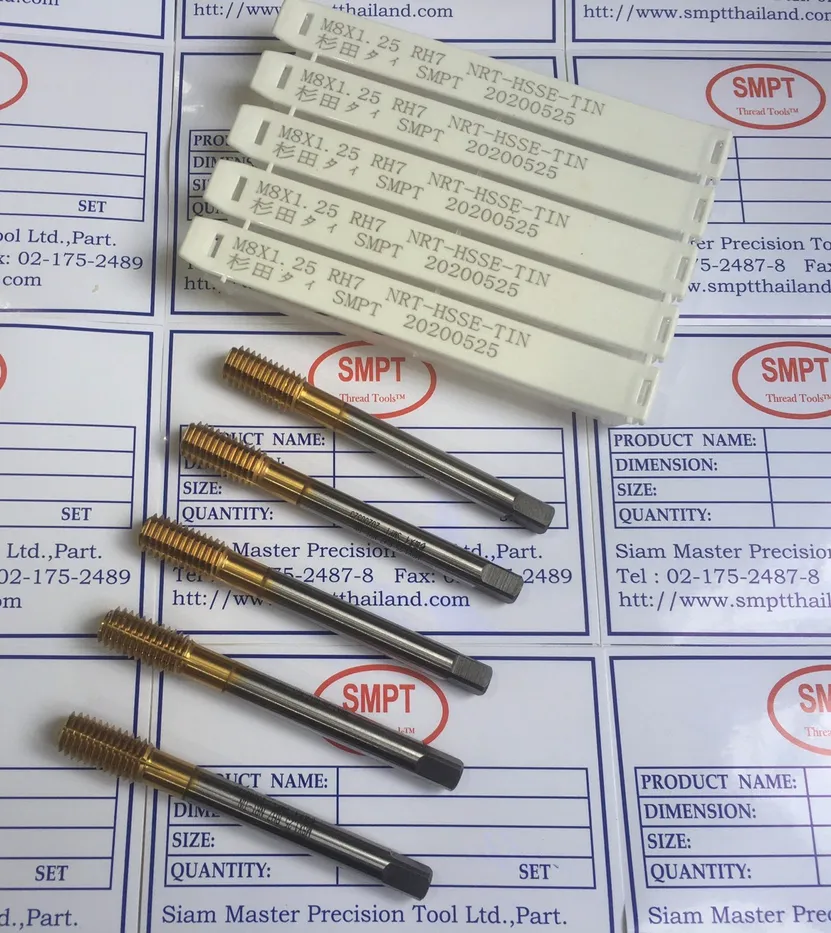
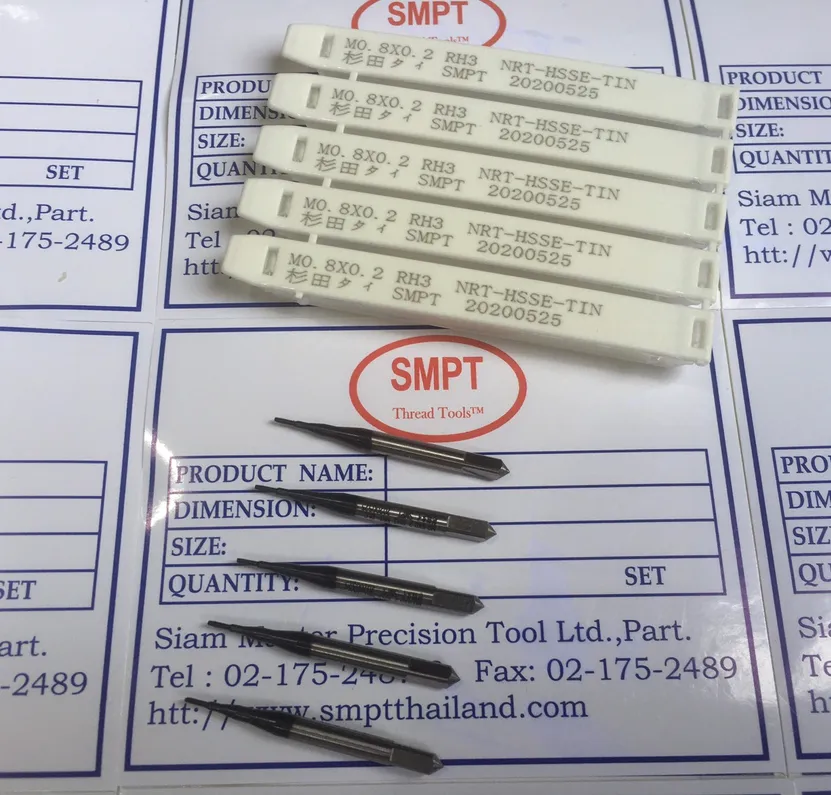
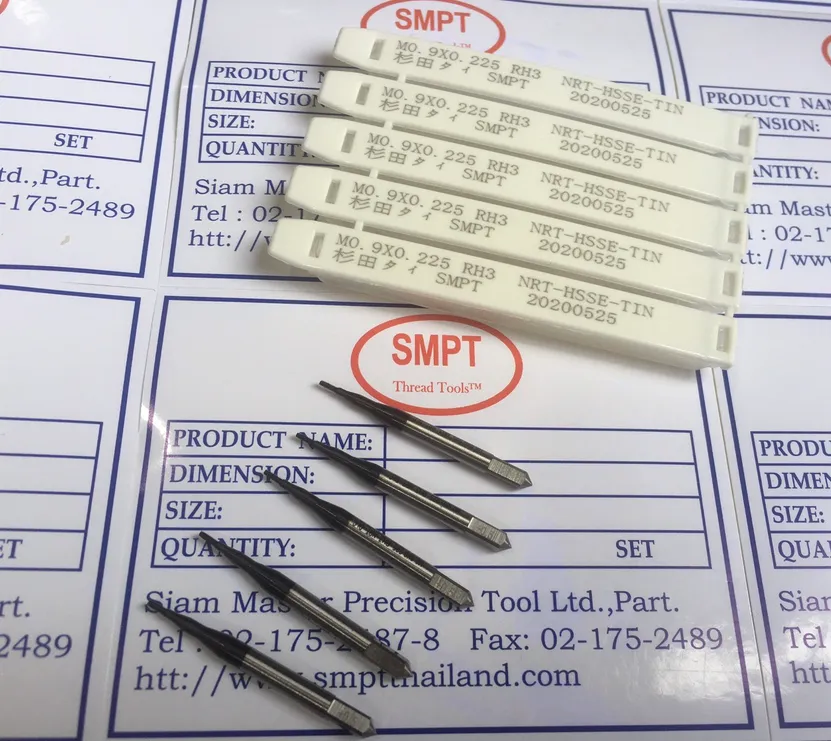
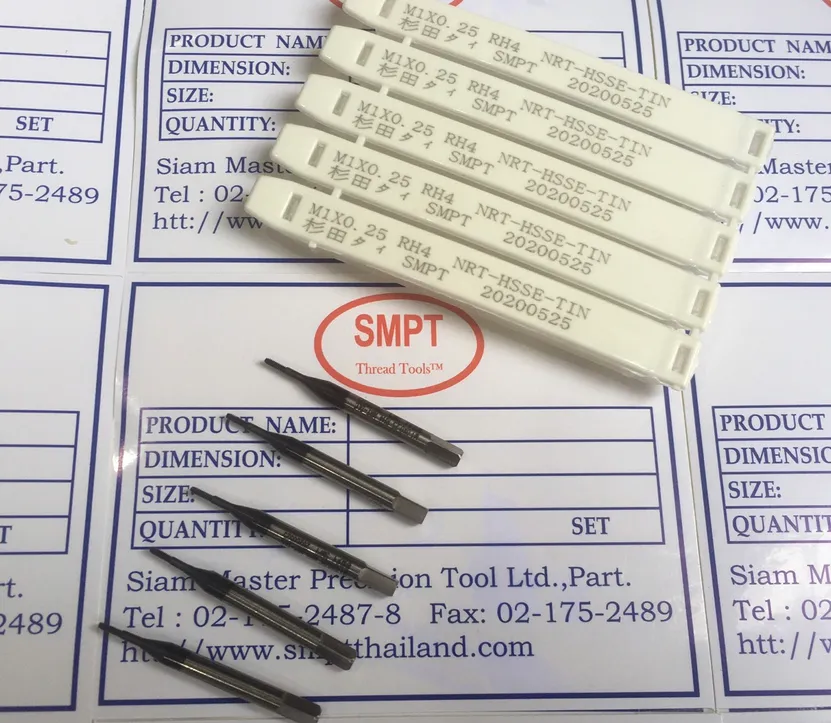
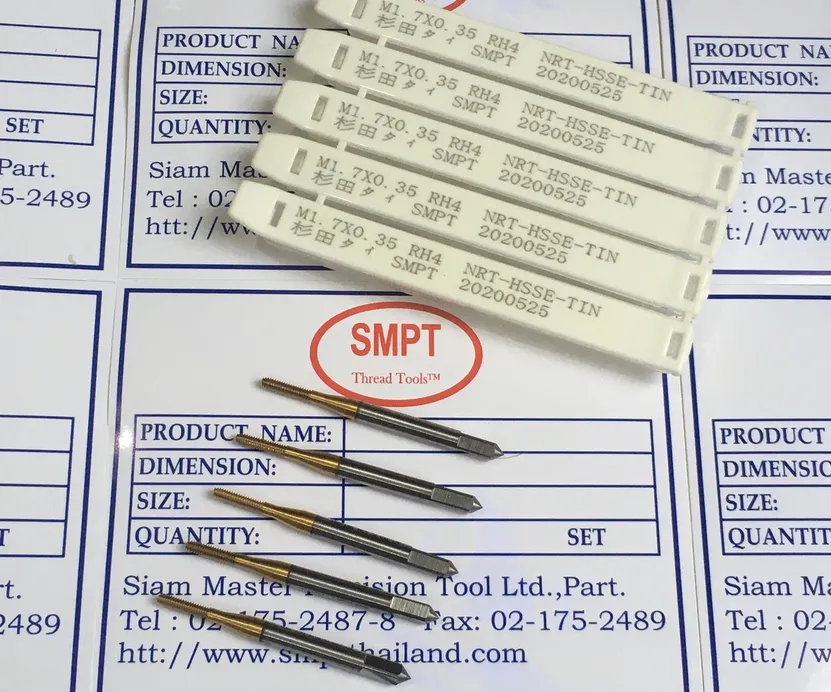
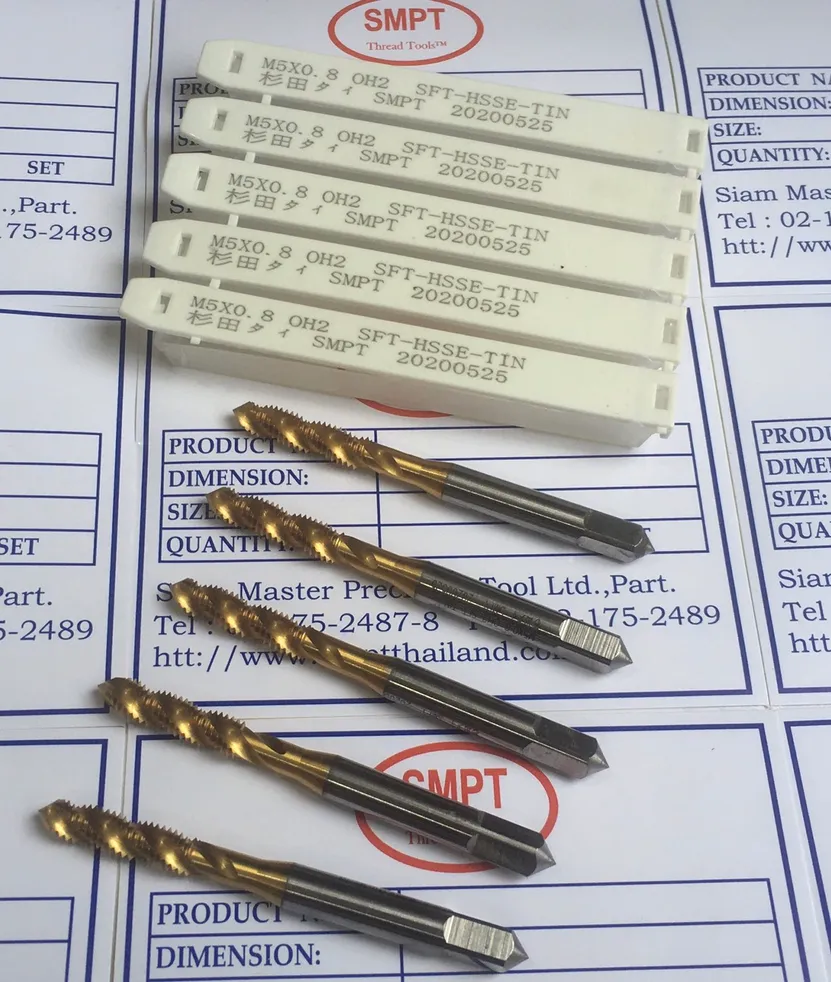
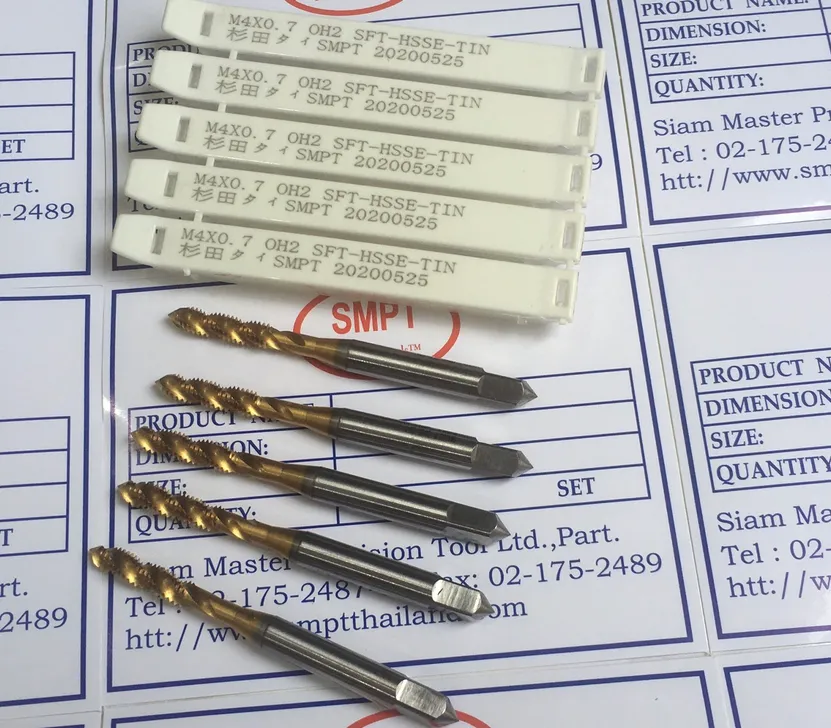
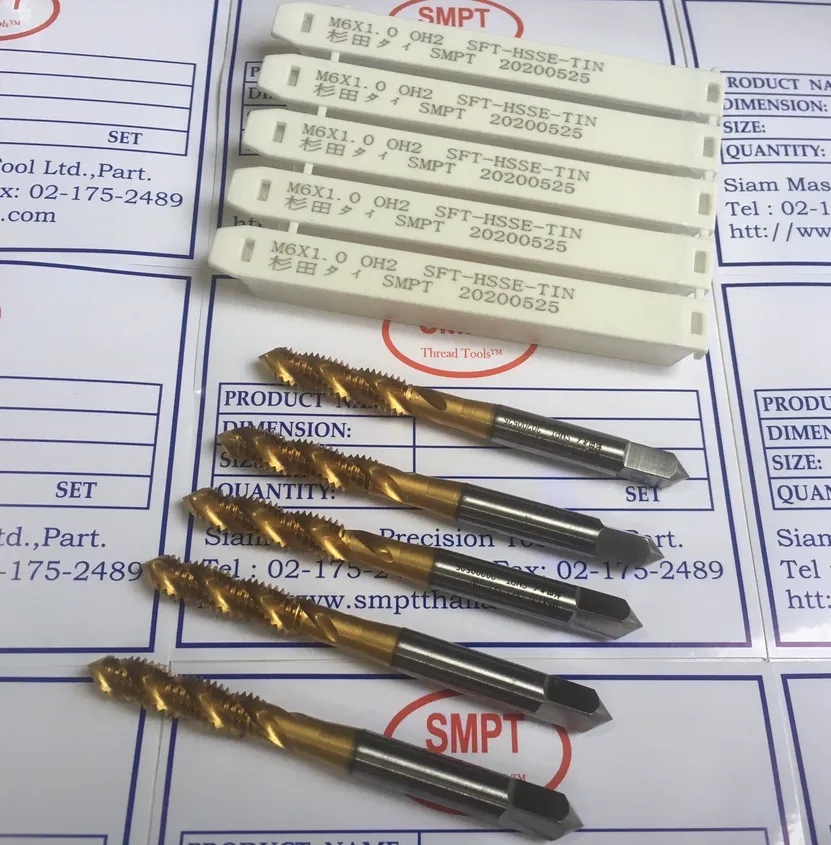
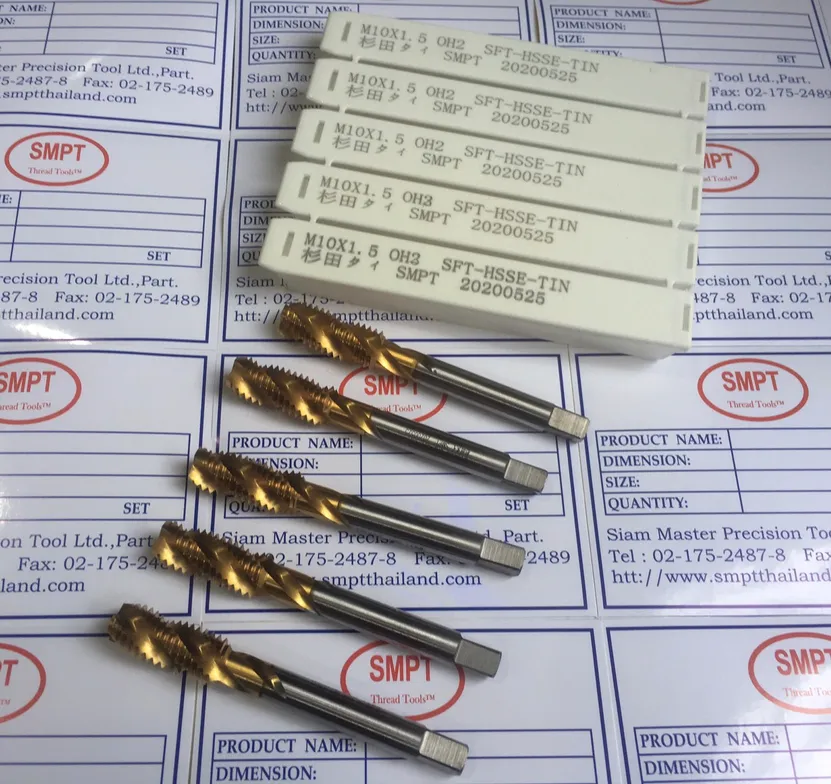
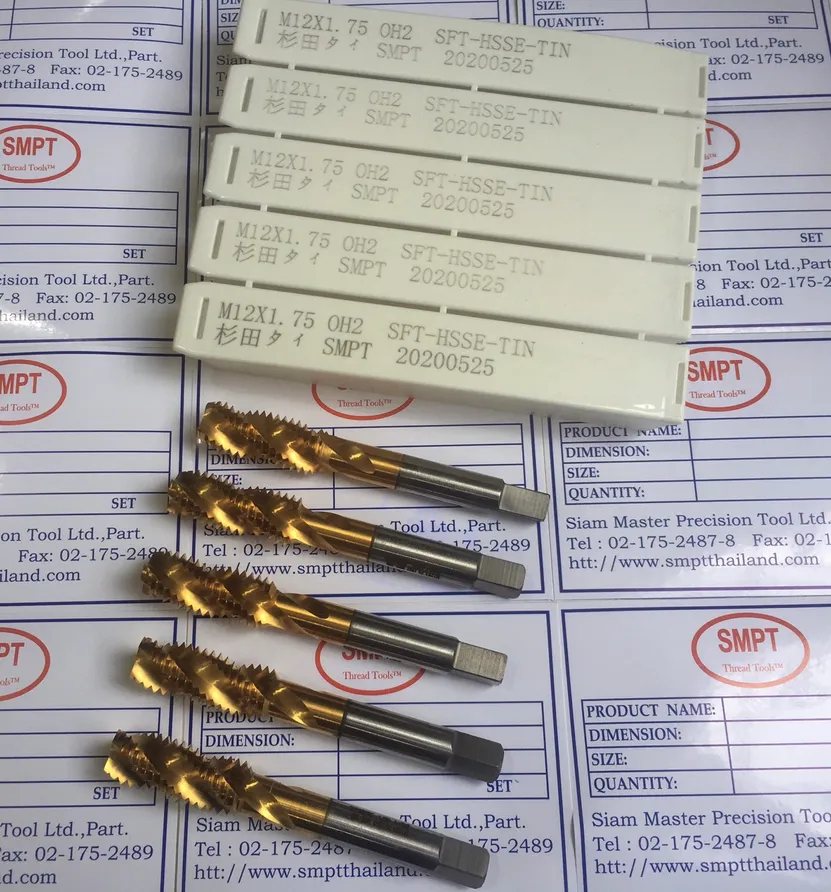
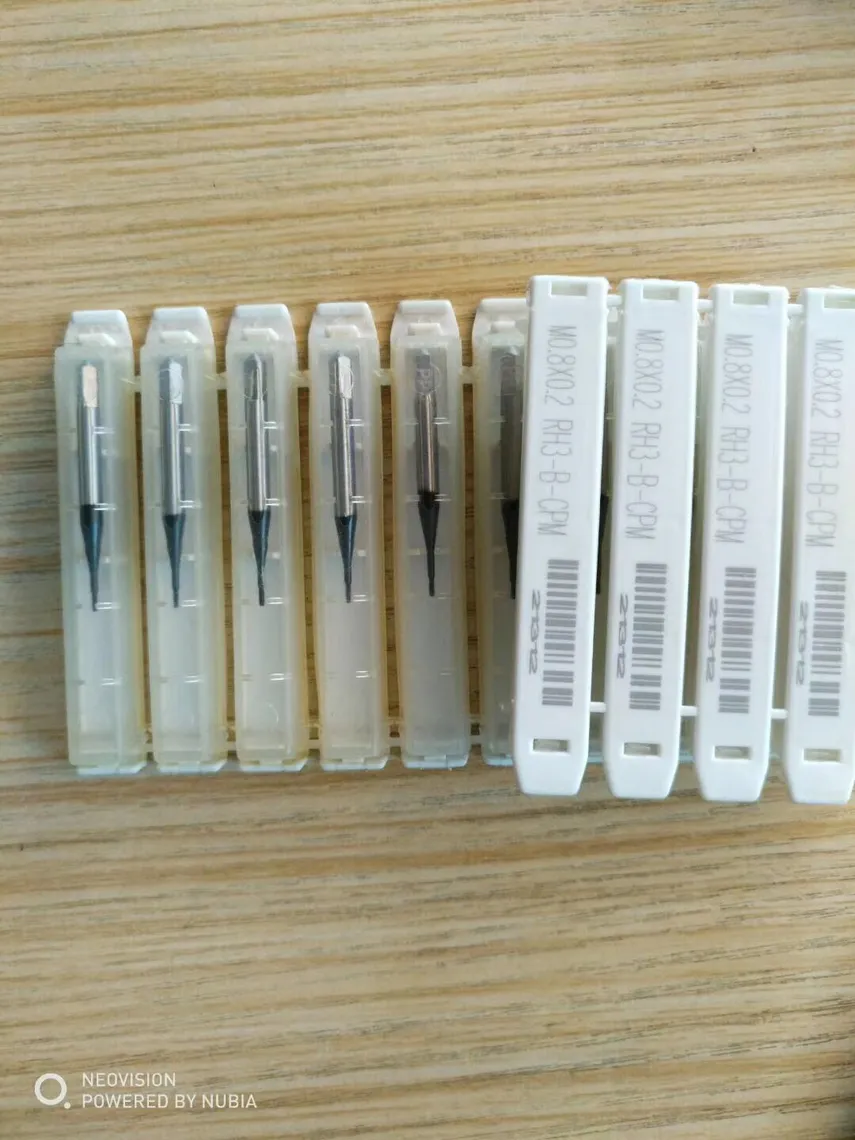
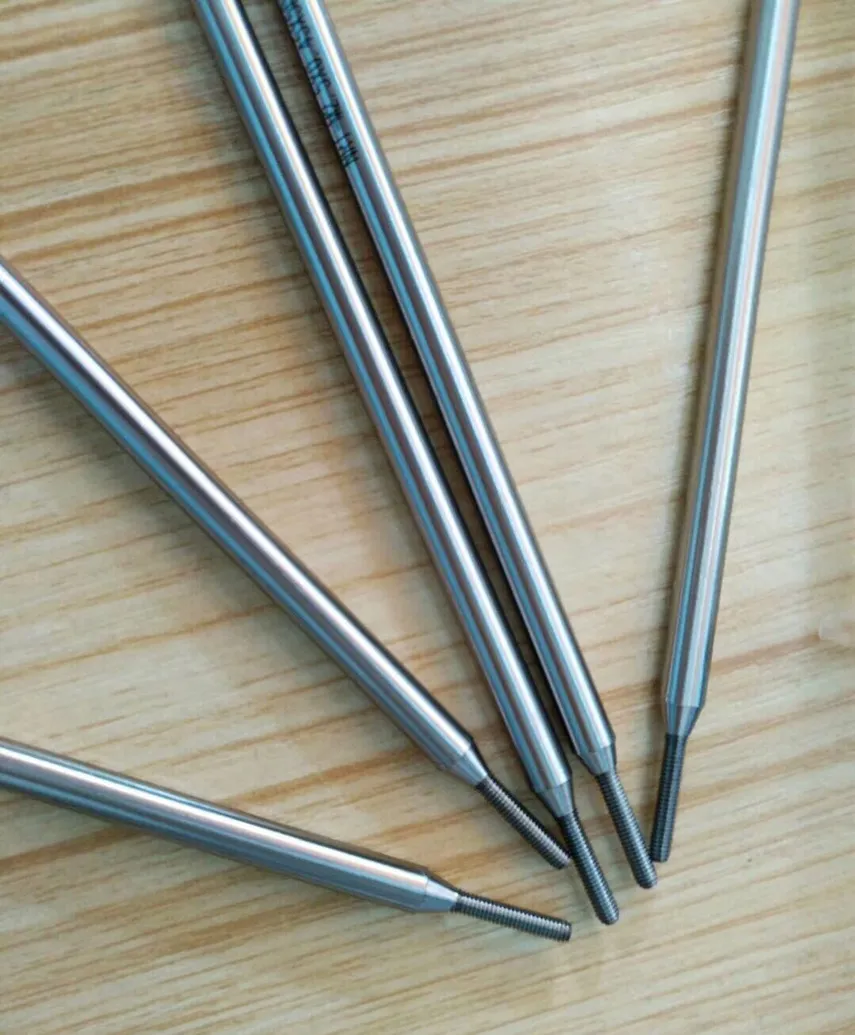
Forming Tap (FlutelessTap) ต๊าปไร้เศษ ต๊าฟรีดเกลียว(มีสต๊อก)ต๊าฟจิ๋ว Microtap Small
M0.5X0.125, M0.6X0.15, M0.7X0.175 ,M0.8X0.2, M0.9X0.22, M1.0X0.25, M1.1X0.25, M1.2X0.25,M1.4X0.3, M1.5X0.35,
M1.6X0.35, M1.7X0.35, M1.8X0.35, M2X0.4 ,M2.5X0.45, M3X0.5 ,M3.5X0.6,M4X0.7 ,M5X0.8 ,M6X1.0 ,M8X1.25 ,M8X1.0
,M10X1.5 ,M10X1.25 ,M12X1.75 ,M12X1.25
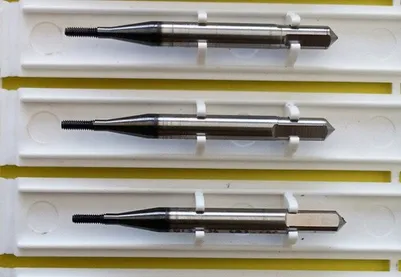
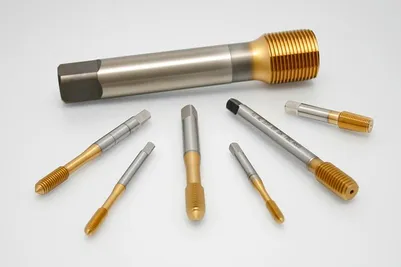
Forming Tap (FlutelessTap) ต๊าปไร้เศษ ต๊าฟรีดเกลียว(มีสต๊อก)ต๊าฟจิ๋ว Microtap Small
M0.5X0.125, M0.6X0.15, M0.7X0.175 ,M0.8X0.2, M0.9X0.22, M1.0X0.25, M1.1X0.25, M1.2X0.25,M1.4X0.3, M1.5X0.35,
M1.6X0.35, M1.7X0.35, M1.8X0.35, M2X0.4 ,M2.5X0.45, M3X0.5 ,M3.5X0.6,M4X0.7 ,M5X0.8 ,M6X1.0 ,M8X1.25 ,M8X1.0
,M10X1.5 ,M10X1.25 ,M12X1.75 ,M12X1.25
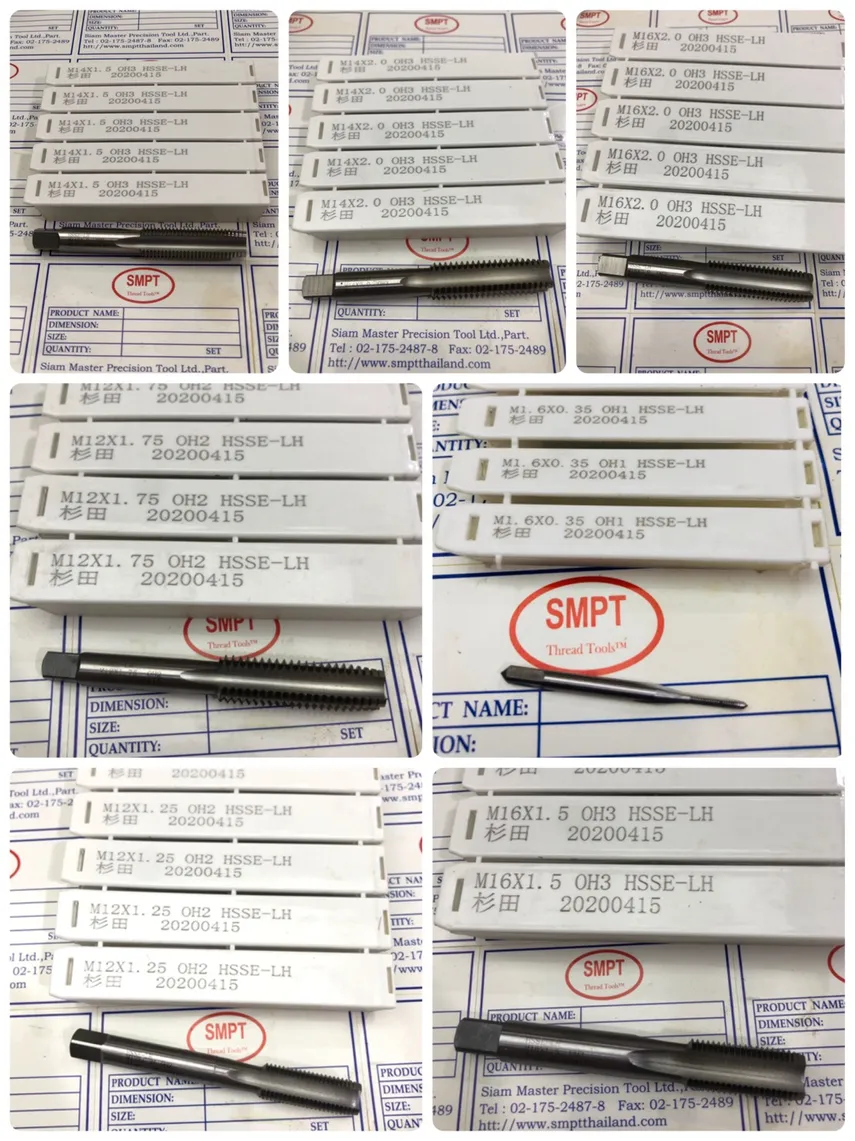
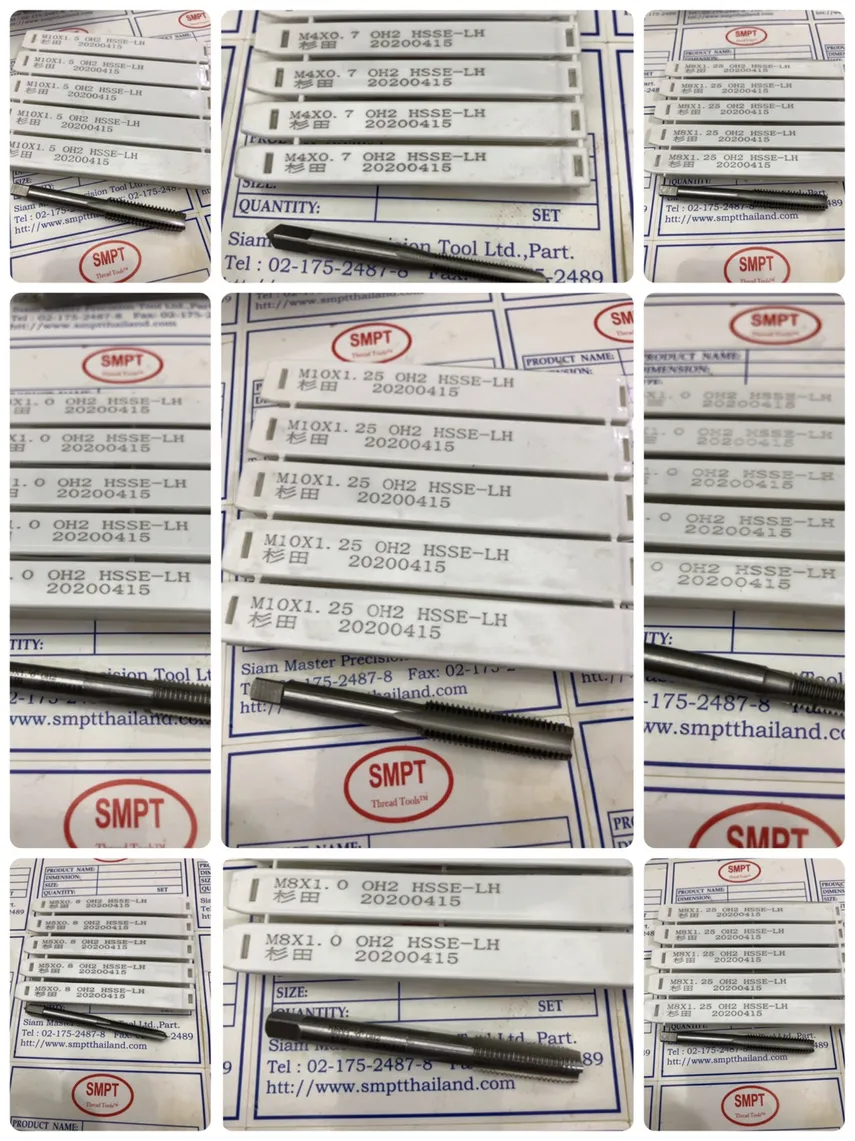
ดอกต๊าปเกลียวพิเศษ ที่ทางเราผลิตเก็บไว้ในสต๊อก
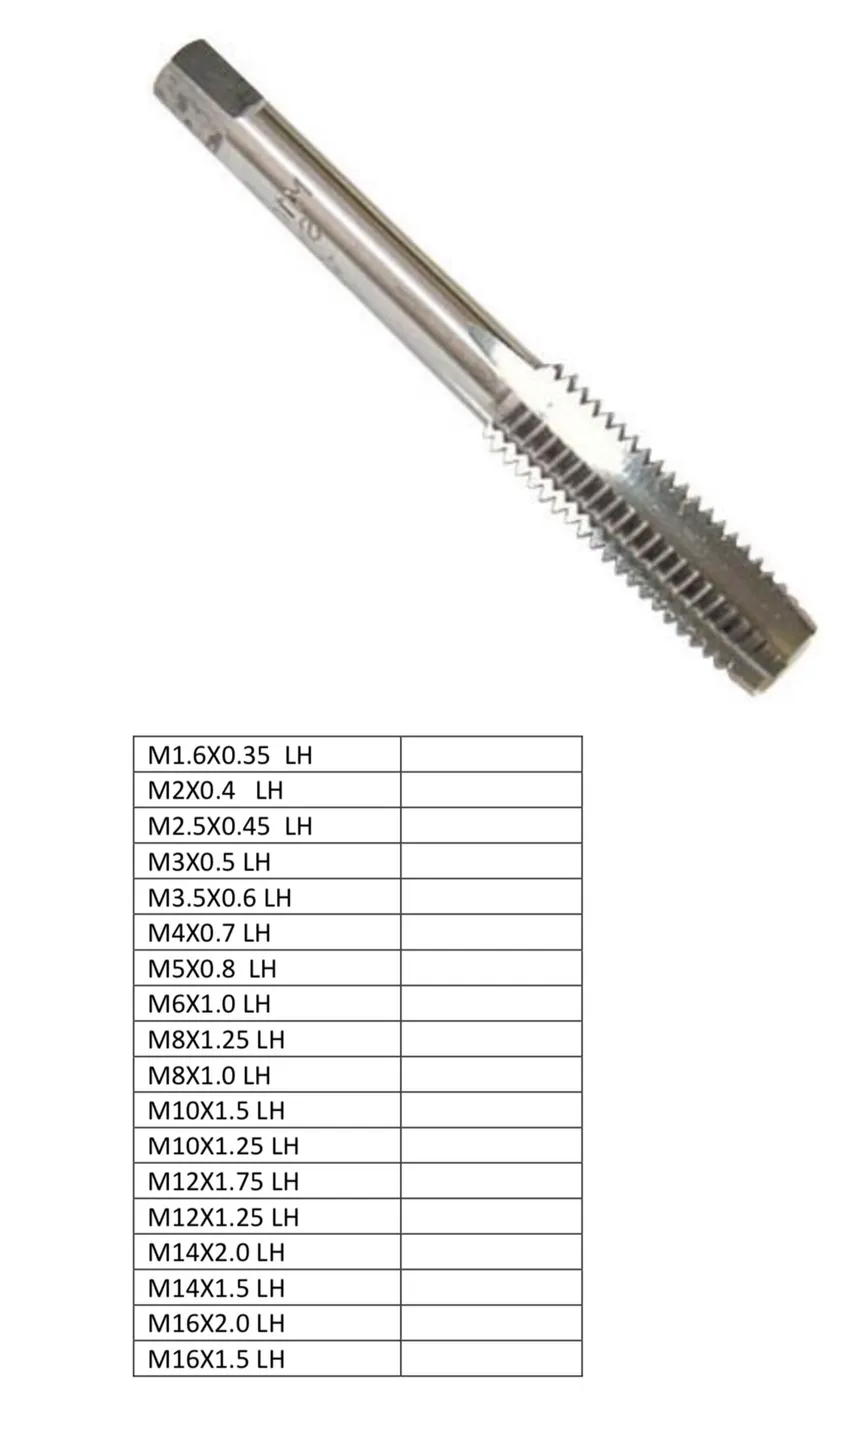
ดอกต๊าฟเกลียวซ้าย Hand Tap for Left-Hand Threads Material: HSS SKH59 Carbide
M1.6X0.35 LH , M2X0.4 LH,M2.5X0.45 LH,M3X0.5 LH,M3.5X0.6 LH,M4X0.7 LH,M5X0.8 LH,M6X1.0 LH,M8X1.25 LH,M8X1.0 LH,M10X1.5 LH,M10X1.25 LH,M12X1.75 LH,M12X1.25 LH,M14X2.0 LH,M14X1.5 LH,M16X2.0 LH,M16X1.5 LH
Rd-Series Knuckle Thread Chart DIN 405
Tap Valve (Internal thread & External Thread) GAS Thailand
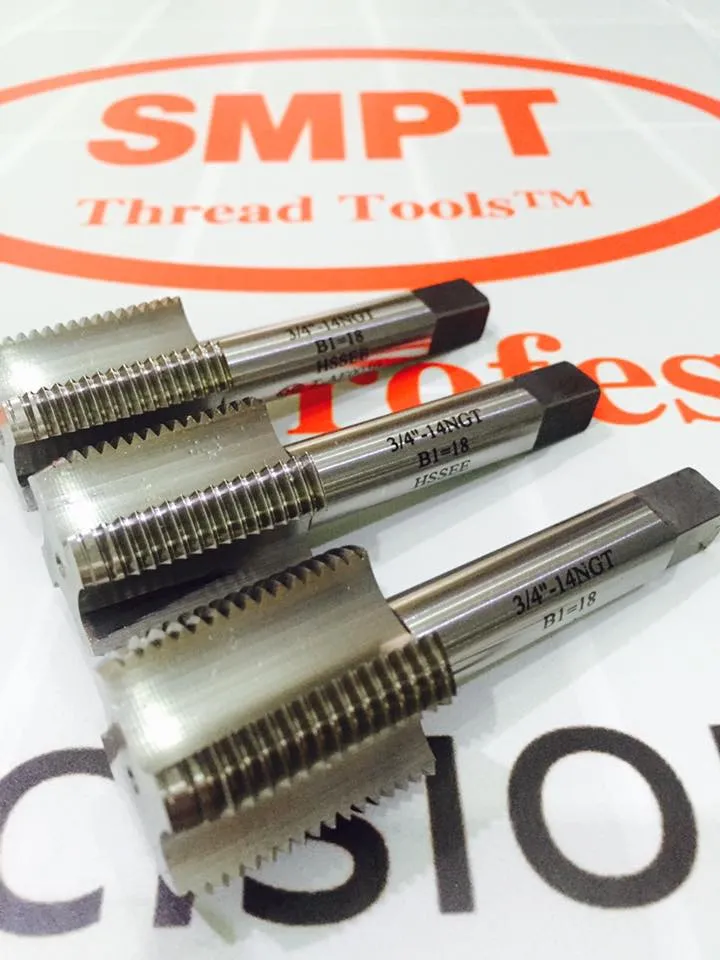
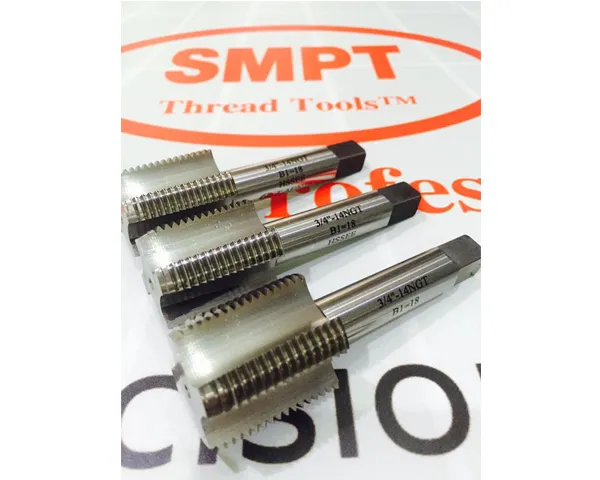
Inlet : 3/4" - 14NGT
Outlet : 0.885 - 14 NGO - LH - INT
Inlet : 3/4" - 14NGT
Outlet : 1.312 - 5 ACME - 2G - RH - EXT, 0.885 - 14 UNS - LH - INT
Inlet : W 28.8 - 14 DIN 477
Outlet : 5/8" - 14 BSPF - LH - INT
Inlet : 3/4" - 14NGT
Outlet : 7/16 - 20 UNF
Inlet : 3/4" - 14NGT
Outlet : 1.312 - 5 ACME - 2G - RH - EXT, 0.885 - 14 UNS - LH - INT
Inlet : W 19.3 - 14
Outlet : W 21.8 - 14 - LH - EXT
Inlet : W 28.8 - 14 DIN 477
Outlet : W 21.8 - 14 - LH - EXT
Inlet : W 28.8 - 14 DIN 477
Outlet : W 20 - 14 - LH - EXT
Inlet : M 25.5 X 2
Outlet : W 20 - 14 - LH - EXT
Inlet : W 19.3 - 14
Outlet : W 21.8 - 14 - LH - EXT
Inlet : W 19.8 - 14 DIN 477
Outlet : W 21.8 - 14 - LH - EXT
1/2" - 14NGT
Inlet : M22 X 1.25
Outlet : M 16 x 1.5
Inlet : 0.715 - 14
Outlet : 3/8" - 19BSPF - LH
Outlet : M 12 x 0.75
#ROUNDSCREWTHREADSDIN405
#Rd thread plug gauge & RD TAP
#spiraltap
LINE:smpt
Tel:021752487
#DIN405
Rd 8 x 1/10"
Rd 9 x 1/10"
Rd 10 x 1/10"
Rd 11 x 1/10"
Rd 12 x 1/10"
Rd 14 x 1/8"
Rd 16 x 1/8"
Rd 18 x 1/8"
Rd 20 x 1/8"
Rd 22 x 1/8"
Rd 24 x 1/8"
Rd 28 x 1/8"
Rd 30 x 1/8"
Rd 32 x 1/8"
Rd 34 x 1/8"
Rd 36 x 1/8"
Rd 38 x 1/8"
Rd 40 x 1/6"
Rd 42 x 1/6"
Rd 44 x 1/6"
Rd 46 x 1/6"
Rd 48 x 1/6"
Rd 50 x 1/6"
Rd 52 x 1/6"
Rd 55 x 1/6"
Rd 58 x 1/6"
Rd 60 x 1/6"
Rd 62 x 1/6"
Rd 65 x 1/6"
Rd 68 x 1/6"
Rd 70 x 1/6"
Rd 72 x 1/6"
Rd 75 x 1/6"
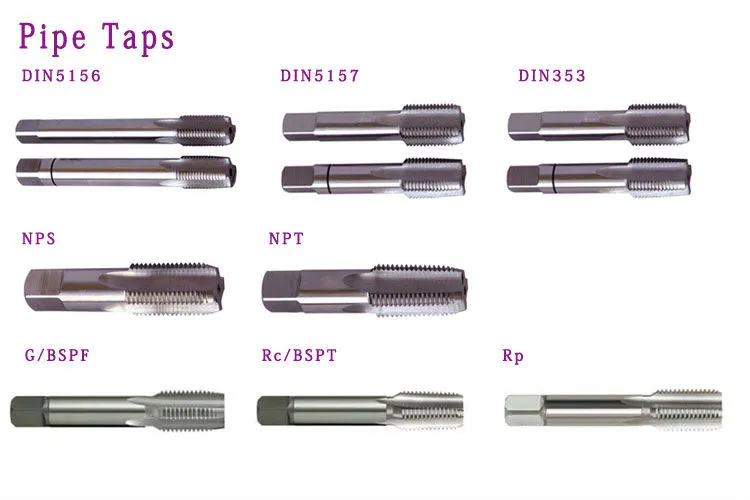
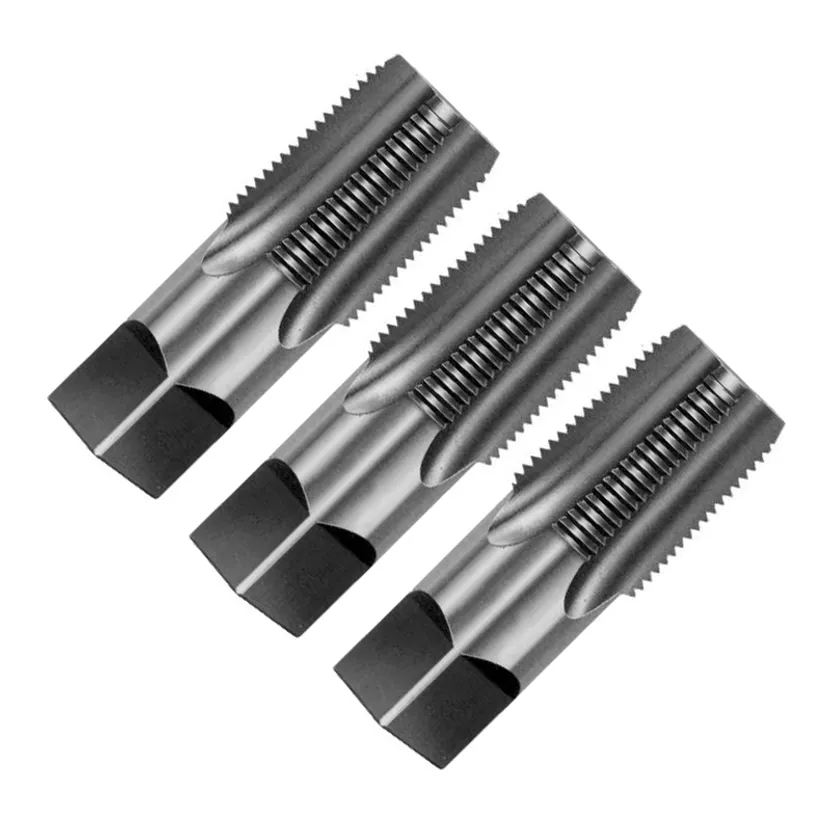
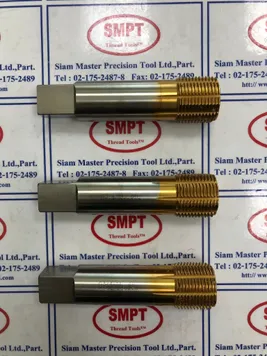
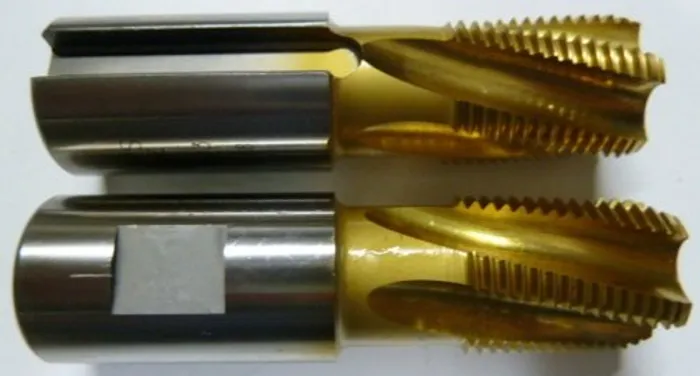
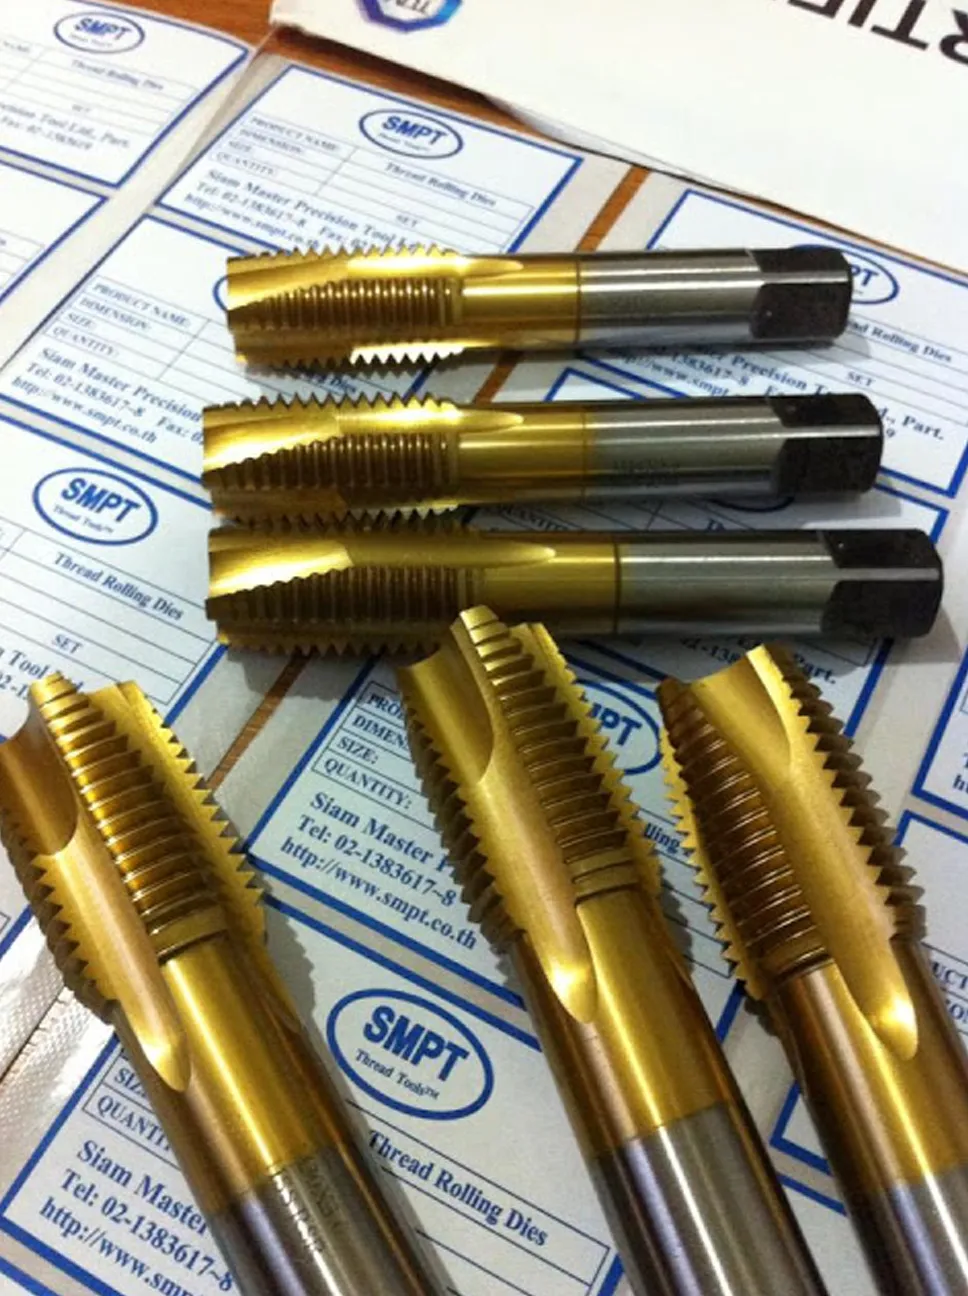
Taper Pipe Tap used for tapping pipe fittings and couplings in a wide variety of materials.
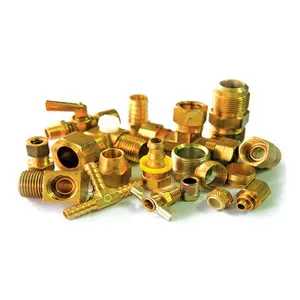
ดอกต๊าปเกลียวสำหรับต๊าปเกลียวข้อต่อทองเหลือง ดอกต๊าปเกลียวข้อต่อทองเหลือง (Brass Fitting Tap )
ดอกต๊าปเกลียวสำหรับต๊าปเกลียวข้อต่อทองเหลือง ดอกต๊าปเกลียวข้อต่อทองเหลือง (Brass Fitting Tap )
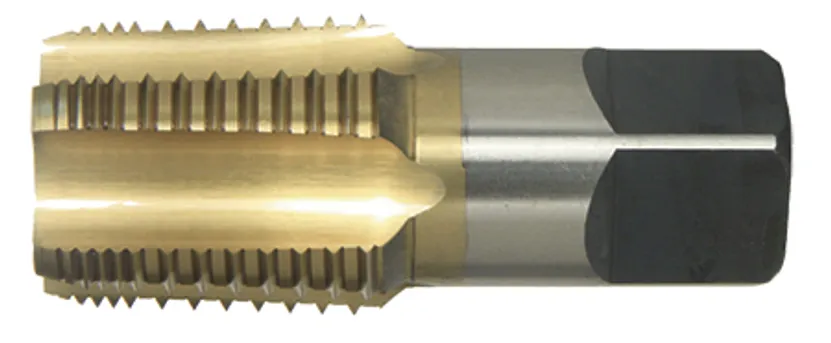
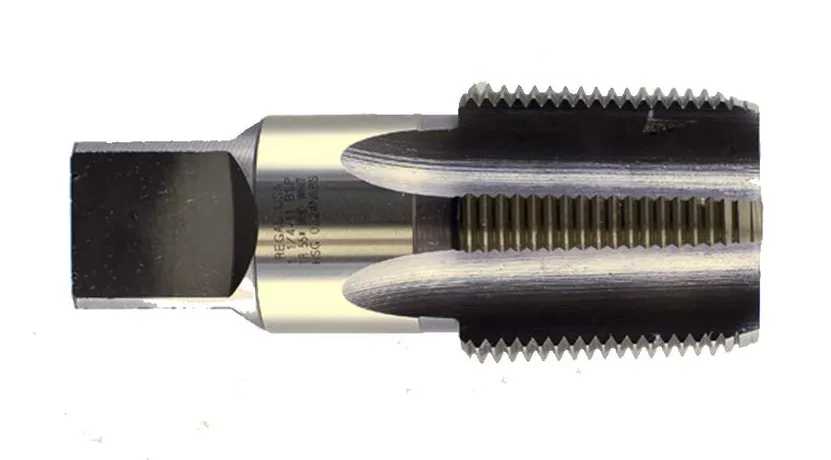
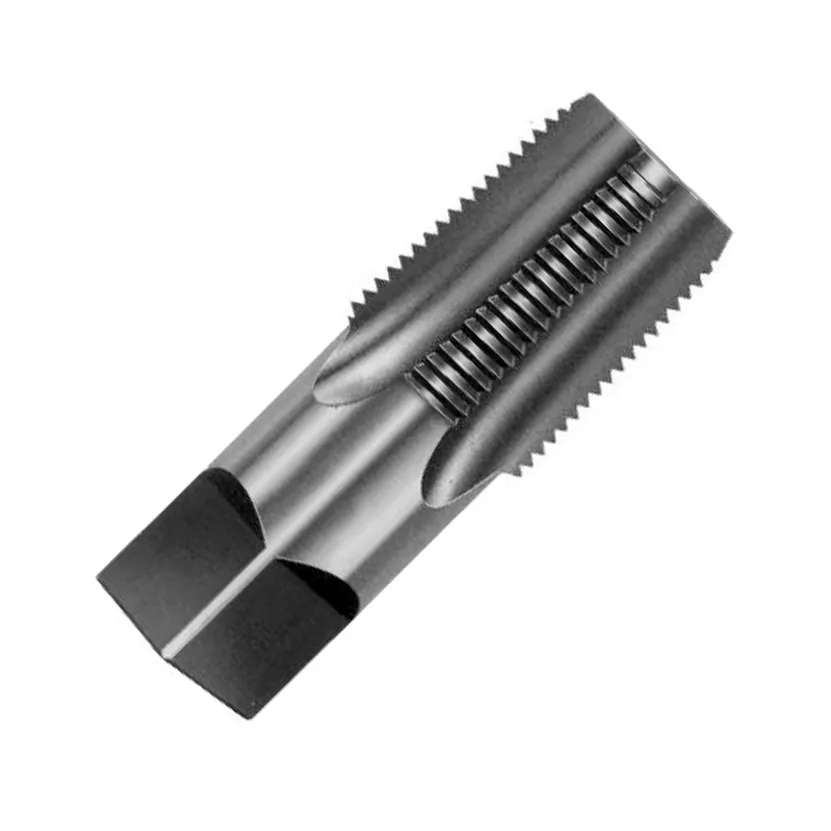
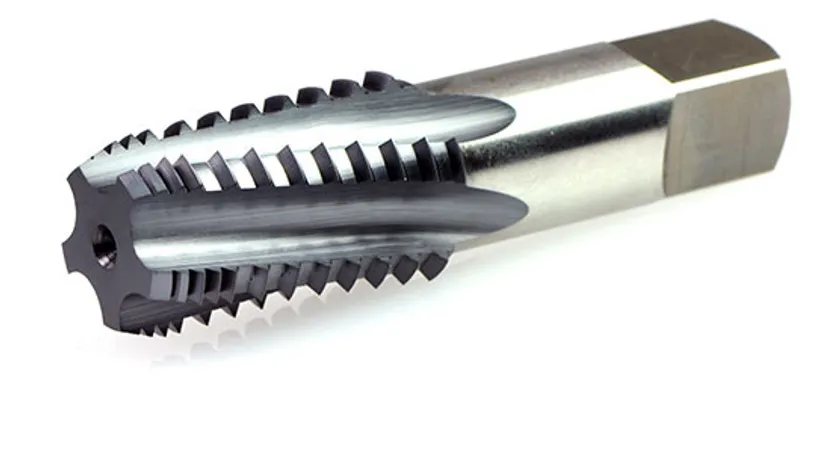
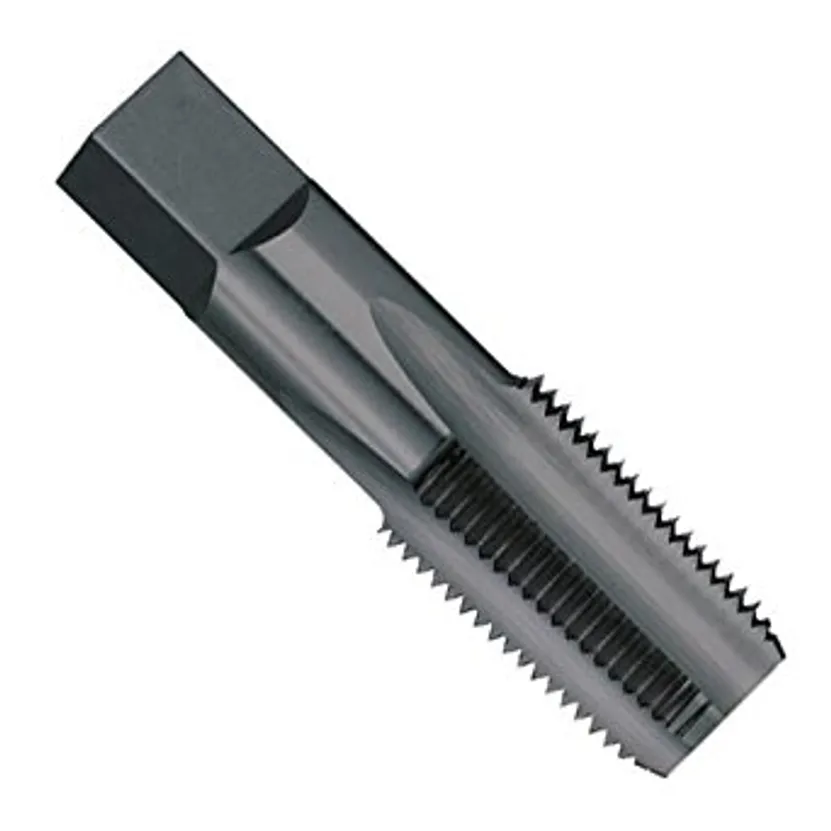
NPT, BSPP and BSPT
| ด้ามต๊าป Tap Shank Dimensions | Tap thread size for various Industry Standards |
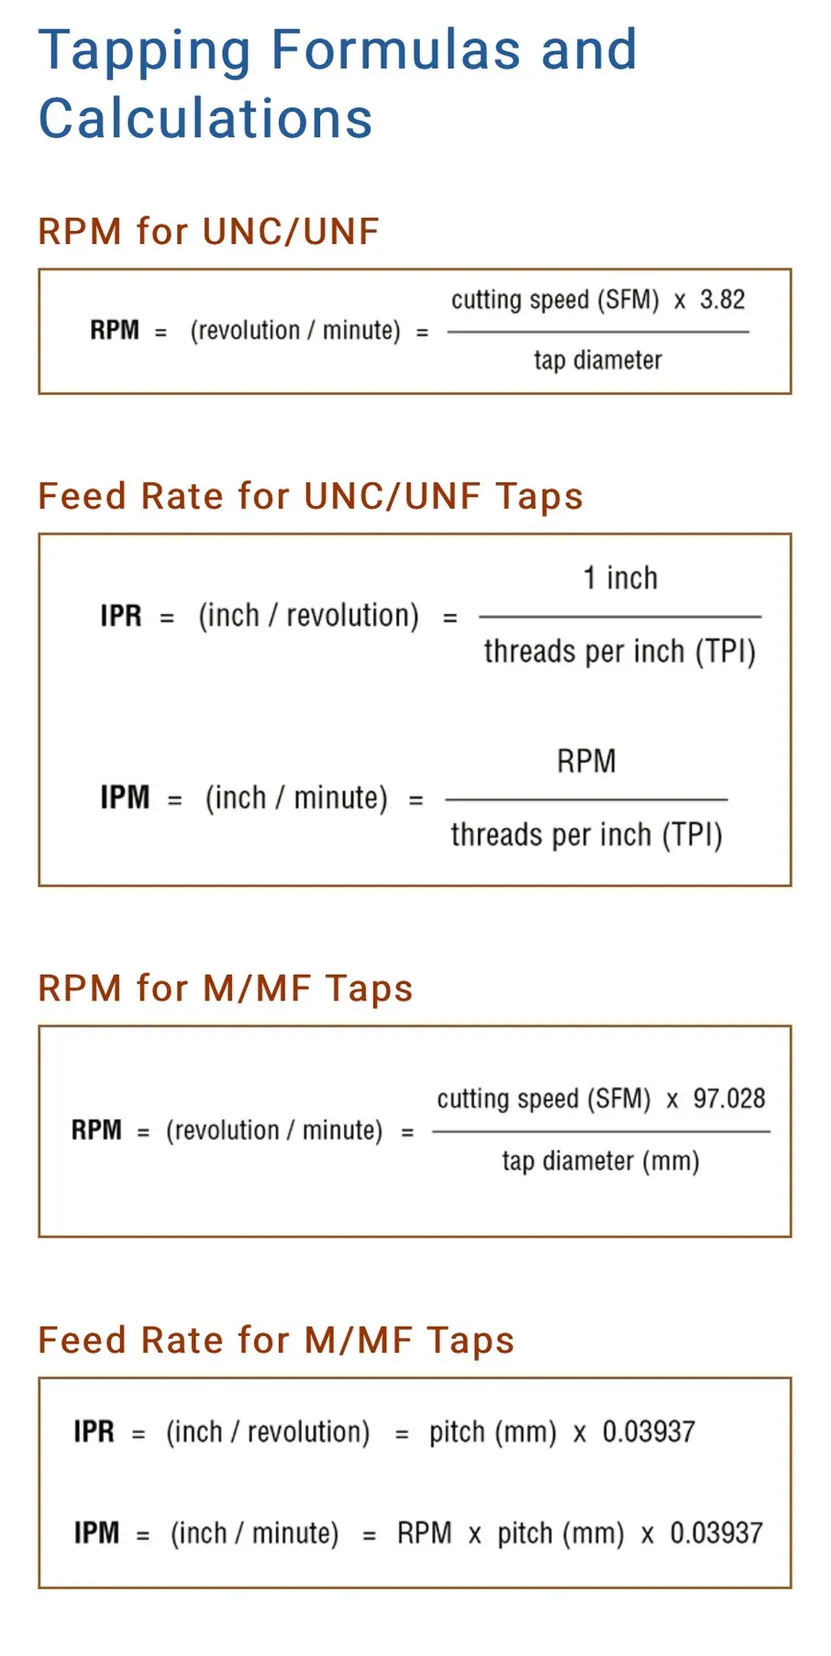
Tapping Formulas and Calculations
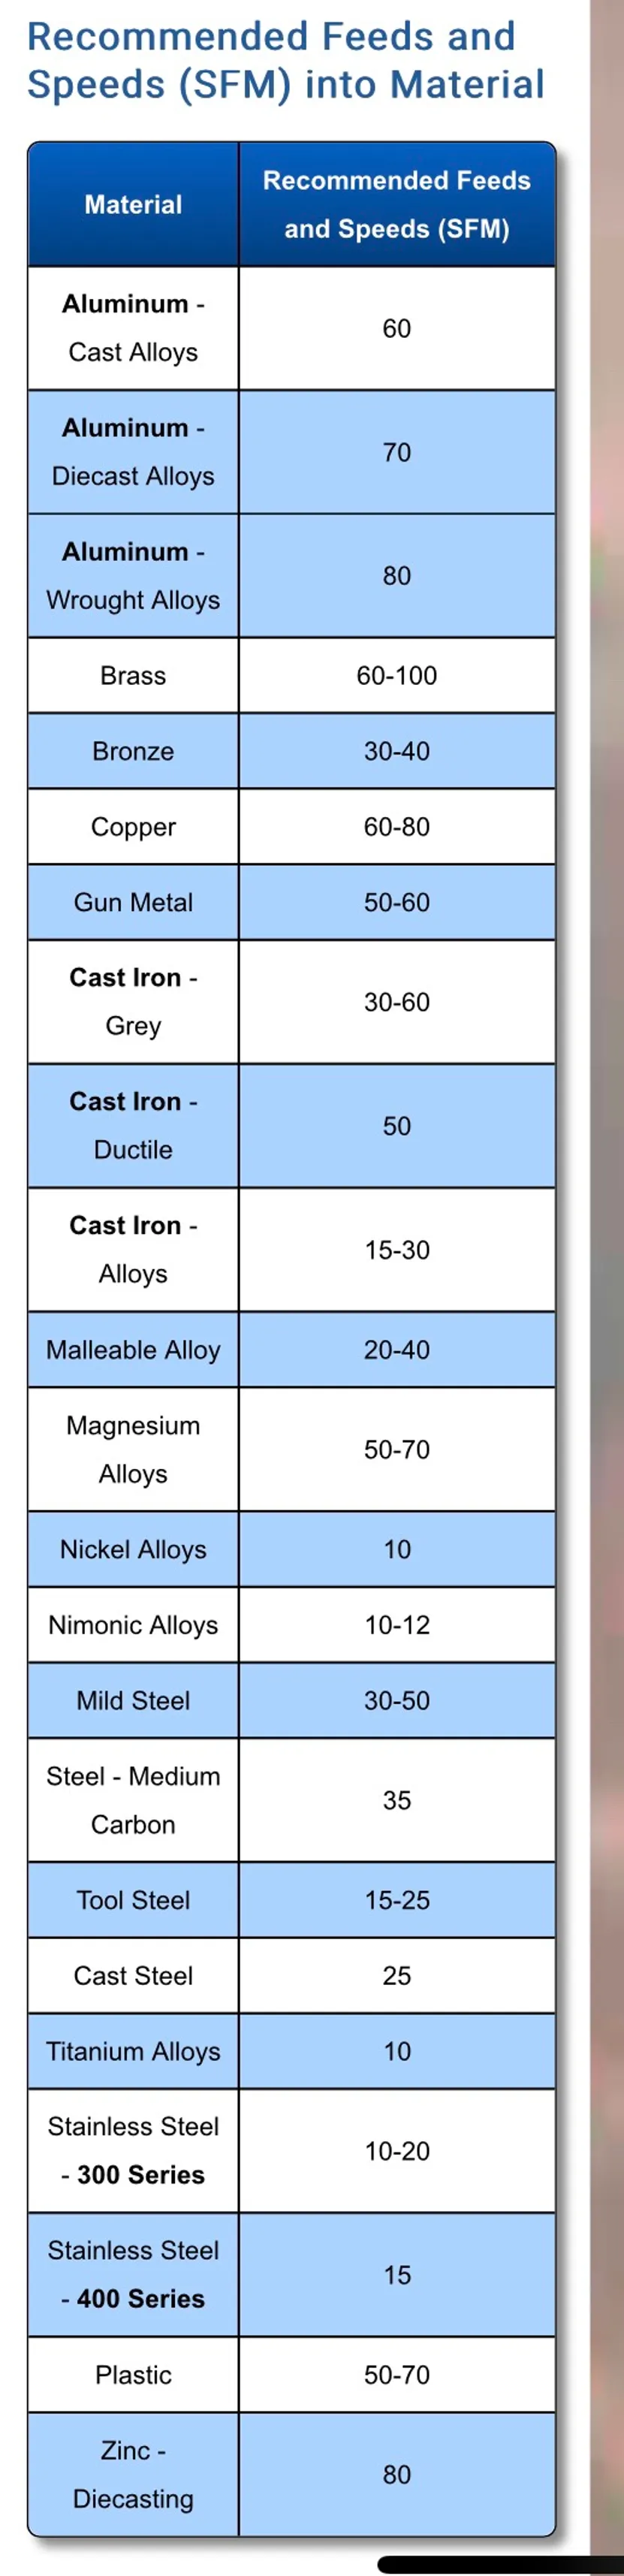
M0.25x0.075
M0.25x0.075
ธนะพัฒน์ เลิศรัตนศักดิ์ดา วิศวกรเชี่ยวชาญเรื่องเครื่องมืออุตสาหกรรมและนักธุรกิจ
M0.3x0.08
M0.3x0.08
M0.3x0.09
M0.3x0.09
M0.35x0.09
M0.35x0.09
M0.4x0.1
M0.4x0.1
M0.45x0.1
M0.45x0.1
M0.5x0.125
M0.5x0.125
M0.55x0.125
M0.55x0.125
M0.6x0.15
M0.6x0.15
M0.7x0.175
M0.7x0.175
M0.8x0.2
M0.8x0.2
M0.9x0.225
M0.9x0.225
M1x0.25
M1x0.25
M1x0.2
M1x0.2
M1.1x0.25
M1.1x0.25
M1.1x0.2
M1.1x0.2
M1.2x0.25
M1.2x0.25
M1.2x0.2
M1.2x0.2
M1.4x0.3
M1.4x0.3
M1.4x0.2
M1.4x0.2
M1.6x0.35
M1.6x0.35
M1.6x0.2
M1.6x0.2
M1.7x0.35
M1.7x0.35
M1.8x0.35
M1.8x0.35
M1.8x0.2
M1.8x0.2
M2x0.4
M2x0.4
M2x0.25
M2x0.25
M2.2x0.45
M2.2x0.45
M2.2x0.25
M2.2x0.25
M2.3x0.45
M2.3x0.45
M2.3x0.4
M2.3x0.4
M2.5x0.45
M2.5x0.45
M2.5x0.35
M2.5x0.35
M2.6x0.45
M2.6x0.45
M3x0.5
M3x0.5
M3x0.35
M3x0.35
M3.5x0.6
M3.5x0.6
M3.5x0.35
M3.5x0.35
M4x0.7
M4x0.7
M4x0.5
M4x0.5
M4.5x0.75
M4.5x0.75
M4.5x0.5
M4.5x0.5
M5x0.8
M5x0.8
M5x0.5
M5x0.5
M5.5x0.5
M5.5x0.5
M6x1
M6x1
M6x0.75
M6x0.75
M6x0.7
M6x0.7
M6x0.5
M6x0.5
M7x1
M7x1
M7x0.75
M7x0.75
M7x0.5
M7x0.5
M8x1.25
M8x1.25
M8x1
M8x1
M8x0.8
M8x0.8
M8x0.75
M8x0.75
M8x0.5
M8x0.5
M9x1.25
M9x1.25
M9x1
M9x1
M9x0.75
M9x0.75
M9x0.5
M9x0.5
M10x1.5
M10x1.5
M10x1.25
M10x1.25
M10x1.12
M10x1.12
M10x1
M10x1
M10x0.75
M10x0.75
M10x0.5
M10x0.5
M11x1.5
M11x1.5
M11x1
M11x1
M11x0.75
M11x0.75
M11x0.5
M11x0.5
M12x1.75
M12x1.75
M12x1.5
M12x1.25
M12x1.25
M12x1
M12x1
M12x0.75
M12x0.75
M12x0.5
M12x0.5
M14x2
M14x2
M14x1.5
M14x1.5
M14x1.25
M14x1.25
M14x1
M14x1
M14x0.75
M14x0.75
M14x0.5
M14x0.5
M15x1.5
M15x1.5
M15x1
M15x1
M16x2
M16x2
M16x1.5
M16x1.5
M16x1.25
M16x1.25
M16x1
M16x1
M16x0.75
M16x0.75
M16x0.5
M16x0.5
M17x1.5
M17x1.5
M17x1
M17x1
M18x2.5
M18x2.5
M18x2
M18x2
M18x1.5
M18x1.5
M18x1.25
M18x1.25
M18x1
M18x1
M18x0.75
M18x0.75
M18x0.5
M18x0.5
M20x2.5
M20x2.5
M20x2
M20x2
M20x1.5
M20x1.5
M20x1
M20x1
M20x0.75
M20x0.75
M20x0.5
M20x0.5
M22x3
M22x3
M22x2.5
M22x2.5
M22x2
M22x2
M22x1.5
M22x1.5
M22x1
M22x1
M22x0.75
M22x0.75
M22x0.5
M22x0.5
M24x3
M24x3
M24x2.5
M24x2.5
M24x2
M24x2
M24x1.5
M24x1.5
M24x1
M24x1
M24x0.75
M24x0.75
M25x2
M25x2
M25x1.5
M25x1.5
M25x1
M25x1
M26x1.5
M26x1.5
M27x3
M27x3
M27x2
M27x2
M27x1.5
M27x1.5
M27x1
M27x1
M27x0.75
M27x0.75
M28x2
M28x2
M28x1.5
M28x1.5
M28x1
M28x1
M30x3.5
M30x3.5
M30x3
M30x3
M30x2.5
M30x2.5
M30x2
M30x2
M30x1.5
M30x1.5
M30x1
M30x1
M30x0.75
M30x0.75
M32x2
M32x2
M32x1.5
M32x1.5
M33x3.5
M33x3.5
M33x3
M33x3
M33x2
M33x2
M33x1.5
M33x1.5
M33x1
M33x1
M33x0.75
M33x0.75
M35x1.5
M35x1.5
M36x4
M36x4
M36x3
M36x3
M36x2
M36x2
M36x1.5
M36x1.5
M36x1
M36x1
M38x1.5
M38x1.5
M39x4
M39x4
M39x3
M39x3
M39x2
M39x2
M39x1.5
M39x1.5
M39x1
M39x1
M40x3
M40x3
M40x2.5
M40x2.5
M40x2
M40x2
M40x1.5
M40x1.5
M42x4.5
M42x4.5
M42x4
M42x4
M42x3
M42x3
M42x2
M42x2
M42x1.5
M42x1.5
M42x1
M42x1
M45x4.5
M45x4.5
M45x4
M45x4
M45x3
M45x3
M45x2
M45x2
M45x1.5
M45x1.5
M45x1
M45x1
M48x5
M48x5
M48x4
M48x4
M48x3
M48x3
M48x2
M48x2
M48x1.5
M48x1.5
M50x4
M50x4
M50x3
M50x3
M50x2
M50x2
M50x1.5
M50x1.5
M52x5
M52x5
M52x4
M52x4
M52x3
M52x3
M52x2
M52x2
M52x1.5
M52x1.5
M55x4
M55x4
M55x3
M55x3
M55x2
M55x2
M55x1.5
M55x1.5
M56x6.5
M56x6.5
M56x5.5
M56x5.5
M56x4
M56x4
M56x3
M56x3
M56x2
M56x2
M56x1.5
M56x1.5
M56x1
M56x1
M58x4
M58x4
M58x3
M58x3
M58x2
M58x2
M58x1.5
M58x1.5
M60x5.5
M60x5.5
M60x4
M60x4
M60x3
M60x3
M60x2
M60x2
M60x1.5
M60x1.5
M60x1
M60x1
M62x4
M62x4
M62x3
M62x3
M62x2
M62x2
M62x1.5
M62x1.5
M63x1.5
M63x1.5
M64x6
M64x6
M64x5.5
M64x5.5
M64x4
M64x4
M64x3
M64x3
M64x2
M64x2
M64x1.5
M64x1.5
M64x1
M64x1
M65x4
M65x4
M65x3
M65x3
M65x2
M65x2
M65x1.5
M65x1.5
M68x6
M68x6
M68x4
M68x4
M68x3
M68x3
M68x2
M68x2
M68x1.5
M68x1.5
M68x1
M68x1
M70x6
M70x6
M70x4
M70x4
M70x3
M70x3
M70x2
M70x2
M70x1.5
M70x1.5
M72x6
M72x6
M72x4
M72x4
M72x3
M72x3
M72x2
M72x2
M72x1.5
M72x1.5
M72x1
M72x1
M75x6
M75x6
M75x4
M75x4
M75x3
M75x3
M75x2
M75x2
M75x1.5
M75x1.5
M76x6
M76x6
M76x4
M76x4
M76x3
M76x3
M76x2
M76x2
M76x1.5
M76x1.5
M76x1
M76x1
M78x2
M78x2
M80x6
M80x6
M80x4
M80x4
M80x3
M80x3
M80x2
M80x2
M80x1.5
M80x1.5
M80x1
M80x1
M82x2
M82x2
M85x6
M85x6
M85x4
M85x4
M85x3
M85x3
M85x2
M85x2
M85x1.5
M85x1.5
M90x6
M90x6
M90x4
M90x4
M90x3
M90x3
M90x2
M90x2
M90x1.5
M90x1.5
M95x6
M95x6
M95x4
M95x4
M95x3
M95x3
M95x2
M95x2
M95x1.5
M95x1.5
M100x6
M100x6
M100x4
M100x4
M100x3
M100x3
M100x2
M100x2
M100x1.5
M100x1.5
M105x6
M105x6
M105x4
M105x4
M105x3
M105x3
M105x2
M105x2
M105x1.5
M105x1.5
M110x6
M110x6
M110x4
M110x4
M110x3
M110x3
M110x2
M110x2
M110x1.5
M110x1.5
M115x6
M115x6
M115x4
M115x4
M115x3
M115x3
M115x2
M115x2
M115x1.5
M115x1.5
M120x6
M120x6
M120x4
M120x4
M120x3
M120x3
M120x2
M120x2
M120x1.5
M120x1.5
M125x8
M125x8
M125x6
M125x6
M125x4
M125x4
M125x3
M125x3
M125x2
M125x2
M125x1.5
M125x1.5
M130x8
M130x8
M130x6
M130x6
M130x4
M130x4
M130x3
M130x3
M130x2
M130x2
M130x1.5
M130x1.5
M135x6
M135x6
M135x4
M135x4
M135x3
M135x3
M135x2
M135x2
M135x1.5
M135x1.5
M140x8
M140x8
M140x6
M140x6
M140x4
M140x4
M140x3
M140x3
M140x2
M140x2
M140x1.5
M140x1.5
M145x6
M145x6
M145x4
M145x4
M145x3
M145x3
M145x2
M145x2
M145x1.5
M145x1.5
M150x8
M150x8
M150x6
M150x6
M150x4
M150x4
M150x3
M150x3
M150x2
M150x2
M150x1.5
M150x1.5
M155x6
M155x6
M155x4
M155x4
M155x3
M155x3
M155x2
M155x2
M160x8
M160x8
M160x6
M160x6
M160x4
M160x4
M160x3
M160x3
M160x2
M160x2
M165x6
M165x6
M165x4
M165x4
M165x3
M165x3
M165x2
M165x2
M170x8
M170x8
M170x6
M170x6
M170x4
M170x4
M170x3
M170x3
M170x2
M170x2
M175x6
M175x6
M175x4
M175x4
M175x3
M175x3
M175x2
M175x2
M180x8
M180x8
M180x6
M180x6
M180x4
M180x4
M180x3
M180x3
M180x2
M180x2
M185x6
M185x6
M185x4
M185x4
M185x3
M185x3
M185x2
M185x2
M190x8
M190x8
M190x6
M190x6
M190x4
M190x4
M190x3
M190x3
M190x2
M190x2
M195x6
M195x6
M195x4
M195x4
M195x3
M195x3
M195x2
M195x2
M200x8
M200x8
M200x6
M200x6
M200x4
M200x4
M200x3
M200x3
M200x2
M200x2
M205x6
M205x6
M205x4
M205x4
M205x3
M205x3
M205x2
M205x2
M210x8
M210x8
M210x6
M210x6
M210x4
M210x4
M210x3
M210x3
M210x2
M210x2
M215x6
M215x6
M215x4
M215x4
M215x3
M215x3
M220x8
M220x8
M220x6
M220x6
M220x4
M220x4
M220x3
M220x3
M220x2
M220x2
M225x6
M225x6
M225x4
M225x4
M225x3
M225x3
M225x2
M225x2
M230x6
M230x6
M230x4
M230x4
M230x3
M230x3
M230x2
M230x2
M235x6
M235x6
M235x4
M235x4
M235x3
M235x3
M240x8
M240x8
M240x6
M240x6
M240x4
M240x4
M240x3
M240x3
M240x2
M240x2
M245x6
M245x6
M245x4
M245x4
M245x3
M245x3
M245x2
M245x2
M250x8
M250x8
M250x6
M250x6
M250x4
M250x4
M250x3
M250x3
M250x2
M250x2
M255x6
M255x6
M255x4
M255x4
M255x3
M255x3
M260x8
M260x8
M260x6
M260x6
M260x4
M260x4
M260x3
M260x3
M265x6
M265x6
M265x4
M265x4
M265x3
M265x3
M270x6
M270x6
M270x4
M270x4
M270x3
M270x3
M275x6
M275x6
M275x4
M275x4
M275x3
M275x3
M280x8
M280x8
M280x6
M280x6
M280x4
M280x4
M280x3
M280x3
M285x6
M285x6
M285x4
M285x4
M285x3
M285x3
M290x6
M290x6
M290x4
M290x4
M290x3
M290x3
M295x6
M295x6
M295x4
M295x4
M295x3
M295x3
M300x8
M300x8
M300x6
M300x6
M300x4
M300x4
M300x3
M300x3
M310x6
M310x6
M310x4
M310x4
M320x6
M320x6
M320x4
M320x4
M330x6
M330x6
M330x4
M330x4
M340x6
M340x6
M340x4
M340x4
M350x6
M350x6
M350x4
M350x4
M360x6
M360x6
M360x4
M360x4
M370x6
M370x6
M370x4
M370x4
M380x6
M380x6
M380x4
M380x4
M390x6
M390x6
M390x4
M390x4
M400x6
M400x6
M400x4
M400x4
M410x6
M410x6
M420x6
M420x6
M430x6
M430x6
M440x6
M440x6
M450x6
M450x6
M460x6
M460x6
M470x6
M470x6
M480x6
M480x6
M490x6
M490x6
M500x6
M500x6
M510x6
M510x6
M520x6
M520x6
M530x6
M530x6
M540x6
M540x6
M550x6
M550x6
M560x6
M560x6
M570x6
M570x6
M580x6
M580x6
M590x6
M590x6
M600x6
M600x6
1-64 UNC
2-56 UNC
3-48 UNC
4-40 UNC
5-40 UNC
6-32 UNC
8-32 UNC
10-24 UNC
12-24 UNC
1/4 "- 20 UNC
5/16 "- 18 UNC
3/8 "- 16 UNC
7/16 "- 14 UNC
1/2 "- 13 UNC
9/16 "- 12 UNC
5/8 "- 11 UNC
3/4 "- 10 UNC
7/8 "- 9 UNC
1 "- 8 UNC
1 1/8 "- 7 UNC
1 1/4 "- 7 UNC
1 3/8 "- 6 UNC
1 1/2 "- 6 UNC
1 3/4 "- 5 UNC
2 "- 4 1/2 UNC
2 1/4 "- 4 1/2 UNC
2 1/2 "- 4 UNC
2 3/4 "- 4 UNC
3 "- 4 UNC
3 1/4 "- 4 UNC
3 1/2 "- 4 UNC
3 3/4 "- 4 UNC
4 "- 4 UNC
0 - 80 UNF
1 - 72 UNF
2 - 64 UNF
3 - 56 UNF
4 - 48 UNF
5 - 44 UNF
6 - 40 UNF
8 - 36 UNF
10 - 32 UNF
12 - 28 UNF
1/4" - 28 UNF
5/16" - 24 UNF
3/8" - 24 UNF
7/16" - 20 UNF
1/2" - 20 UNF
9/16" - 18 UNF
5/8" - 18 UNF
3/4" - 16 UNF
7/8" - 14 UNF
1" - 12 UNF
1 1/8" - 12 UNF
1 1/4" - 12 UNF
1 3/8" - 12 UNF
1 1/2" - 12 UNF12 - 80 UNEF
1/4" - 32 UNEF
5/16" - 32 UNEF
3/8" - 32 UNEF
7/16" - 28 UNEF
1/2" - 28 UNEF
9/16" - 24 UNEF
5/8" - 24 UNEF
11/16" - 24 UNEF
3/4" - 20 UNEF
13/16" - 20 UNEF
7/8" - 20 UNEF
15/16" - 20 UNEF
1" - 20 UNEF
1 1/16" - 18 UNEF
1 1/8" - 18 UNEF
1 1/4" - 18 UNEF
1 5/16" - 18 UNEF
1 3/8" - 18 UNEF
1 7/16" - 18 UNEF
1 1/2" - 18 UNEF
1 9/16" - 18 UNEF
1 5/8" - 18 UNEF
1 11/16" - 18 UNEF
Thread Oil filter (Engine Oil Filter),ต๊าปไร้เศษผลิตไส้กรองน้ำมันเครื่อง,ต๊าปรีดเกลียวผลิตไส้กรองน้ำมัน,rolltap,Formingtap,FlutelessTap
M20X1.5-6H INT
M16X1.5-6H INT
1"-14 UNS-2B
1 1/4"-12UNS-2B
M85X2.0-7H INT
1 1/2"-16UN-2B
M16X1.5-6G EXT
M22X1.5-6G INT
1 1/4"-11 1/2NPT
1/2"-20UNF-2B
3/4"-16UNF-2A
1/8"-27NPT-2A
13/16"-16UNS-2B
15/16"-16UN-2B
7/8"-14UNF-2B
1"-12UNF-2B
1 1/8"12UNF-2A
M72X2.0-7H INT
M24X1.5-6H INT
3/8"24UN-2B
1 1/16"16UN-2B
M14X1.5-6H INT
13/16"-18UNS-2B
11/16"-16UN-2B
7/8"-14UNS-2B
13/16"-12UNS-2B
11/16"-16UN-2B
M18X1.5-6H INT
13/16"-12UNS-2B
M32X1.5-6H INT
M30X1.5-6H INT
2 1/4"-12UNS-2B
1/2"-14NPTF
M22X1.5-6G INT
3/8"-18NPTF
M16X1.5-6G EXT
3/4"NPT14
1"-11 1/2NPT
1 1/4"-11 1/2NPT
M85X2.0-7H INT
Thread Size Filter
15/16"-16UN-2B
1 1/2"-16UNF
1 3/8"-12UNF
1"-14UNS-2B
1 1/8"-16UN-2B
1 1/4"-12UNF-2B
Tap Valve (Internal thread & External Thread) GAS Thailand
Thread Forming Taps Roll Taps YAMAWA TANOI Roll form taps
Inlet : 3/4" - 14NGT
Outlet : 0.885 - 14 NGO - LH - INT
Inlet : 3/4" - 14NGT
Outlet : 1.312 - 5 ACME - 2G - RH - EXT, 0.885 - 14 UNS - LH - INT
Inlet : W 28.8 - 14 DIN 477
Outlet : 5/8" - 14 BSPF - LH - INT
Inlet : 3/4" - 14NGT
Outlet : 7/16 - 20 UNF
Inlet : 3/4" - 14NGT
Outlet : 1.312 - 5 ACME - 2G - RH - EXT, 0.885 - 14 UNS - LH - INT
Inlet : W 19.3 - 14
Outlet : W 21.8 - 14 - LH - EXT
Inlet : W 28.8 - 14 DIN 477
Outlet : W 21.8 - 14 - LH - EXT
Inlet : W 28.8 - 14 DIN 477
Outlet : W 20 - 14 - LH - EXT
Inlet : M 25.5 X 2
Outlet : W 20 - 14 - LH - EXT
Inlet : W 19.3 - 14
Outlet : W 21.8 - 14 - LH - EXT
Inlet : W 19.8 - 14 DIN 477
Outlet : W 21.8 - 14 - LH - EXT
1/2" - 14NGT
Inlet : M22 X 1.25
Outlet : M 16 x 1.5
Inlet : 0.715 - 14
Outlet : 3/8" - 19BSPF - LH
Inlet : M 16 x 1.5
Outlet : M 12 x 0.75
Tr 8× 1.5
Tr 9× 2 Tr 9× 1.5 Tr 10× 2 Tr 10× 1.5
Tr 11× 3 Tr 11× 2 Tr 12× 3 Tr 12× 2 Tr 14× 3 Tr 14× 2 Tr 16× 4 Tr 16× 2 Tr 18× 4 Tr 18× 2 Tr 20× 4 Tr 20× 2
M, MF, EG M, EG MF, G, Rp, Rc/PT, Pg, MJ, W cyl, Tr, W tap, BSW, BSF, BA, NPT, NPTF, UNC, UNF, UNEF, UN, EG UNC(STI), EG UNF(STI), UNJC, UNJF, & NPSM PG gland thread sizes
1/8-27 NGT ¼-18 NGT 3/8-18 NGT ½-14 NGT ¾-14 NGT $ ¾-14 NGT (Cl)–1* ¾-14 NGT (Cl)–2* ¾-14 NGT (Cl)–3* ¾-14 NGT (Cl)–4* 1-11.5 NGT 1.1/2-11.5 NGT
Car Oil filter Motor oil Motor vehicle Thread• Tapping drill sizes for taps in a multilingual format for thread types: M, MF, EG M, EG MF, G, Rp,
Rc/PT, Pg, MJ, W cyl, Tr, W tap, BSW, BSF, BA, NPT, NPTF, UNC, UNF, UNEF, UN, EG UNC(STI), EG
UNF(STI), UNJC, UNJF, & NPSM,Rd Thread DIN• METRIC THREAD -- COARSE PITCH -- M
• METRIC THREAD -- FINE PITCH -- M (1 mm - 28 mm)
• METRIC THREAD -- FINE PITCH -- M (30 mm - 64 mm)
• METRIC THREAD -- FINE PITCH -- M (65 mm - 100 mm)
• PIPE THREAD -- BRITISH STANDARD PIPE PARALLEL -- BSPP/BSPF
• PIPE THREAD -- JAPANESE PIPE PARALLEL -- PF (see BSPP/BSPF chart)
• PIPE THREAD -- BRITISH STANDARD PIPE TAPER -- BSPT
• PIPE THREAD -- JAPANESE PIPE TAPER -- PT (see BSPT chart)
• PIPE THREAD -- METRIC TAPER PIPE -- MT
• BRITISH THREAD -- COARSE PITCH -- BSW
• BRITISH THREAD -- FINE PITCH -- BSF
• BRITISH THREAD -- MINIATURE SERIES -- BA
• METRIC THREAD -- COARSE PITCH -- MINIATURE SERIES -- BS 4827 -- S
• METRIC 80 degree Pg form THREAD -- ELECTRICAL THREAD -- Pg
• METRIC 60 degree M form THREAD -- ELECTRICAL THREAD -- M
• METRIC THREAD -- Aerospace threads MJ
• METRIC 30 degree Tr form THREAD -- TRAPEZOIDAL THREAD (~Acme) -- Tr
• METRIC BUTTRESS COARSE THREAD -- DIN 513
• METRIC KNUCKLE THREAD -- DIN 405
• METRIC KNUCKLE THREAD -- DIN 20400
• METRIC SCREW THREAD INSERT THREADS - for HELICAL WIRE INSERTS -- Eg M
• BRITISH ET -- ELECTRICAL THREAD -- (Conduit to BS 31)
• BRITISH STANDARD CYCLE -- BSC
• BRITISH STANDARD BRASS -- BSB
• BRITISH WHITWORTH -- GAS CYLINDER THREAD -- DIN 477
• TIRE VALVE SCREW THREAD -- DIN 7756
• BICYCLE SCREW THREAD -- DIN 79012
• CYCLE ENGINEER INSTITUTION THREAD -- CEI
• IMPERIAL WIRE GAUGE – IWG spoke thread data
• USA THREAD -- UNIFIED COARSE -- UNC
• USA THREAD -- UNIFIED FINE -- UNF
• USA THREAD -- UNIFIED EXTRA FINE -- UNEF
• USA THREAD -- NATIONAL PIPE TAPERED THREAD -- NPT Tapping Chuck Collet Drilling
Knuckle Thread DIN 405 RD thread
Düz kanallı kılavuz
ดอกต๊าปเกลียวซ้าย ดอกต๊าปเกลียวสั่งทำ ดอกต๊าปเกลียวท่อ เกลียวมิล เกลียวนิ้ว
เกลียวหุน เกลียวอังกฤษ เกลียวอเมริกา เกลียวคางหมู เกลียวแม่แรง #ดอกต๊าปเกลียวพิเศษ
CROSS REFERENCE
CHART
Metric Cable
Grip Size Tap Size Metric Tapped
Hole Size Inch Tapped
Hole Size Closest American
Drill Size Metric
Through-Hole Inch
Through-Hole
M 12 M 12x1.5 10.5 mm 0.413 z(.413) 12.2mm 0.480
M 16 M 16x1.5 14.5mm 0.571 37/64"(.578) 16.2mm 0.638
M 20 M 20x1.5 18.5mm 0.728 47/64"(.734) 20.2mm 0.795
M 25 M 25x1.5 23.5mm 0.925 59/64"*(.922) 25.2mm 0.992
M 32 M 32x1.5 30.5mm 1.2 - 32.2mm 1.268
M 40 M 40x1.5 38.5mm 1.516 - 40.2mm 1.583
If you are going to use a polyamide grip with a nut and are not going to tap the hole, you will need to drill a larger hole to push the grip through. Use the chart below for the correct size hole.
DRILL HOLE
AND TAP INFORMATION
Cable Grip
Size Rose PG Tap
Part Number Metric Tapped
Hole Size Inch Tapped
Hole Size Closest American
Drill Size Metric
Through-Hole Inch
Through-Hole
PG 7 08070000 11.5mm 0.453 29/64" ( .453) 12.3mm 0.484
PG 9 08090000 14mm 0.551 35/64" ( .547) 15.1mm 0.594
PG 11 08110000 17.25mm 0.679 46/63"( .672) 19.6mm 0.772
PG 13.5 08130000 19mm 0.748 3/4"( .750) 20.2mm 0.795
PG 16 08160000 21.25mm 0.837 53/64"( .828) 22.3mm 0.878
PG 21 08210000 27mm 1.063 1 1/16"(1.063) 28.2mm 1.11
PG 29 08290000 35.5mm 1.398 1 25/64"(1.391) 36.9mm 1.453
PG 36 08360000 45.5mm 1.791 1 51/64"(1.797) 48.8mm 1.921
PG 42 08420000 52.8mm 2.079 2 5/64"(2.078) - -
PG 48 08480000 58mm 2.283 2 9/32"(2.281) -
-
CABLE GRIP
SELECTION GUIDE
Wire Size Metric Size PG Size American Size
mm Inches
3-6.5 .12-.26 M12 PG7 -
4-8 .18-.32 M16 PG 9 3/8" NPT
6-10 .24-.39 M16 PG 11 -
6-12 .24-.47 M20 - -
7-12 .28-.47 - PG13.5 1/2" NPT
10-14 .39-.55 M20 PG16
-ดอกต๊าปเกลียวพิเศษ,Custom-Made Tap,เกลียวซ้าย,Taps YAMAWA,Nachi,OSG, TANOI, ISCAR, Kyocera, MITSUBISHI, HITACHI, TOSHIBA, Nachi, Yamawa OSG, TANOI, ISCAR, Kyocera, MITSUBISHI, HITACHI, TOSHIBA, Nachi, Yamawa
EMUGE-FRANKEN,JBO,KGS,YG1,tanoi yamawa zeus dixi
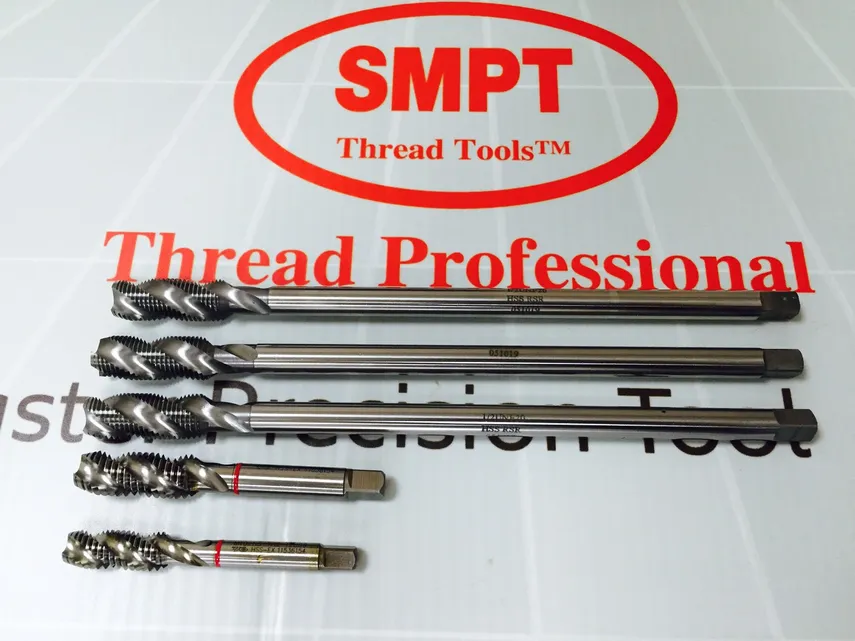
Application: long reduced shank to allow nuts to run over
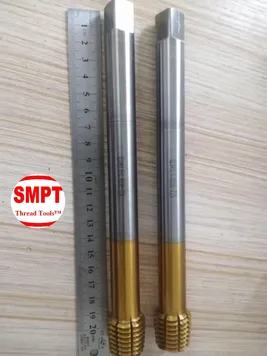
Mainly used for tapping nuts. The threaded length and extended shank portion are designed for good workability with nuts, allowing continuous machining until the shank portion is completely filled with stacked up nuts.Nut taps are designed to thread nuts in small lot sizes or used because of the long entering chamfer
13-18 .51-.71 - PG21 3/4" NPT
14-18 .55-.71 M25 - -
20-25 .79-.98 M32 PG29 1" NPT
24-32 .95-1.26 M40 PG36 -
32-38 1.26-1.50 M50 PG42 -
37-44 1.46-1.73 M63 PG48 -
Torneiras manuais, torneiras em espiral, torneiras em espiral
Kılavuz çekme takımları dört tipe ayrılır: Düz kanallı kılavuz, spiral uçlu kılavuz, spiral fitil kılavuz ve biçim verme kılavuzu. Diş açılacak deliğin kör delik mi boydan boya delik mi olduğuna ve parça malzemesine göre hangi tipin kullanılacağı belirlenir.
Düz kanallı kılavuz
Spiral uçlu kılavuz
Spiral uçlu kılavuz
Spiral fitil kılavuz
Spiral fitil kılavuz
Biçim verme kılavuzu
Biçim verme kılavuzu
Метчик ручной, метчик спиральный, метчик спиральный
カスタマイズされたスクリュータップ:オーダーメイド
Customized screw taps: made to order
定制丝锥:定做
စိတ်ကြိုက်ဝက်အူဘုံ: အမိန့်လုပ်လေ၏
हाथ नल, सर्पिल नल, सर्पिल नल tap
Tarauds à vis personnalisés: fabriqués sur commande
Vòi vít tùy chỉnh, được làm theo đơn đặt hàng
Ketuk skru disesuaikan: dibuat mengikut pesanan
Keran sekrup khusus: dibuat sesuai pesanan
صنابير لولبية مخصصة: حسب الطلب
HC+SP
HC - SP
HC+SP OX
HC- SP OX
AL+SP
AL - SP
AL-SP 1.5P
LO-SP
LS-LO-SP
ZET-B
ZEN-B
PM-SP
LS-PM-SP
F_SP
LS-F-SP
HFIHS
HFISP
VUSP
VUSP 1.5P
HVSP
MHSP
SP
SP 1.5P
+SP
ISP
SP OX
SP LH
AU+SP
LS-SP
LS-SP OX
LS-SP LH
LS-SP V
VUPO
PO
+PO
IPO
PO OX
PO LH
PO V
LS-PO
LS-PO V
LS-PO-K
SU+PO
SU-PO
LS-SU-S-PO
S-PO
HC+PO
HC - PO
HC-PO OX
EH-PO
ZEN-P
Pitch≦0.6mm (40TPI)
Size:M1-M24 :
15µm tolerance. The tolerance of P1, P2, P3,P4,P5…
is defined as (P1 =basic +10~+25µm), (P2=(+25~+40µm), (P3=+40~+55µm)
Pitch >0.6mm Pitch≦1.75mm
Size: M1-M24
20µm tolerance.
The tolerance of P1, P2, P3 ...,P5
is defined as basic (P1=+0~+20µm), (P2=+20~+40µm), (P3=+40~+60µm)
Pitch≦0.6mm
Size:M1-M24
: 15µm tolerance. OH1, OH2, OH3,OH4,OH5,OH6
is defined as (OH1 =basic +10~+25µm), (OH2=(+25~+40µm), (OH3=+40~+55µm),(OH4=+55~+70µm),
: 20µm tolerance. tolerance. OH1, OH2,OH3,OH4,OH5,OH6
is defined as basic
(OH1=+0~+20µm), (OH2=+20~+40µm), (OH3=+40~+60µm) , (OH4=+60~+80µm)CONDUIT THREAD;Pg DIMENSIONS #pg
PG7
PG9
PG11
PG13.5
PG16
PG19
PG21
PG25
PG29
PG36
PG42
PG48
PG63
CONDUIT THREAD;Pg DIMENSIONS #pg
เกลียวPG (Germany PG Thread) คือมาตราฐานเกลียวของทางประเทศเยอรมัน สามารถแบ่งตามขนาดเกลียวได้ดังนี้ : PG7, PG9, PG11, PG13.5, PG16, PG21, PG29, PG36, PG42, PG48, PG63
Cable Gland เคเบิ้ลHEYGO thread tap standard: ISO529, DIN 371, DIN376, DIN374, DIN352, JIS, ANSI, GOS……
Type: Straight Flute, Spiral Flute, Spiral Point, and Forming thread taps.
Material: HSS, HSS-CO, HSS-E, HSS-PM, etc.
Coating: Balzers TiN, TiALN, TiCN coating
Workpiece: Suitable for steel, stainless steel, cast iron, aluminum, and hardened steel.
Both standard and custom products are available
Z-PRO Spiral Fluted Taps, Coated
Z-PRO Spiral Fluted Taps, Coated 1.5P
ZPRO Spiral futed taps for forged parts in the heavy metalworking industry
Z-PRO Spiral Taps for Medium Hard Carbon Steels
Spiral Fluted Taps
Spiral Fluted Taps 1.5P
Plus Series Spiral Fluted Taps
Spiral Fluted Taps for General Purpose
Spiral Fluted Taps, Oxidized
Spiral Fluted Taps for Left Hand Threads
Plus Series Spiral Fluted Taps, Optimum Coating for the tapping
Long Shank Spiral Fluted Taps
Long shank oxidized spiral tap
Long Shank Spiral Fluted Taps for Left Hand Threads
ดอกต๊าปเกลียวซ้าย yamawa ดอกต๊าปเกลียว คืออุปกรณ์ที่ใช้ในการสร้างเกลียวให้กับชิ้นงาน ดอกต๊าปเกลียวตัวเมีย ดอกต๊าปเกลียว4หุน ดอกต๊าปเกลียวยี่ห้อไหนดี ดอกต๊าปเกลียวขนาดใหญ่
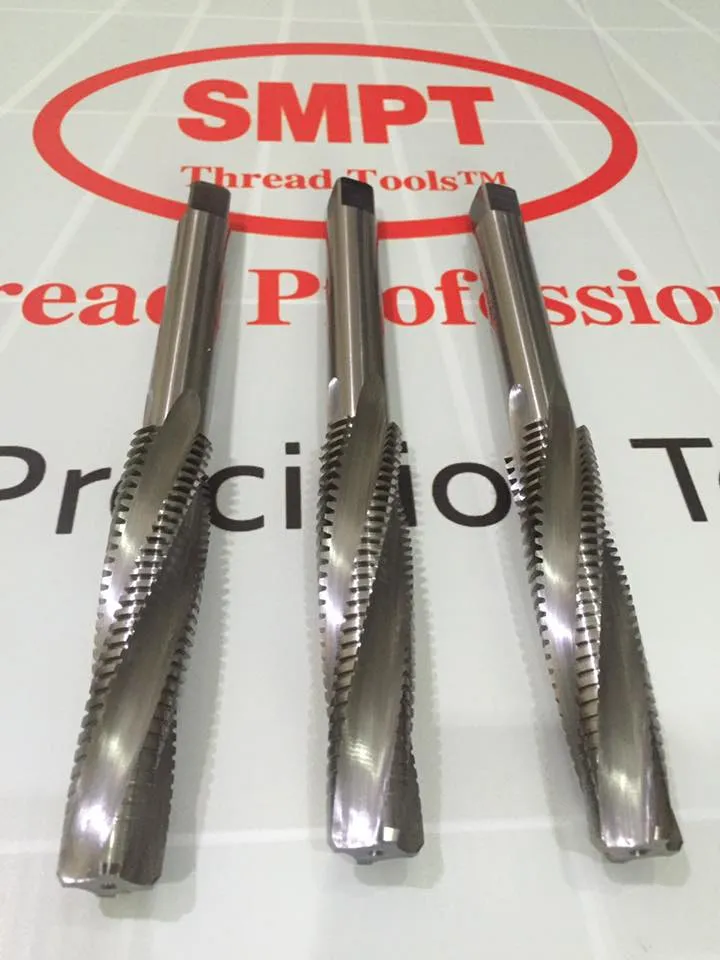
ดอกต๊าปเกลียวเลื้อย OSG OSG General Purpose Tapดอกต๊าป ไฮสปีดสตีล HSSE เกลียวเลื้อย OSG EX-SFT เหมาะสำหรับการต๊าปเหล็กเหนียวทั่วไปEX-SFTHSSE
1/8-27 NGT ¼-18 NGT 3/8-18 NGT ½-14 NGT ¾-14 NGT $ ¾-14 NGT (Cl)–1* ¾-14 NGT (Cl)–2* ¾-14 NGT (Cl)–3* ¾-14 NGT (Cl)–4* 1-11.5 NGT 1.1/2-11.5 NGT
The 7 Benefits of Form TappingChip-less Tapping: since threads are formed and not cut, there are no chips to interfere with the tapping process or cause chip-removal problems in blind holes. Making threads without chips produces excellent thread surface quality, eliminates the risk of poor threads due to axial “mis-cutting”, increases static and dynamic strength of threads and allows elevated tapping speeds.
Stronger Threads: the grain flow of formed threads follows the contour of the thread, resulting in greater thread strength. This is especially true for materials that work-harden such as steel and stainless steel.
Better Thread Gaging: forming taps rearrange the metal in the hole to create the thread. Because no metal is cut away, the possibility of producing oversized threads is greatly reduced.
Stronger Taps: the absence of chips eliminates the need for flutes, resulting in a solid, stronger tap. Since the metal’s structure is cold worked along the thread profile, the threads produced are generally stronger and have a smooth, burnished surface finish.
Longer Tap Life: forming taps can last 3 to 20 times longer than cutting taps because they have no cutting edge to dull.
More Efficient Production: longer tap life, less tap breakage, and faster tapping speeds combine to reduce cycle time and machine downtime. Form taps can be operated at higher speeds and feeds than conventional taps.
Ideal for Non-Lead Screw Tappers: the ability to form their own lead makes Form taps especially well suited for machines without lead screws.What is a Thread Tap?
Thread taps are tools specifically for cutting the female portion of a pair of mating metal fasteners. The masculine sections are cut with a die, on the other hand. Dice are used to cutting bolts, while taps are used to cut nuts. Taps can also create threads in a hole, making it easier for a bolt to fit through.
Threading and tapping have different purposes. Screw threads are created by both threading and tapping. But tapping creates internal threads, whereas threading creates outward lines. There are numerous varieties of thread taps, including power taps, spiral point taps, plug taps, and hand taps. These are only a few of the multiple thread taps available. These can be operated manually using a tap handle or a wrench, as well as mechanical drilling equipment.
A machine is constructed from many tiny components that are connected. The most common tools are nuts, bolts, and various screws. High-speed steel, even alloy steel, high-carbon steel, etc., are all used to make taps. These have been tempered and toughened. They resemble headless bolts with complete threads in form. Four flutes are formed on the whole part, which has cables, and the upper portion is generally square.
A screw mechanism uses a tap to create newer threads or clear out (chase) old ones. A tapping set could be in the toolbox of an automotive technician, even though machinists and engineers are the ones that use this equipment the most frequently. There are numerous instances where a thorough understanding of the science involved in tapping threads into a piece of equipment can save hours of frustrating work and a lot of money in replacement parts.
Parts of a Thread Tap:
Body: This is usually the part where the threads are cut and is considered the central part.
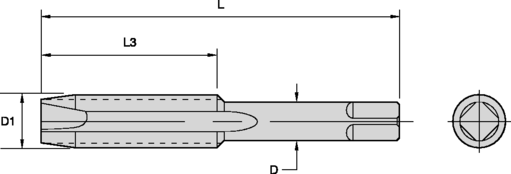
Shank: The shank is the smooth portion above the body where the threads are cut. It is circular and has markings indicating the thread pitch the shank will cut.
Tang: The tang refers to the area above the shank. It has a square shape, and turning it around requires gripping it with a tap handle.
Land: The land is where the threads are cut or the space between the flutes.
Flutes: The grooves made on the area between two lands on the tap are flutes. These are constructed as a length, top to Bottom. These flutes deliver lubricant within and expel the metal shavings created during cutting threads.
Heel: The heel refers to the diagonal area behind the threads cut into the ground.
Cutting Face: The cutting face is the surface of the cutting tool that the material is pushed against.
Types of Thread Taps:
There is a total of 10 types of Thread Taps; they are mentioned as follows:
1. Hand tap: These taps are utilized as a set. Three fixtures are included in this set:
Taper Tap:This involves rubbing and chamfering the lower side of 8 to 10 threads. These work as threading devices and are simple to install in drill holes. This tap’s lower end is the same size as the tap-size drill.
Intermediate Tap:Another name for it is a second tap. On the lower side of this tap, taper up to 3 to 5 threads is produced. It gives threads created by the taper tap the correct depth and form. Only these two taps are utilized if threads must be cut through drill holes.
Bottom or Finishing Tap:The third tap in the set is the Bottom, also called Finishing Tap. It is employed in locations where the hole does not run the length of the project after the taps, as mentioned above, have been used. Additionally, it is employed for threads that have been cut through the drill to be cleaned and finished. At a taper’s end, one or a half threads are cut.
Plug Tap:A plug tap’s cutting edges taper less noticeably. This results in a steady cutting action for the plug tap that is more aggressive than a taper tap but less harsh than a bottoming tap. Before the maximum cutting diameter is engaged, the plug tap typically has 3 to 5 tapered threads. Plug taps are excellent for use with through holes since they start almost as quickly as taper taps but provide a broader range of threads.
2. Power Taps: This thread tap is ideal if one needs it for hand-matching labor or CNC applications. Since the tips mentioned above require manual operation, they are commonly known as hand taps. The machinist frequently needs to reverse a hand tap to shatter the chip (also regarded as a swarf) that accumulates during cutting. By doing this, the sliced material is kept from crowding the tap and breaking it. The most prevalent power-driven tap is a “spiral point” plug tap, sometimes known as a “gun” tap, whose cutting edges are obliquely offset from the tap centerline.
This feature prevents congestion by repeatedly breaking the chip and ejecting it into the hole in front of it. To allow the chips to escape, spiral point taps are typically employed in holes that penetrate the entire material.
The spiral flute tap is an alternative to the spiral point plug tap, and it has flutes that resemble twist drill flutes. The ability of spiral flute taps to function well in blind holes makes them a common choice for high-speed, automatic tapping operations.
3. Gas Tap: It is used to fit at locations where almost any liquid or gas goes through pipes and to cut gas-type threads. This sort of tap has some taper in the body length and 1/12 threads chamfered at the lower section. The taper is 1/4 per foot. Gas does not spill because of this.
4. Spiral Tap: To allow the chips to escape, spiral point taps are typically employed in holes that penetrate the entire material. The spiral flute tap is an alternative to the spiral point plug tap, and it has flutes that resemble twist drill flutes. The ability of spiral flute taps to function well in blind holes makes them a common choice for high-speed, automatic tapping operations.
Similar to hand taps, spiral point taps are available with a taper tap, which has a tapered end, or a plug tap, which has significantly less taper and is designed for blind holes.
The other two are usually preferred, although they are less expensive than the other two. The main drawback of these is that they advance the chips into the hole before the tap-down, to put it another way. For blind spots, this is a horrible idea, but it’s not a significant deal for through holes.
5. Spiral Fluted Tap: These thread taps possess relief grooves and a spiral cut. They are widespread and resemble the majority of hand touches anyone may encounter. However, the front cutting edges’ spiral angles aid in chip ejection, and the angled edge also provides better cutting performance. Due to their lower cost and ability to operate at somewhat higher rates than hand taps, they are the thread tap one should consider employing for power tapping.
Similar to hand taps, spiral point taps could be purchased with a plug tap (designed for blind holes) or a taper tap, which has a tapered end. Its unique feature is that the flutes in this tap are spirally carved rather than straight. These taps are not trapped in the slot’s edges since they are spiral flutes. Two or even three threads are chamfered on its edge.
6. Interrupted Thread Tap: There is just one tooth for each different thread on these thread taps. The goal is to offer better chip extraction. Every other tooth is removed, which aids chip breaking and creates more space for lubricant to enter and perform its function and more area for the chip to exit.
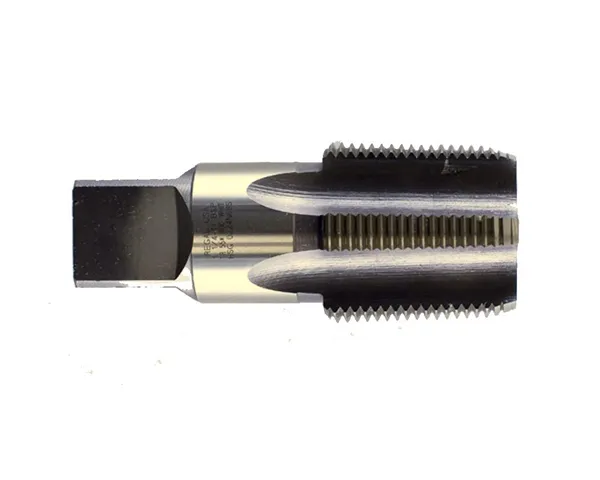
7. Pipe Taps: The thread taps used to tap pipe threads are known as pipe taps. Depending on whether the pipe thread is supposed to be straight or tapered, there are both short and pointed pipe taps available. A common NPT Thread Pipe Tap is seen in the picture. The NPT thread profile’s taper is visible.
Since a tapered hole cannot be drilled, taps for tapered pipe threads must work harder. At the top of the hole, they have a lot more material to remove than at the Bottom. It is recommended to taper the hole with a pipe taper reamer to reduce the strain on the tap.
8. Forming Tap: A forming tap is a very unusual kind of tap. When turned into the hole, a forming tap, also known as a flueless tap or roll tap, merely forces the metal into a thread shape rather than cutting it from the edges of the hole as cutting taps do. A forming fixture is like a plain thread or a cutting tap, even without flutes.
As the tap is inserted into a hole of the correct size, lobes that are periodically spaced around it form the thread. The cables behind the lobes are somewhat recessed to lessen friction during contact.
There is no need to regularly back out the tap to clear away chips because the fixture does not produce chips, which can block and damage a cutting tap. Because of the chip buildup in the hole, tapping blind holes with a cutting tap is more complex and better suited for thread formation. Forming taps are only adequate on pliable materials like aluminum or mild steel.
Usually, formed threads are more durable than cut threads. It is essential to remember that the tap drill size is different from the size used for a cutting tap, as given in most tap drill tables and that a precise hole size is necessary because a hole that is just a little bit too small will break the tap. Due to the frictional forces involved, proper lubrication is essential; consequently, lubricating oil rather than cutting fat is employed.
9. Extension Tap: These thread taps are similar to standard hand taps, except they have much longer shanks. It is used to cut threads in deep locations, like oil cups or the hub of a pulley.
10. Flute-less Tap: In soft metals such as brass, copper, aluminum, etc., this tap is employed to cut threads similar to the thread rolling method. No material is sliced by it. This tap stands out because it lacks flutes and instead cuts threads throughout the whole length of its body.
Some other types of taps include
Master Tap: This tap is almost identical to the hand tap, except it has more cutting faces because it consists of 6 to 10 flutes. The thread is precise and neat with this tap. Threads are only cut with this tap in inspection equipment like thread ring gauges.
Machine Tap: With the aid of a tap drill machine, these thread taps are utilized to cut threads. They are used while being held in a unique holder. To make it simple to remove the fixture from the task, the drill machine must have reverse speed.
Machine Screw Tap: Machine Screw Taps are taps used to create threads in holes less than 14 in diameter. The lower side has two or four chamfered threads.
Bend Shank Tap: When there is no suitable area for moving the handle with hands, this sort of tap is employed with a handle. This tap’s long, curved shank is bent at the top.
Stay Bolt Tap: This tap’s lower plain section, whose diameter matches that of the job’s hole, aids in maintaining the tap’s straightness.
What is the Size of a Tap?
The tap hole should be the correct size; therefore, before driving the tap to cut the inside threads of the work, the drill is used to bore the gap to the right size. The tap’s core diameter should match the size of the routine.
The threads wouldn’t be the correct depth if the drill were more giant. There would be trouble cutting threads and a chance the tap might break if the exercise were more minor. Therefore, the movement must be the correct size. A tap-size drill is a drill of that size. It is calculated using the formula shown below:
Size of tap X 7/8 – 1/32= size of the exercise.
What are the types of Tap Handles?
With a tap, it is possible to manually cut threads in work by moving the tap handle into the hole. There are three varieties of tap handles, solid, adjustable, and “T” Type handles.
Solid and Adjustable Tap Handle: The fixed handles on the solid tap handle are manufactured from solid material on both sides for convenience. Two distinct rectangular grooves are carved from across the tap in the middle of the rectangle. These may move fixtures of two different sizes. A moveable tap, a pair of two pieces kept in place by the adjusting screw, and taps of various sizes can all be moved.
“T” Type Handle: A chuck with three fitting jaws. This chuck holds various little taps of multiple types. On the upper side of its shank, a hole is drilled, through which a rod is inserted, allowing the fixture that is fastened to the rod to be easily adjusted.
What is the procedure for cutting Threads with Taps?
One should start by boring a tap hole that is the proper size for the tap. It is essential to ensure that the fixture can be chamfered or filed. The next step is securely holding the task in a vice, etc. Then, to begin with, cut threads with a taper tap.
One should verify that the tap is moving straight through the try square after moving two or three threads. Moving the fixture in the motion forward and backward should be done when tapping. While tapping, utilization of adequate lubrication should be there. One should move the intermediate, and finishing taps must come after moving the taper tap. At last, to remove the metal shavings while cutting threads in a blind hole, a fixture should be removed in between.
What are the Precautions to be taken while cutting Threads with Taps?
Before tapping, a hole of the proper size must be drilled.
Before utilizing the tap, it should be carefully cleaned.
Use the tap handle as directed by the tap.
Maintain equal hand pressure on both ends of the tap handle.
To avoid jolts, the tap should be stroked forward and bbackward
The tap needs to be kept secure and cleaned appropriately.
How to Use a Tap?
The initial step is to determine The Threads per inch. The threads are sliced into a hole when one taps. A cylinder’s threads are cut using a die set (bolt). Determine the threads per inch (TPI) of the component to be fixed before using a tap or a die. The TPI of a bolt or nut can be determined by using a gauge system with various pins. After deciding its TPI, one should also pick the die that fits the bolt’s TPI. Which side to start using will be determined by a tapered die. The unique wrench that holds and controls the die is designed to fit the die.
Then it is essential to make new threads. One should put the worn-out bolt into a vice to retain it while the wrench is turned over to use the die to create new threads. Put some cutting oil on the bolt to lubricate it since cutting metal with metal might generate heat.
Hold the die horizontally and place it over the bolt. A wrench is turned. The bolt’s already-cut threads will cause the die to catch. Reverse the twist every few revolutions to clear the threads and improve the dice cutting. Additionally, keep applying cutting oil as one goes. The bolt must pass the top of the die before the user may turn the wrench.
Then one is to make a bolt out of a steel rod. Using a die set, any ordinary steel rod can also be transformed into a bolt. The rod’s end must be beveled for this to work. If necessary, use a grinder to chamfer a rod’s back to create an angle. A flat-ended rod will not function properly with the die. When cutting through a worn bolt, lubricate the rod frequently. Make slow turns. To get the desired results from this approach, exercise a little patience.
The last step includes using a tap. The user should Pick the right size tap for the bolt or hole one wishes to thread before using it. The tap should be inserted into the unique wrench and tightened. Then comes the positioning of the fixture’s cutting end over the hole and turn. To keep the tap lubricated, use cutting oil. Once the tap is turned on, periodically turn it slightly backward, just like anyone would with the die.
Bitec
Special Size
SMPT Thread Tools
ต๊าปคาร์ไบด์
ดอกต๊าปเกลียว NGT
Special Taps
HT,SFT,POT Tap
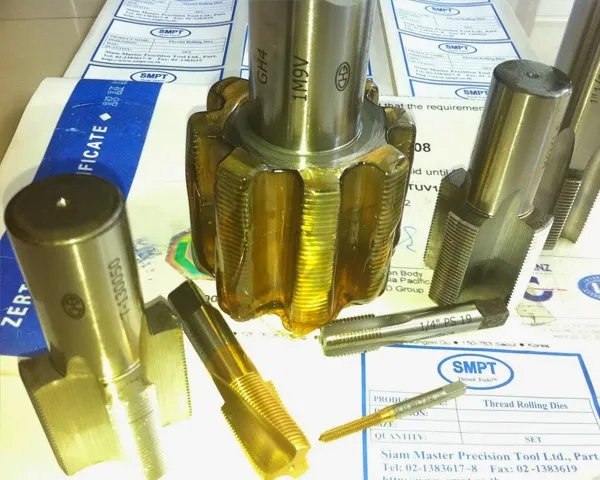
Made to Order
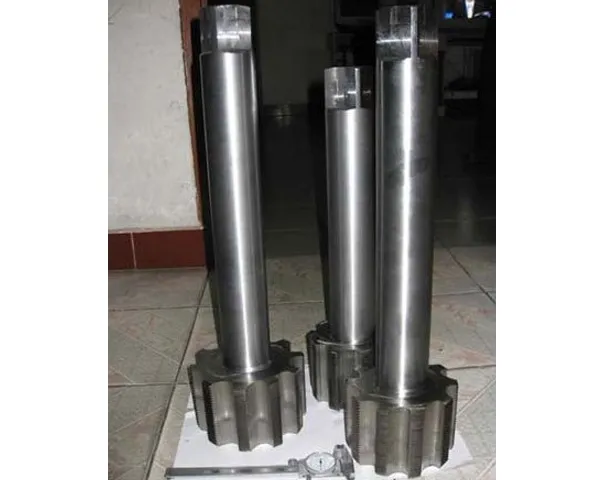
Big Tap
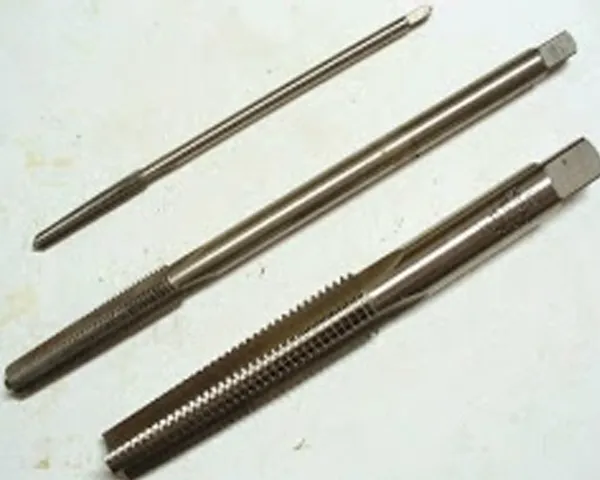
Long Shank Taps
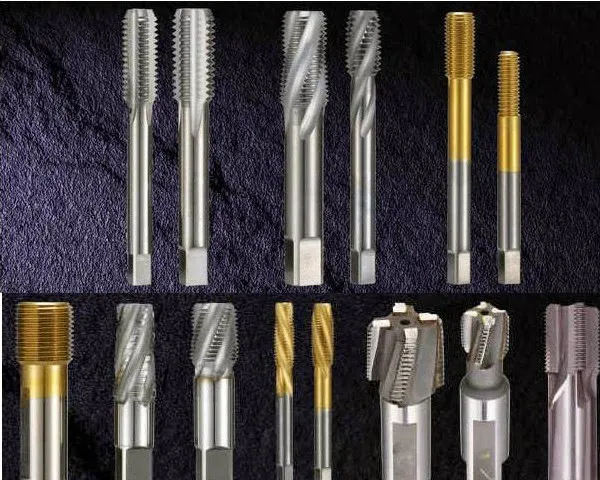
Carbide Taps
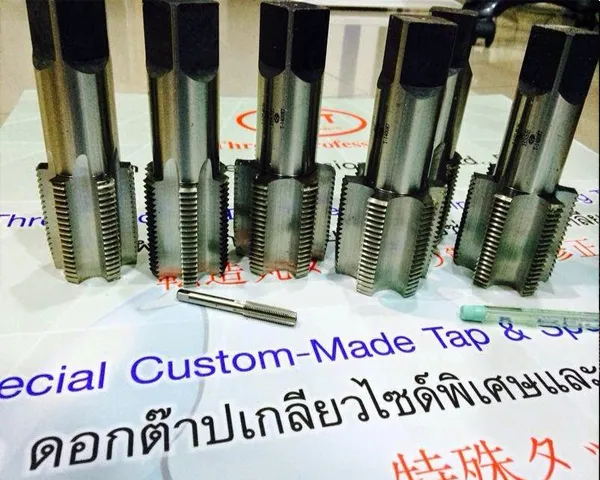
Big Taps
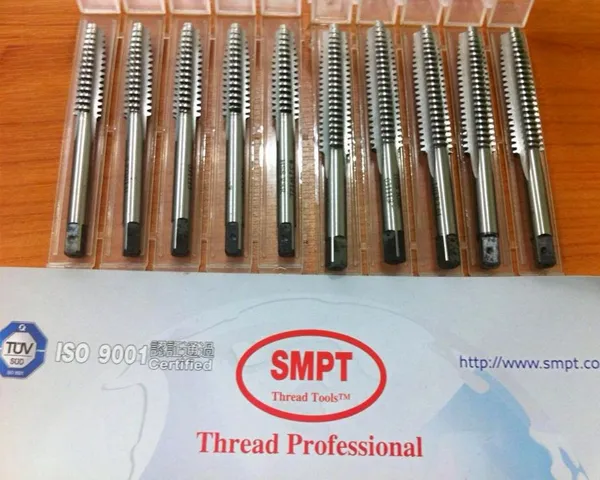
ACME TAP
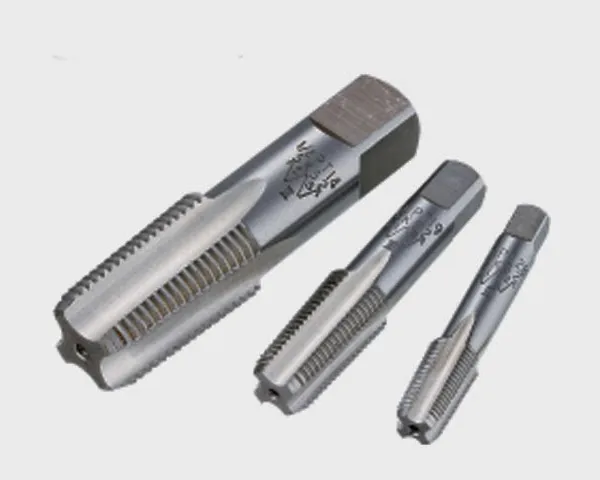
Pipe Tap
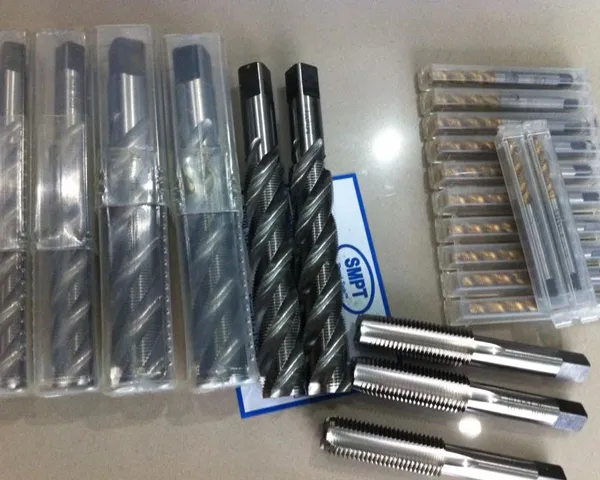
Taps
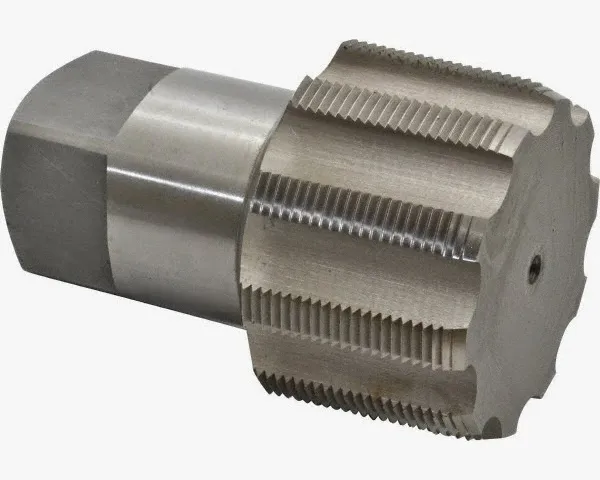
Pipe tap
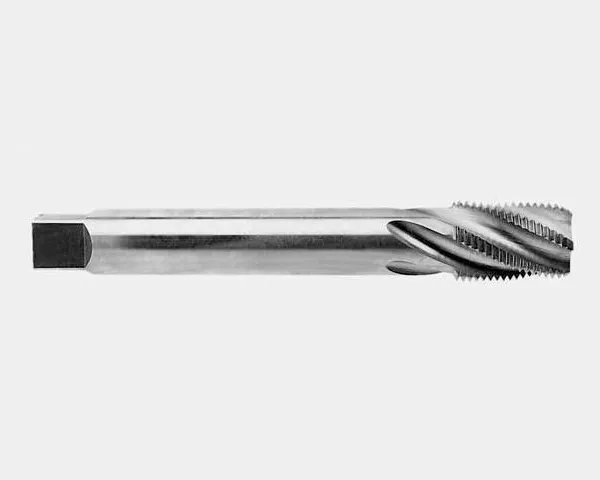
ต๊าปขนาดพิเศษ สั่งทำ
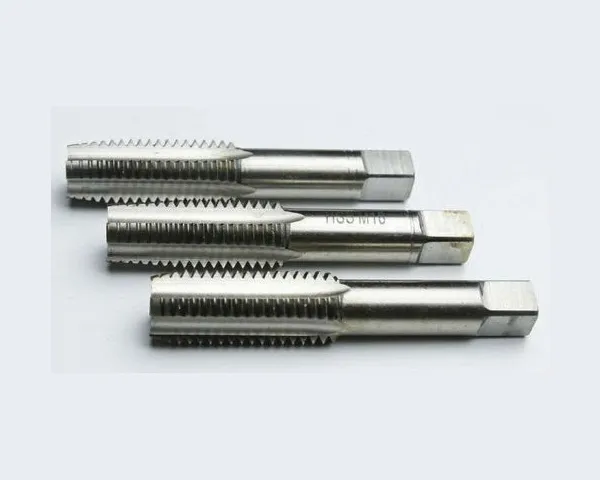
Hand Tap (SET)
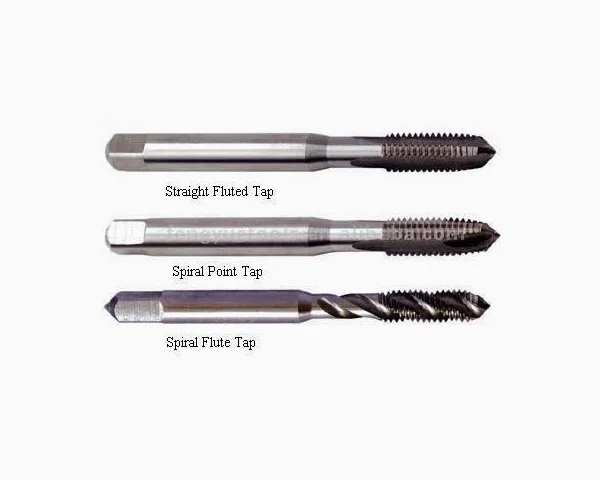
Tap Type
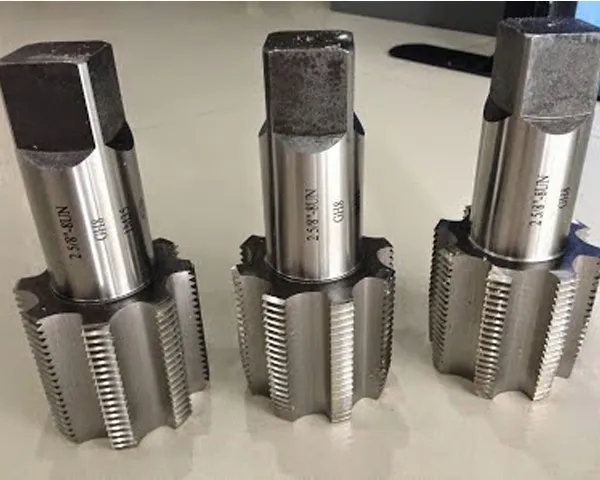
ดอกต๊าปเกลียวพิเศษ สั่งทำ
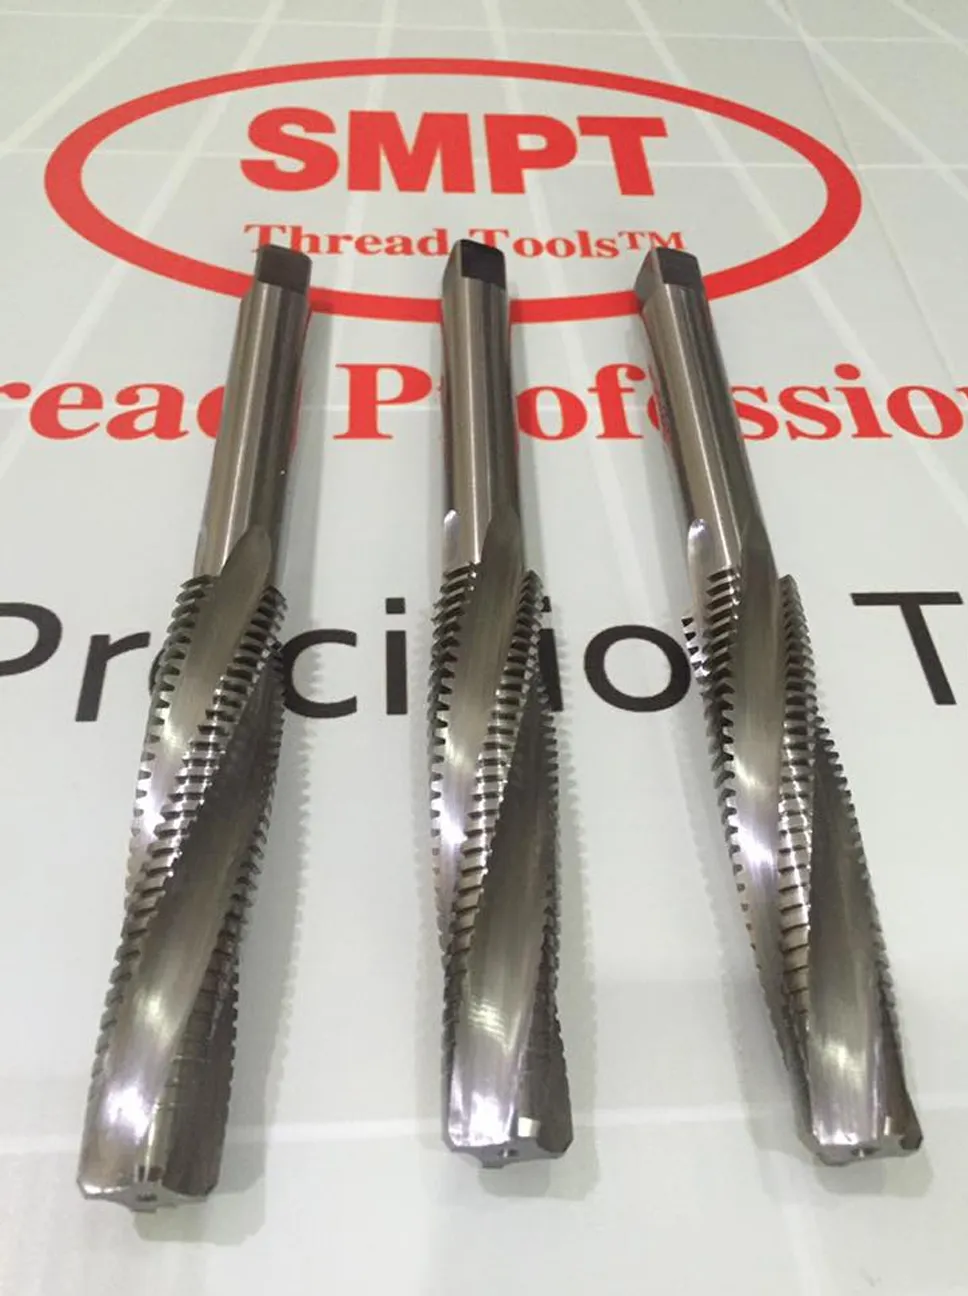
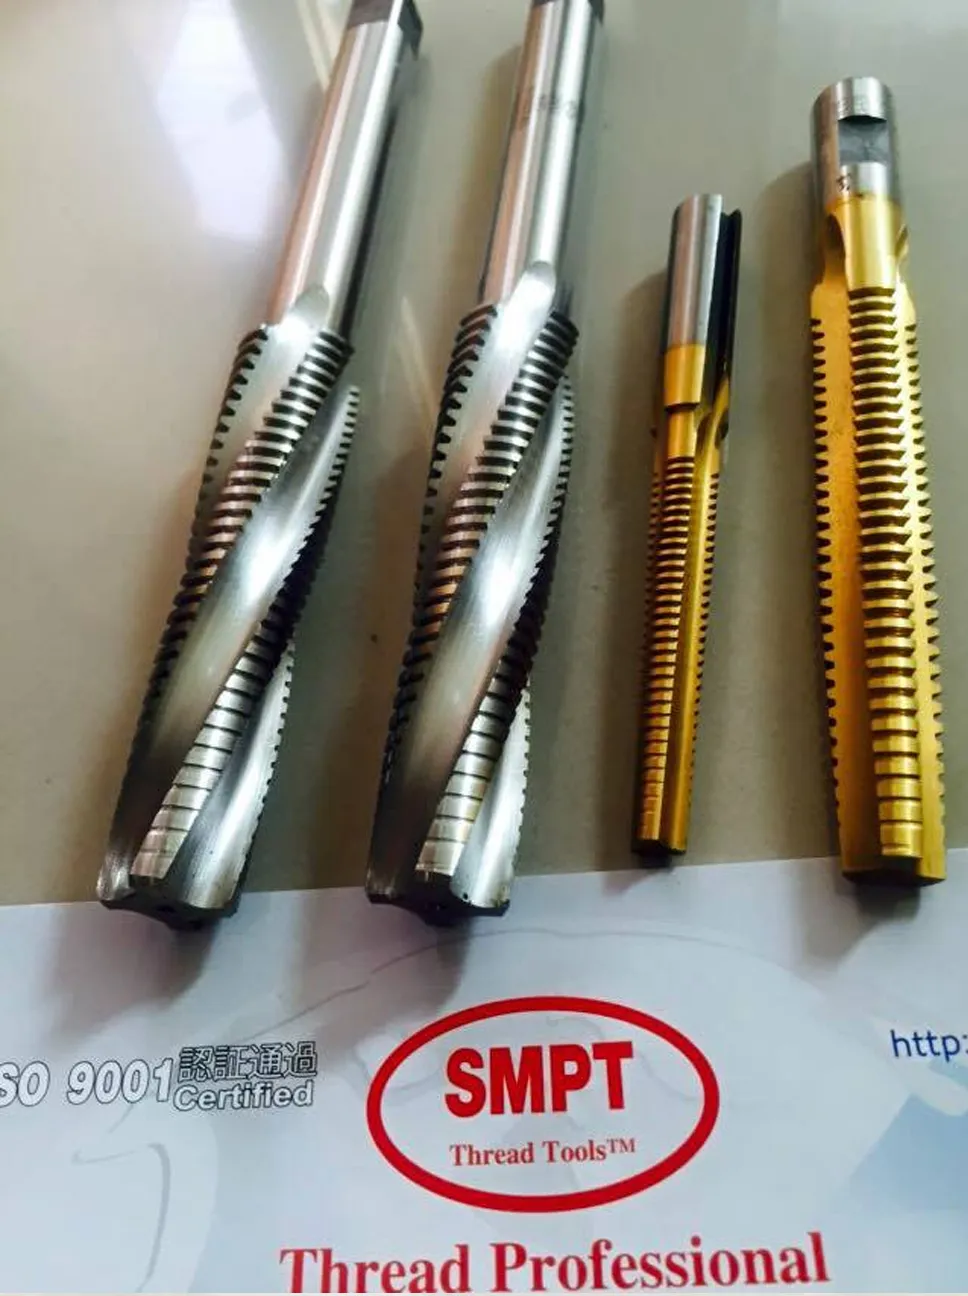
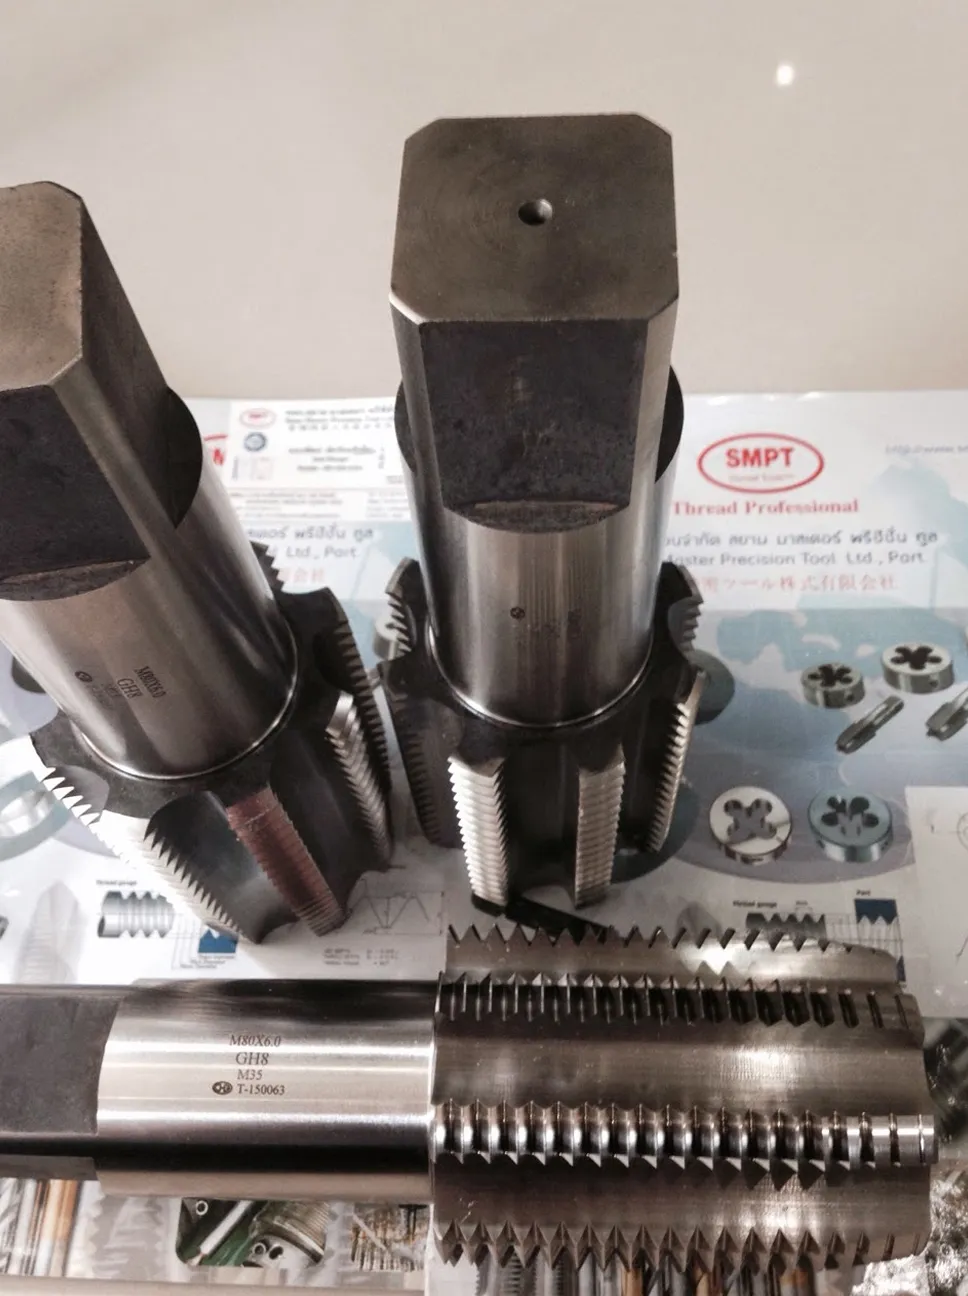
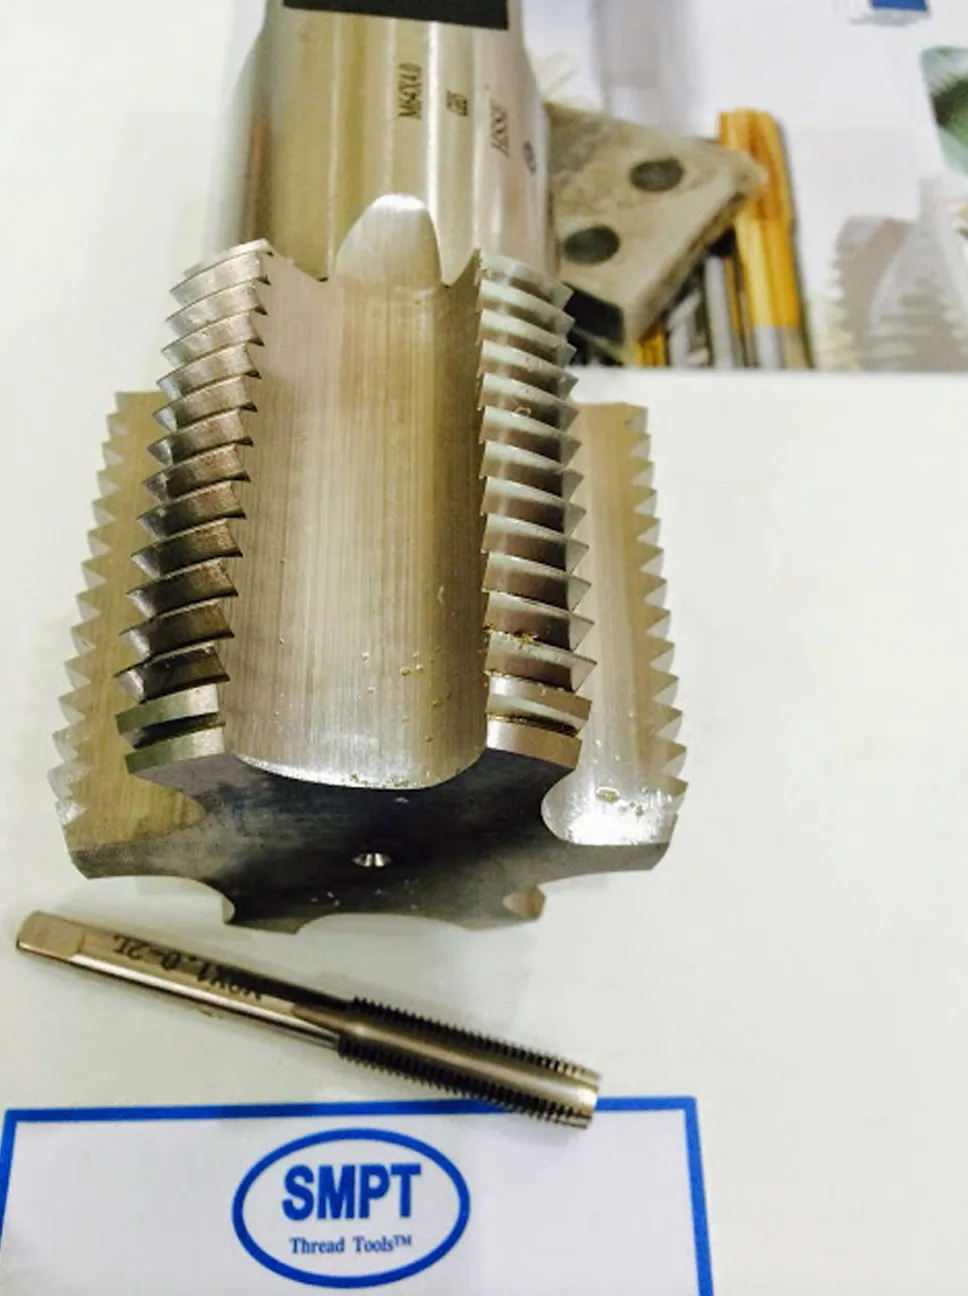
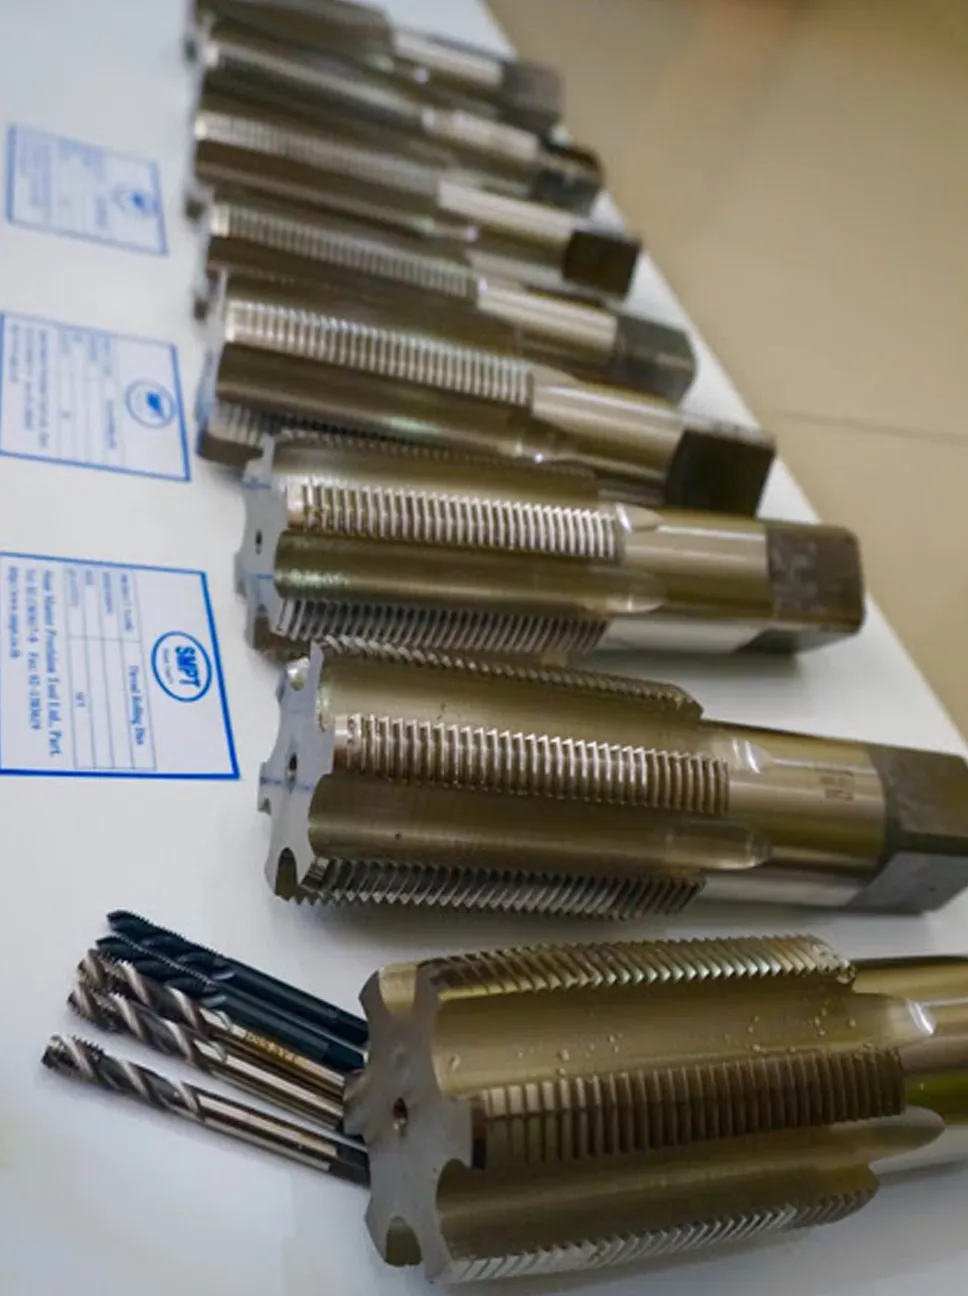
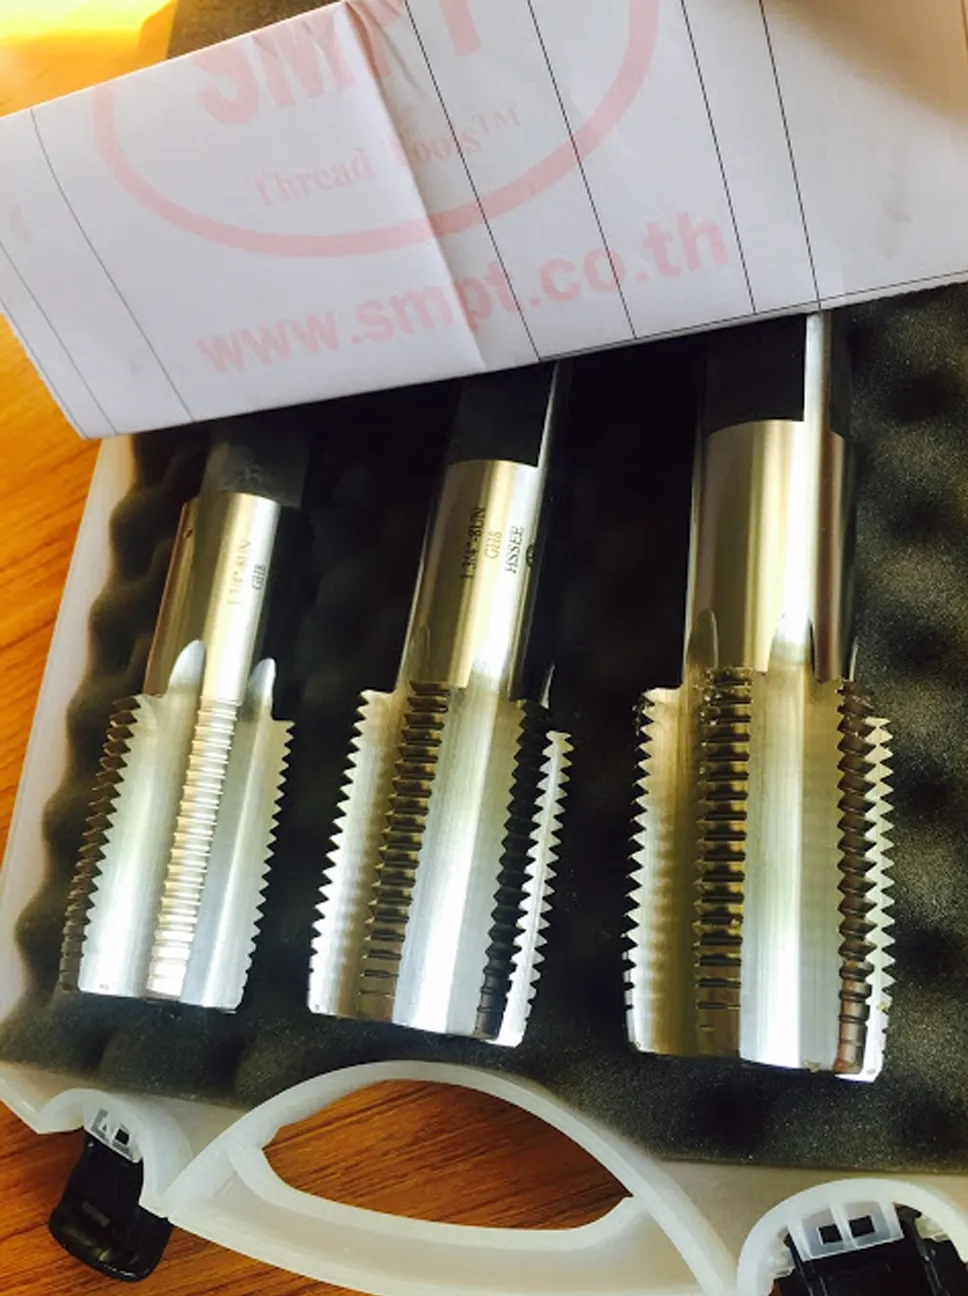
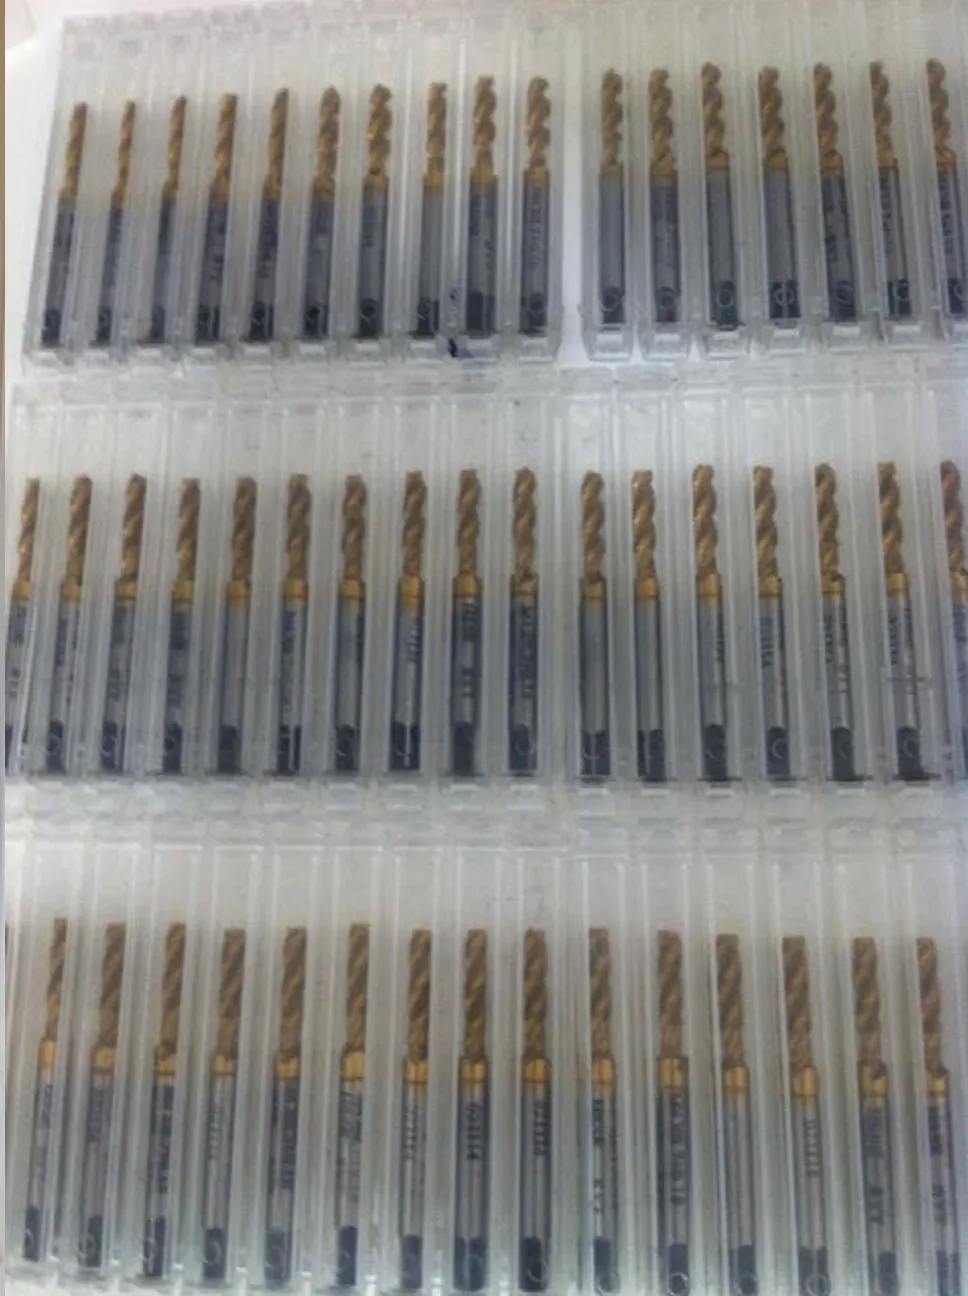
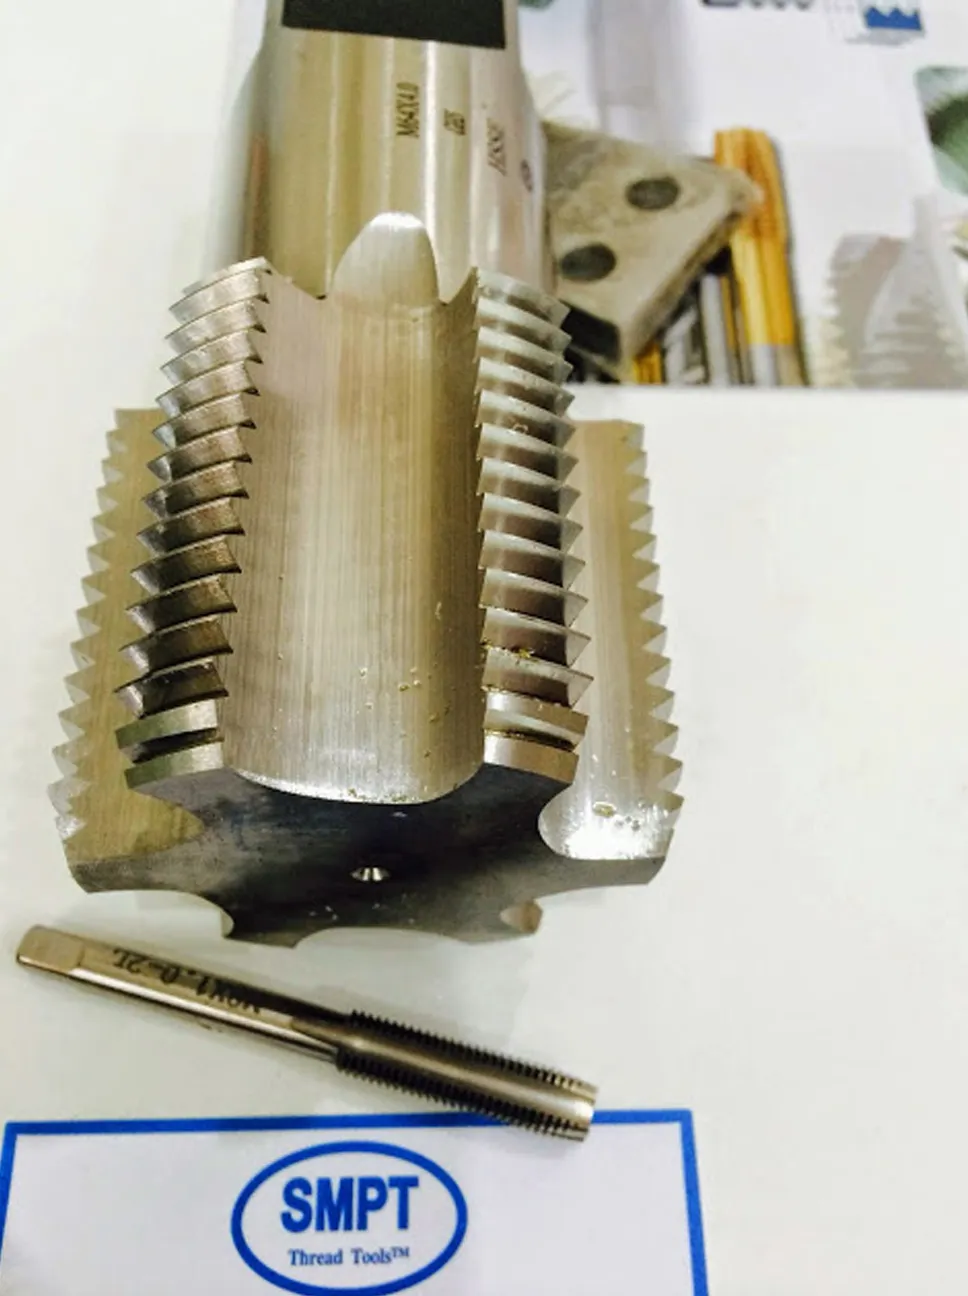
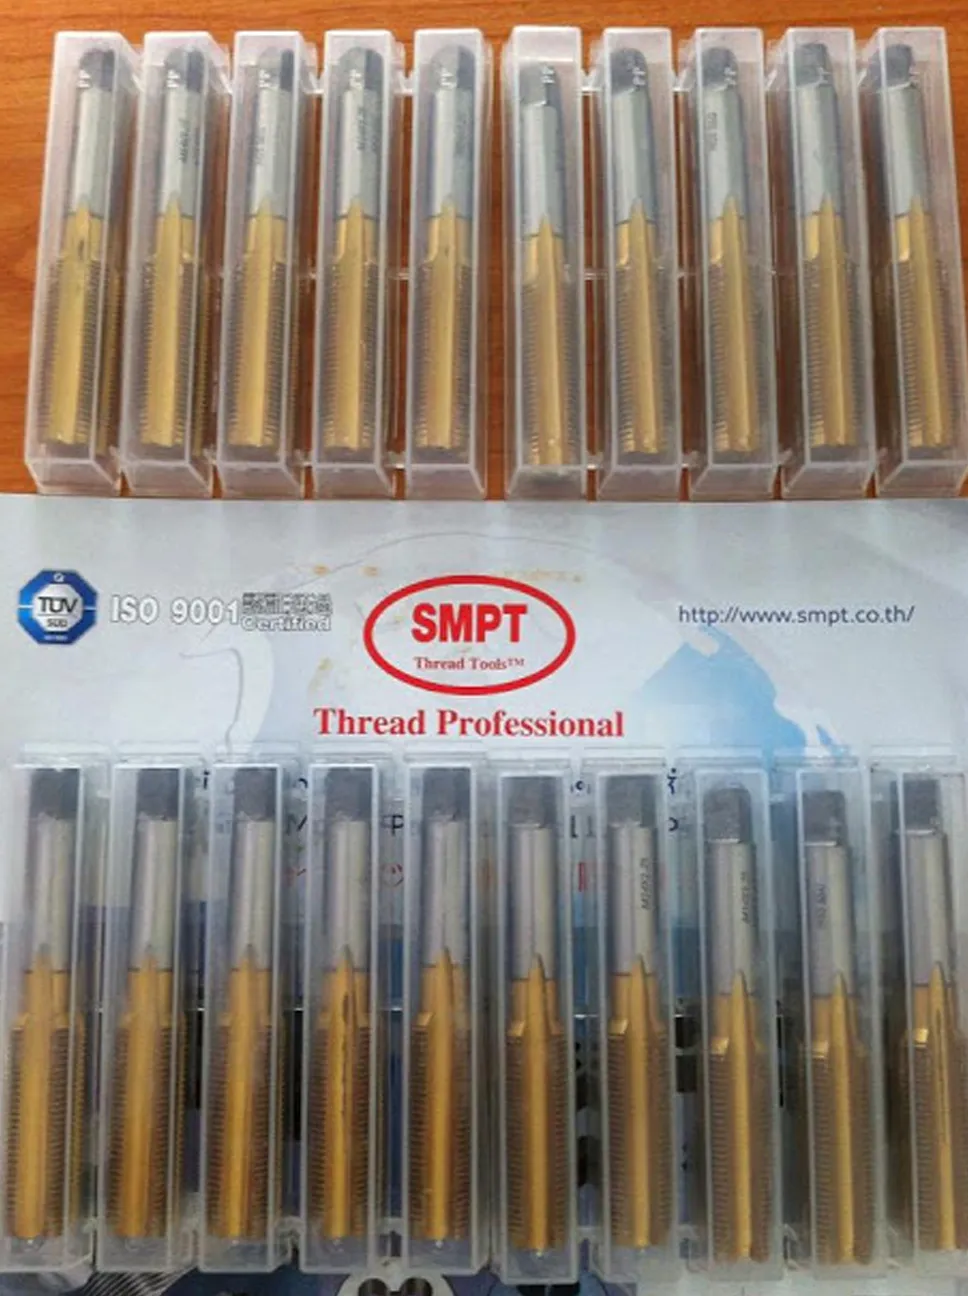
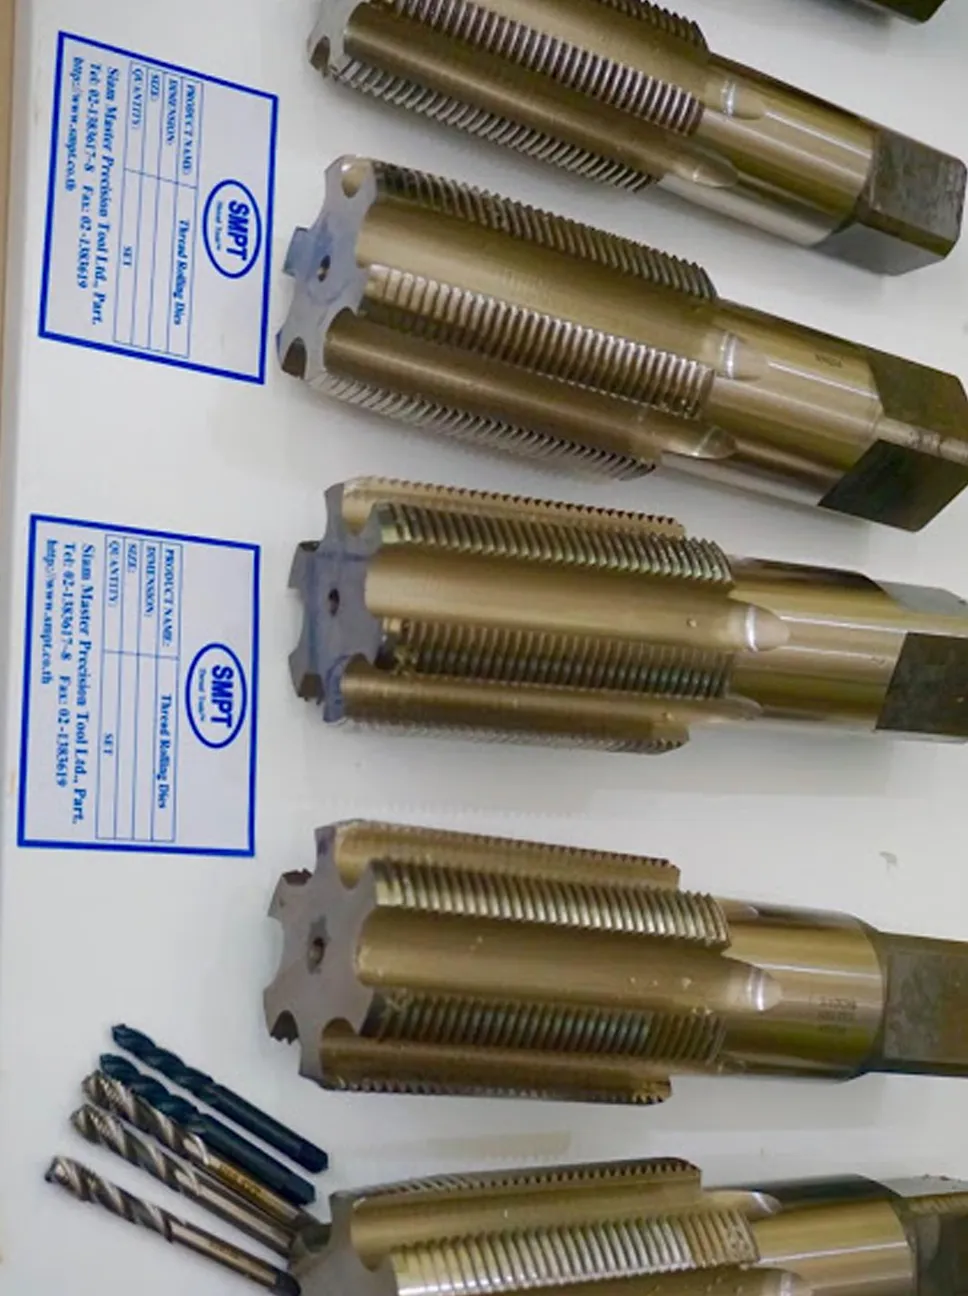
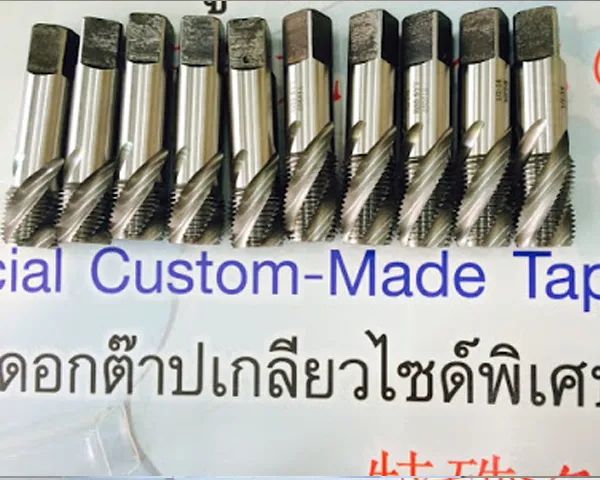
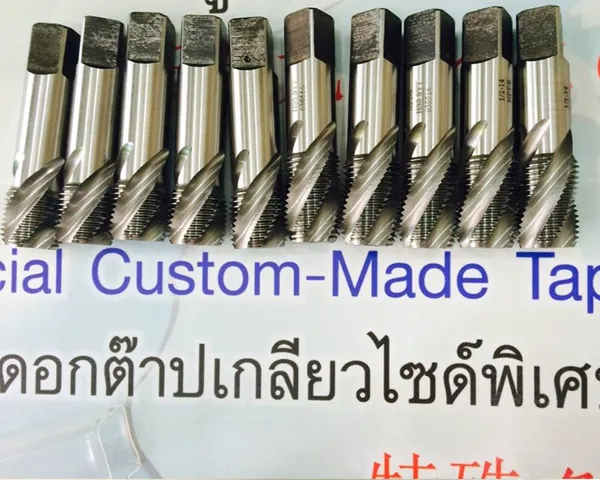
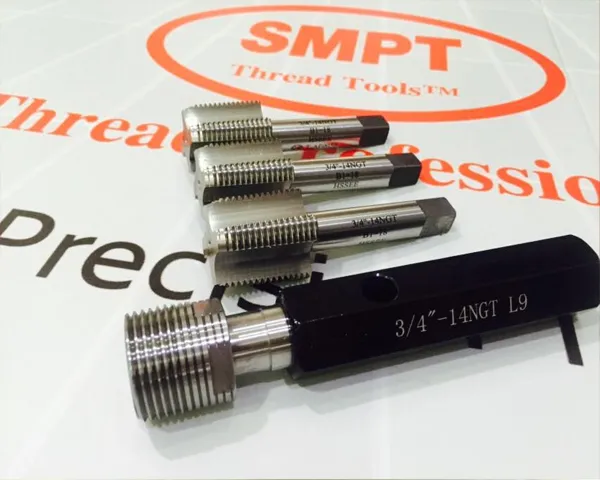
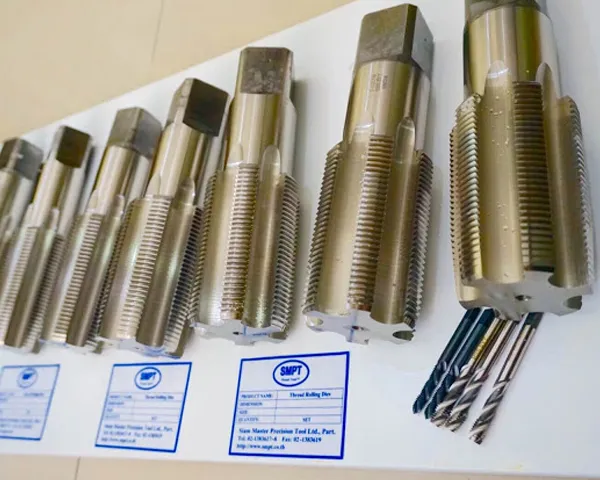
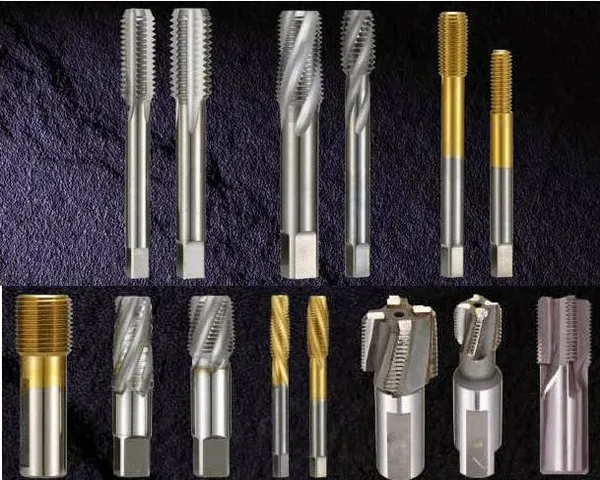
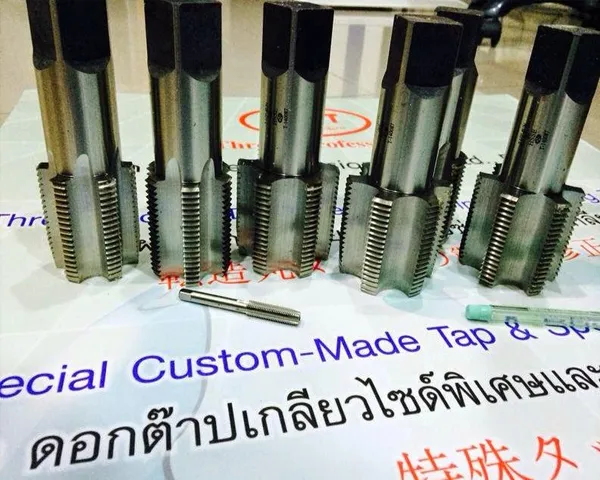
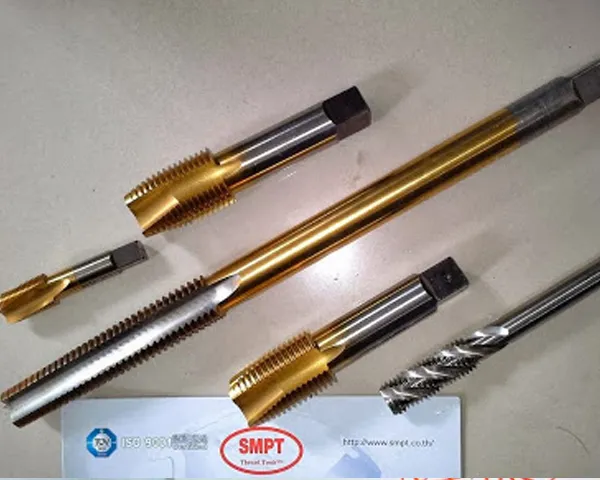
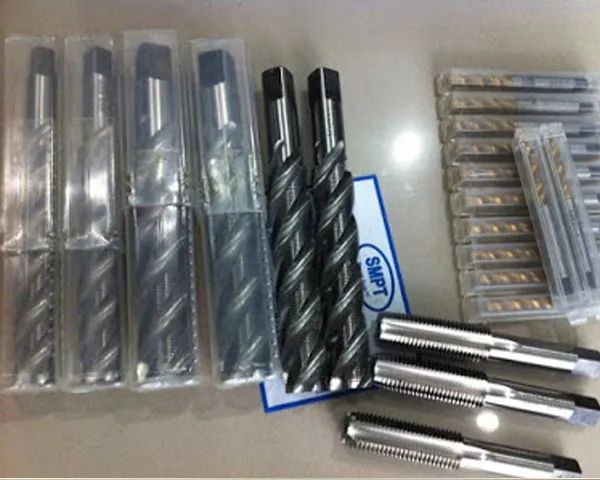
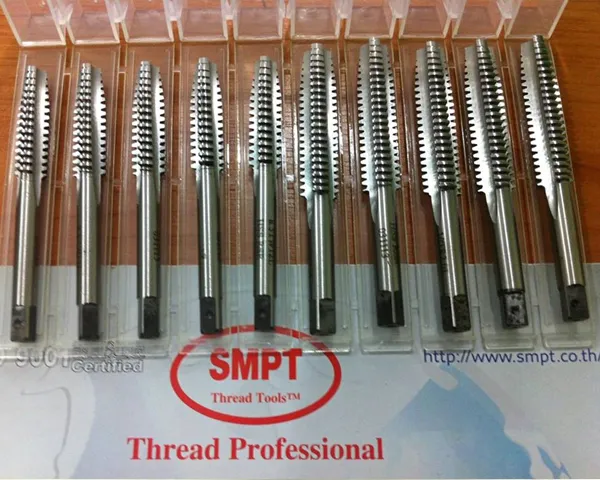
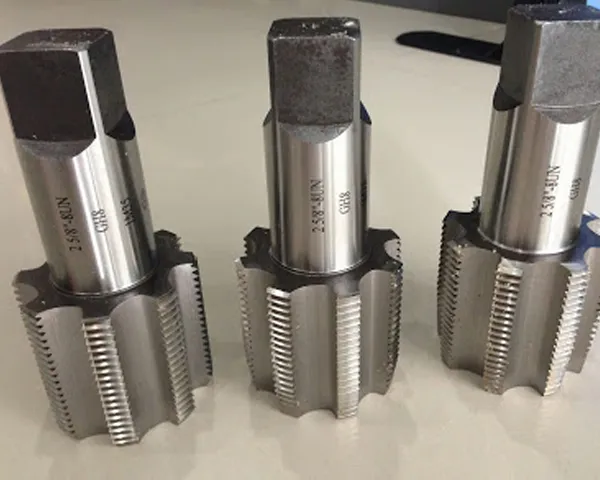
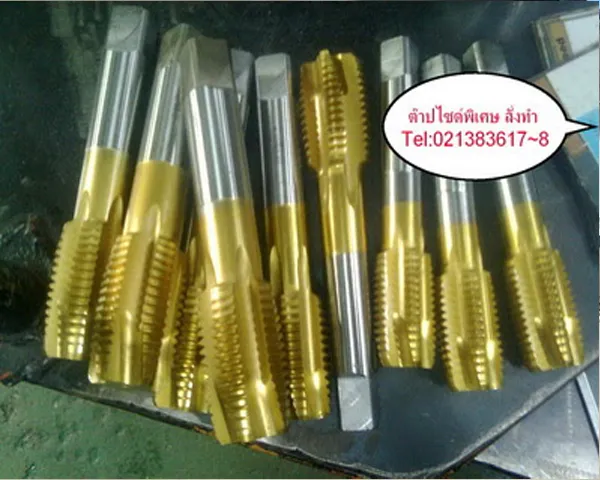
Point Tap
TiN
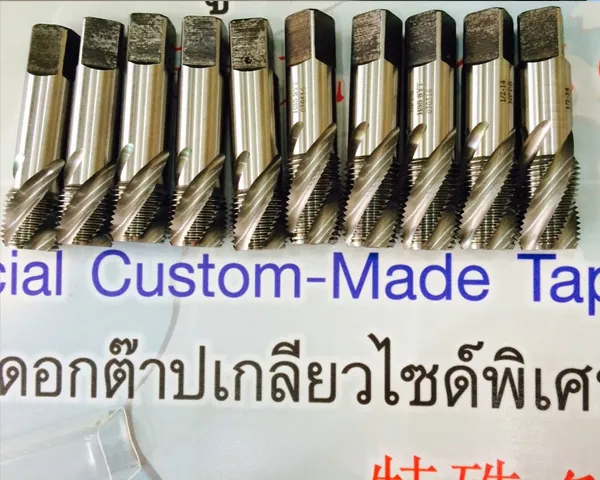
Spiral Flute Taps
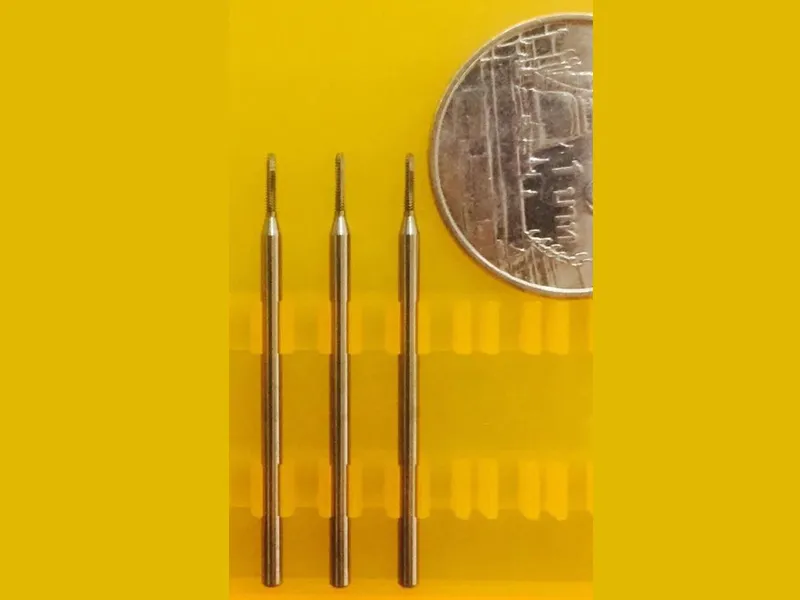
Micro Tap
Small Tap Less than <1mm Carbide
kundenspezifische Spezialgewindebohrer
特殊スパイラルタップ、オーダーメイド、逆スパイラル、大スパイラル、異形スパイラル、左ねじれタップ 市販されていないもの、特殊ねじ(図面またはサンプルをご用意ください) 材質:超硬、HSSe、AISI M42、JIS SKH59 DIN 1.3343、SKH-9
タップ、スパイラルタップ ドリルねじタップ スパイラルタップ、ハンドタップ、ソリッド用タップ、ハンドタップ、マシンタップ、ハイスピークタップ、3タップ、タップセット、マシンタップ、HSSタップ。 左ねじタップ、手タップ、マシンタップ、マシンタップ、ねじタップ、真鍮ジョイント 真鍮ねじ込み継手 めねじ、おねじ、インチねじ、斜めテーパねじ 真鍮継手タップ用ねじタップ 真鍮継手タップ
주문 제작된 특수 스파이럴 탭, 오버사이드 스파이럴, 대형 스파이럴, 이상한 스파이럴, 왼손 스파이럴 탭 시중에서 구할 수 없는 특수 나사산(도면이나 샘플만 있음) 재질 : Carbide , HSSe, AISI M42, JIS SKH59 DIN 1.3343, SKH-9
탭, 스파이럴 탭 드릴 나사 탭 스파이럴 탭, 핸드 탭, 솔리드 탭용 탭, 핸드 탭, 머신 탭, 하이스피크 탭, 3 탭, 탭 세트, 머신 탭, 탭 HSS. 왼나사 탭, 핸드 탭, 기계 탭, 기계 탭, 나사 탭, 황동 조인트 황동 나사 피팅 암나사, 수나사, 인치 나사, 비스듬한 테이퍼 나사 황동 조인트 태핑용 나사 탭 황동 피팅 탭
حنفية لولبية خاصة ، مصنوعة حسب الطلب ، لولبية كبيرة ، لولبية كبيرة ، لولبية غريبة ، حنفية لولبية يسرى غير متوفرة في السوق ، خيط خاص (فقط لديك رسم أو عينة) المواد: كربيد ، HSSe ، AISI M42 ، JIS SKH59 DIN 1.3343 ، SKH-9
الحنفيات ، الصنابير الحلزونية حنفية الخيط اليسرى ، حنفية يدوية ، حنفية آلة ، حنفية آلة ، حنفية ملولبة ، وصلة نحاسية تركيبات ملولبة من النحاس خيط داخلي ، خيط خارجي ، خيط بوصة ، خيط مائل مدبب حنفية خيوط لربط الوصلات النحاسية
ดอกต๊าปเกลียว (Tapping) หรือ ดอกต๊าป เป็นอุปกรณ์ที่ใช้สำหรับการสร้างเกลียวให้กับชิ้นงานด้วยกระบวนการต๊าป โดยการตัดเกลียวในภายในรูของชิ้นงาน ซึ่งจัดอยู่ในกลุ่มของเครื่องมือตัด ทำจากเหล็กกล้า หรือคาร์ไบด์นอกจากนี้ยังใช้ในการแปรรูปโลหะต่างๆ การสร้างเกลียวในชิ้นงานนั้นสามารถทำได้ทั้งการต๊าปเกลียวด้วยมือ และการต๊าปเกลียวด้วยเครื่องจักร ซึ่งเกลียวที่เกิดจากการต๊าปนั้นมีทั้งเกลียวใน และเกลียวนอก
รูปแบบและวิธีการเลือกดอกต๊าปเกลียว
1. ดอกต๊าปร่องตรง (Straight Flute Tap)
ดอกต๊าปเกลียวชนิดนี้ นิยมใช้กันอย่างแพร่หลาย และเป็นแบบมาตรฐานในการสร้างเกลียวให้กับชิ้นงาน ลักษณะของดอกต๊าปเกลียวชนิดนี้จะมีสองด้าน ด้านยาวใช้สำหรับเจาะรูทะลุ ส่วนด้านสั้นใช้สำหรับเจาะรูตัน ในส่วนนี้จะมีข้อเสียคือจะมีเศษติดอยู่ในร่องเกลียว ทำให้ต้องเป่าเอาเศษฝุ่นออก ดอกต๊าปเกลียวนี้ทำจากวัสดุที่มีความแข็งแรงสูง เช่น เหล็กกล้าความเร็วสูง และซีเมนต์คาร์ไบด์ มักจะเห็นดอกต๊าปชนิดนี้ในการผลิตขนาดเล็ก
2. ดอกต๊าปร่องเกลียว (Spiral Flute Tap)
ดอกต๊าปเกลียวชนิดนี้มีการออกแบบให้ระหว่างแต่ละเกลียวตัดมีร่องระบายเศษ เพื่อที่ในขั้นตอนในการทำการต๊าปเศษของวัสดุจะถูกดันกลับออกมาตามร่อง ช่วยยืดอายุการใช้งานให้นานขึ้น นอกจากนี้ดอกต๊าปเกลียวมีองศาที่ต่างกันเพื่อให้เหมาะสมกับความเร็วรอบในการใช้งาน ซึ่งจะแบ่งเป็น ความเร็วต่ำมุมเกลียวจะอยู่ที่ 18-30 องศา และความเร็วสูงมุมเกลียวจะอยู่ที่ 45-52 องศา แต่ละมุมก็จะเหมาะกับวัสดุที่แตกต่างกันไป เช่น
มุมเกลียวจะอยู่ที่ 45 องศาหรือมากกว่า : เหมาะกับวัสดุที่มีความอ่อนตัว เช่น อลูมิเนียม หรือทองแดง
มุมเกลียวที่ 25-35 องศา : เหมาะกับโลหะผสม ที่มีความเปราะแตกง่าย
มุมเกลียวที่ 05-20 องศา : เหมาะกับวัสดุที่แข็งมากหรือเหนียวมาก เช่น สแตนเลสบางชนิด ไทเทเนียม หรือ โลหะผสมนิกเกิล
3. ดอกต๊าปปลายร่องเฉียง (Spiral Point Tap)
ดอกต๊าปชนิดนี้มีลักษณะคล้ายกับดอกต๊าปเกลียวร่องตรง แต่มีความพิเศษที่ส่วนปลายของดอกจะมีร่องที่ช่วยในการดันเศษวัสดุไปด้านหน้าทำให้เศษไม่ติดอยู่ในรูที่ทำการต๊าป เหมาะสำหรับการทำเกลียวแบบรูทะลุหรืองานที่ต้องการความเร็วในการต๊าปสูง
4. ดอกต๊าปมือ (Hand Tap)
เป็นดอกต๊าปเกลียวที่นิยมใช้กันพื้นฐาน เหมาะกับการทำเกลียวด้วยตัวเอง หรือด้วยมือ ผลิตจากเหล็กกล้าผสมคาร์บอน หรือเหล็กกล้าความเร็วรอบสูง มีความแข็งมากเหมาะกับการใช้ทำเกลียวกับวัสดุที่มีความแข็ง มีอยู่ด้วยกัน 3 ชนิด คือ
ตัวเรียว (Taper Tap) : สำหรับใช้ในการตัดเกลียวในวัสดุที่มีความแข็งมาก เช่น Alloy และชิ้นงานที่ต้องการเกลียวขนาดเล็กซึ่งมีโอกาสสูงที่จะแตกหัก
ตัวตาม (Plug Tap) : ลักษณะดอกต๊าปเกลียวจะคล้ายกับ ตัวเรียว (Taper Tap) แต่จะมีความยาวของช่วงที่เรียวน้อยกว่า เหมาะกับงานที่เป็นรูเจาะทะลุ หรือรูตัด
ตัวสุดท้าย (Bottoming Tap) : ลักษณะดอกต๊าปเกลียวนี้คือจะมีปลายเรียวเล็กน้อยเท่านั้น เพื่อช่วยให้เข้าไปในชิ้นงานตอนเริ่มต้นต๊าปเกลียวเท่านั้น เหมาะสำหรับรูที่ผ่านการต๊าปชนิดอื่นนำร่องมาก่อน ใช้ในการสร้างรูทะลุ และไม่ทะลุ
ดอกต๊าปเกลียวชนิดนี้ ถูกออกแบบมาให้มีความแตกต่างจากชนิดอื่น คือ จะสร้างเกลียวด้วยการรีด หรืออัดขึ้นรูปวัสดุภายในรู ในกระบวนการทำงานของดอกต๊าปชนิดนี้นั้นจะไม่มีเศษเกิดขึ้น เพราะเศษจะถูกอัดเข้าไปในเนื้อชิ้นงาน เหมาะกับการสร้างเกลียวให้กับวัสดุประเภทที่ไม่มีความแข็งมาก จึงเหมาะกับวัสดุ เช่น เหล็กคาร์บอนต่ำ หรืออลูมิเนียม
การเลือกดอกต๊าปที่เหมาะสม ดอกต๊าป (Tap) เป็นเครื่องมือที่ทำหน้าที่ตัดเฉือนหรือรีดเกลียวที่รูเจาะ ชิ้นส่วนที่มีรูเกลียวจะถูกนำไปประกอบเข้าด้วยกันกับชิ้นส่วนที่มีสลักเกลียว (Bolt) หรือเกลียวนอก การทำรูเกลียวเริ่มจากการเจาะรูที่มีขนาดเล็กกว่าความยาวเส้นผ่านศูนย์กลางนอก (Outer diameter) ของขนาดเกลียวที่ต้องการ จากนั้นใช้ดอกต๊าปในการขึ้นรูปเกลียว เราจะเรียกรูที่ผ่านการทำเกลียวนี้ว่า “เกลียวใน” การต๊าปเกลียวสามารถทำได้ทั้งแบบ Manual, แบบกึ่ง Manual และแบบอัตโนมัติ

ดอกต๊าปมีหลายประเภท แต่ละประเภทจะเหมาะกับการใช้งานและวัสดุที่แตกต่างกันไป การเข้าใจดอกต๊าปแต่ละประเภท จะทำให้สามารถเลือกใช้ได้อย่างเหมาะสม ได้ขนาดรูเกลียวที่ได้มาตรฐาน ใช้เวลาในการทำงานสั้น ได้ต้นทุนในการทำเกลียวต่ำที่สุด และดอกต๊าปมีอายุการใช้งานยาวนาน
ดอกต๊าปที่ใช้งานกันอยู่ทั่วไปในปัจจุบัน สามารถแบ่งได้ 5 ประเภท ดังนี้
1. ดอกต๊าปร่องตรง (Straight Flute Tap)

ดอกต๊าปร่องตรง สามารถทำได้ทั้งเกลียวแบบรูตันและแบบรูทะลุ เหมาะกับวัสดุชิ้นงานเหล็กหล่อหรือวัสดุที่มีเศษสั้น แต่มีข้อจำกัดคือ กรณีทำเกลียวแบบรูตัน เศษจากการตัดจะอยู่ภายในรูเกลียวไม่สามารถระบายออกสู่ภายนอกได้ ในระหว่างการตัดเกลียวจึงต้องคอยเป่าไล่เศษวัสดุออกภายนอก มิฉะนั้นดอกต๊าปอาจจะหักคาติดอยู่กับชิ้นงานในขณะทำเกลียวได้
2. ดอกต๊าปร่องเลื้อย (Spiral Tap)

ดอกต๊าปร่องเลื้อย เหมาะสำหรับการทำเกลียวแบบรูตัน เนื่องจากมีร่องเลื้อยทำหน้าที่ในการระบายเศษ โดยในขณะทำเกลียวเศษของวัสดุจะถูกดันกลับออกมาตามร่องและย้อนขึ้นมาทางปากรู ดอกต๊าปชนิดนี้เหมาะสำหรับการใช้งานกับวัสดุกลุ่มเหล็กเหนียวหรือวัสดุที่มีเศษยาว
3. ดอกต๊าปปลายร่องเฉียง (Spiral Point Tap)

ดอกต๊าปปลายร่องเฉียง เหมาะกับการทำเกลียวแบบรูทะลุหรืองานที่ต้องการความเร็วในการต๊าปสูงๆ จะมีลักษณะคล้ายกับดอกต๊าปแบบร่องตรง แต่มีความพิเศษตรงที่บริเวณปลายของดอกจะมีร่องที่ช่วยในการดันเศษวัสดุไปด้านหน้าและไหลออกสู่ภายนอกที่ด้านล่างของรูเจาะ ทำให้เศษไม่ติดอยู่ในรูที่ทำการต๊าป
4. ดอกต๊าปมือ (Hand Tap)

ดอกต๊าปมือ เป็นดอกต๊าปพื้นฐานที่นิยมใช้งานกัน สำหรับการทำเกลียวแบบ Manual หรือการต๊าปเกลียวด้วยมือ ดอกต๊าปชนิดนี้จะมี 3 ดอก โดยมีการทำงานดังนี้
- ดอกแรกตัวเรียว (Taper Tap) เป็นตัวทำเกลียวตัวแรก โดยส่วนปลายเกลียวจะมีความเรียว (Chamfer length) อยู่ประมาณ 6-7 ฟัน ก่อนที่ฟันเกลียวจะเต็มรูปร่าง
- ดอกตาม (Plug Tap) เป็นดอกต๊าปตัวที่สอง เพื่อสร้างเกลียวให้มีขนาดที่ใกล้เคียงกับที่ต้องการ ดอกตามตัวนี้สามารถใช้แทนเกลียวดอกแรกได้เลยหากวัสดุที่ต้องการทำเกลียวนั้นไม่แข็งมากเกินไป ปลายเกลียวมีความเรียว (Chamfer length) อยู่ที่ 3-4 ฟัน
- ดอกสุดท้าย (Bottoming Tap) ดอกต๊าปเกลียวตัวนี้ส่วนของเกลียวแทบจะไม่มีส่วนที่เรียวเลย จึงใช้เป็นตัวสุดท้ายเพื่อทำเกลียวให้สมบูรณ์
5. ดอกต๊าปรีดเกลียว (Forming Tap)
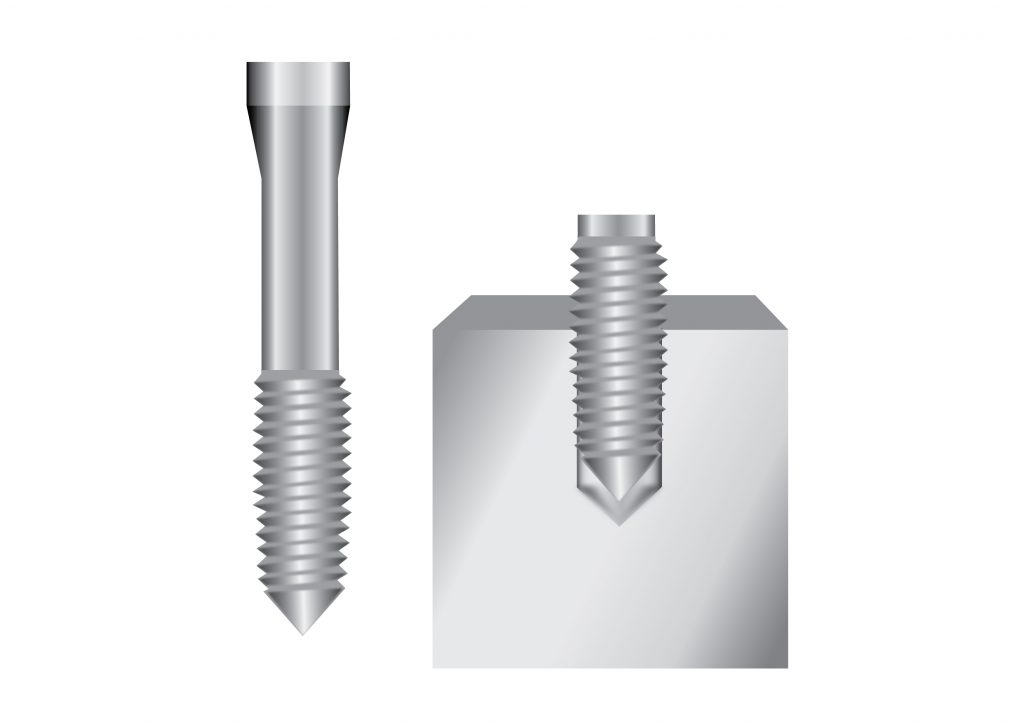
ดอกต๊าปรีดเกลียว จะสร้างเกลียวด้วยการรีดหรืออัดขึ้นรูปวัสดุภายในรู ซึ่งจะแตกต่างจากดอกต๊าปชนิดอื่นๆที่ขึ้นรูปด้วยการตัดเฉือน ทำให้การทำเกลียวด้วยดอกต๊าปนี้ไม่มีเศษเกิดขึ้นเลย เนื่องจากเศษถูกอัดเข้าไปในเนื้อเกลียว นอกจากข้อดีในเรื่องที่ไม่มีเศษแล้ว ยังทำให้เกลียวมีความแข็งแรงขึ้นอีกด้วย ดอกต๊าปรีดเกลียวเหมาะกับการทำเกลียวในวัสดุประเภทที่ไม่แข็งมาก เช่น เหล็กคาร์บอนต่ำ หรืออลูมิเนียม

ดอกต๊าปเกลียวคืออะไร
ดอกต๊าปเกลียว (Tapping) หรือ ดอกต๊าป เป็นอุปกรณ์ที่ใช้สำหรับการสร้างเกลียวให้กับชิ้นงานด้วยกระบวนการต๊าป โดยการตัดเกลียวในภายในรูของชิ้นงาน ซึ่งจัดอยู่ในกลุ่มของเครื่องมือตัด ทำจากเหล็กกล้า หรือคาร์ไบด์นอกจากนี้ยังใช้ในการแปรรูปโลหะต่างๆ การสร้างเกลียวในชิ้นงานนั้นสามารถทำได้ทั้งการต๊าปเกลียวด้วยมือ และการต๊าปเกลียวด้วยเครื่องจักร ซึ่งเกลียวที่เกิดจากการต๊าปนั้นมีทั้งเกลียวใน และเกลียวนอก
รูปแบบและวิธีการเลือกดอกต๊าปเกลียว
1. ดอกต๊าปร่องตรง (Straight Flute Tap)
ดอกต๊าปเกลียวชนิดนี้ นิยมใช้กันอย่างแพร่หลาย และเป็นแบบมาตรฐานในการสร้างเกลียวให้กับชิ้นงาน ลักษณะของดอกต๊าปเกลียวชนิดนี้จะมีสองด้าน ด้านยาวใช้สำหรับเจาะรูทะลุ ส่วนด้านสั้นใช้สำหรับเจาะรูตัน ในส่วนนี้จะมีข้อเสียคือจะมีเศษติดอยู่ในร่องเกลียว ทำให้ต้องเป่าเอาเศษฝุ่นออก ดอกต๊าปเกลียวนี้ทำจากวัสดุที่มีความแข็งแรงสูง เช่น เหล็กกล้าความเร็วสูง และซีเมนต์คาร์ไบด์ มักจะเห็นดอกต๊าปชนิดนี้ในการผลิตขนาดเล็ก
2. ดอกต๊าปร่องเกลียว (Spiral Flute Tap)
ดอกต๊าปเกลียวชนิดนี้มีการออกแบบให้ระหว่างแต่ละเกลียวตัดมีร่องระบายเศษ เพื่อที่ในขั้นตอนในการทำการต๊าปเศษของวัสดุจะถูกดันกลับออกมาตามร่อง ช่วยยืดอายุการใช้งานให้นานขึ้น นอกจากนี้ดอกต๊าปเกลียวมีองศาที่ต่างกันเพื่อให้เหมาะสมกับความเร็วรอบในการใช้งาน ซึ่งจะแบ่งเป็น ความเร็วต่ำมุมเกลียวจะอยู่ที่ 18-30 องศา และความเร็วสูงมุมเกลียวจะอยู่ที่ 45-52 องศา แต่ละมุมก็จะเหมาะกับวัสดุที่แตกต่างกันไป เช่น
มุมเกลียวจะอยู่ที่ 45 องศาหรือมากกว่า : เหมาะกับวัสดุที่มีความอ่อนตัว เช่น อลูมิเนียม หรือทองแดง
มุมเกลียวที่ 25-35 องศา : เหมาะกับโลหะผสม ที่มีความเปราะแตกง่าย
มุมเกลียวที่ 05-20 องศา : เหมาะกับวัสดุที่แข็งมากหรือเหนียวมาก เช่น สแตนเลสบางชนิด ไทเทเนียม หรือ โลหะผสมนิกเกิล
3. ดอกต๊าปปลายร่องเฉียง (Spiral Point Tap)
ดอกต๊าปชนิดนี้มีลักษณะคล้ายกับดอกต๊าปเกลียวร่องตรง แต่มีความพิเศษที่ส่วนปลายของดอกจะมีร่องที่ช่วยในการดันเศษวัสดุไปด้านหน้าทำให้เศษไม่ติดอยู่ในรูที่ทำการต๊าป เหมาะสำหรับการทำเกลียวแบบรูทะลุหรืองานที่ต้องการความเร็วในการต๊าปสูง
4. ดอกต๊าปมือ (Hand Tap)
เป็นดอกต๊าปเกลียวที่นิยมใช้กันพื้นฐาน เหมาะกับการทำเกลียวด้วยตัวเอง หรือด้วยมือ ผลิตจากเหล็กกล้าผสมคาร์บอน หรือเหล็กกล้าความเร็วรอบสูง มีความแข็งมากเหมาะกับการใช้ทำเกลียวกับวัสดุที่มีความแข็ง มีอยู่ด้วยกัน 3 ชนิด คือ
ตัวเรียว (Taper Tap) : สำหรับใช้ในการตัดเกลียวในวัสดุที่มีความแข็งมาก เช่น Alloy และชิ้นงานที่ต้องการเกลียวขนาดเล็กซึ่งมีโอกาสสูงที่จะแตกหัก
ตัวตาม (Plug Tap) : ลักษณะดอกต๊าปเกลียวจะคล้ายกับ ตัวเรียว (Taper Tap) แต่จะมีความยาวของช่วงที่เรียวน้อยกว่า เหมาะกับงานที่เป็นรูเจาะทะลุ หรือรูตัด
ตัวสุดท้าย (Bottoming Tap) : ลักษณะดอกต๊าปเกลียวนี้คือจะมีปลายเรียวเล็กน้อยเท่านั้น เพื่อช่วยให้เข้าไปในชิ้นงานตอนเริ่มต้นต๊าปเกลียวเท่านั้น เหมาะสำหรับรูที่ผ่านการต๊าปชนิดอื่นนำร่องมาก่อน ใช้ในการสร้างรูทะลุ และไม่ทะลุ
5. ดอกต๊าปรีดเกลียว (Forming Tap)
ดอกต๊าปเกลียวชนิดนี้ ถูกออกแบบมาให้มีความแตกต่างจากชนิดอื่น คือ จะสร้างเกลียวด้วยการรีด หรืออัดขึ้นรูปวัสดุภายในรู ในกระบวนการทำงานของดอกต๊าปชนิดนี้นั้นจะไม่มีเศษเกิดขึ้น เพราะเศษจะถูกอัดเข้าไปในเนื้อชิ้นงาน เหมาะกับการสร้างเกลียวให้กับวัสดุประเภทที่ไม่มีความแข็งมาก จึงเหมาะกับวัสดุ เช่น เหล็กคาร์บอนต่ำ หรืออลูมิเนียม
ขนาดของต๊าปเกลียว
การเตรียมชิ้นงานด้วยการต๊าปนั้นอาจจะมีข้อผิดพลาด ถ้าหากเตรียมรูที่ใหญ่เกินไปอาจทำให้เกลียวที่ได้มีฟันเกลียวที่ตื้น ส่งผลให้เกลียวที่ได้ไม่มีความแข็งแรง หรือหากเล็กเกินไป จะต้องใช้แรงบิดมากขึ้น เพื่อทำการต๊าปเกลียว ซึ่งอาจทำให้ดอกต๊าปเกลียวหักได้ ซึ่งจะหาขนาดของรูเจาะเกลียวแต่ละชนิดมีทั้งดูจากตารางของแคตตาล็อคสินค้าเอง หรือคำนวณโดยใช้สูตร ดังนี้
การคำนวณรูเจาะสำหรับ เกลียวเมตริก (Metric)
ขนาดของรูเจาะทำเกลียว = เส้นผ่านศูนย์กลางภายนอกของเกลียว – ระยะพิตซ์ (pitch)
การคำนวณรูเจาะสำหรับ เกลียวอเมริกัน (Unified National Coarse (UNC))
ขนาดของรูเจาะทำเกลียว = เส้นผ่านศูนย์กลางภายนอกของเกลียว – ระยะพิตซ์ (pitch) โดยระยะพิตซ์ (pitch) = (1/จำนวนเกลียวต่อนิ้ว)
การคำนวณรูเจาะสำหรับ เกลียวอังกฤษ British Standard Whitworth (BSW)
ขนาดของรูเจาะทำเกลียว = เส้นผ่านศูนย์กลางภายนอกของเกลียว – (2 x ความลึกของเกลียว) + (ระยะเผื่อ) โดยระยะเผื่อสามารถหาได้จาก 2 x ¼ x ความลึกเกลียว
ธนะพัฒน์ เลิศรัตนศักดิ์ดา (Thanapath Lertrattanasakda)
ดอกต๊าปเกลียวคืออะไร
ดอกต๊าปเกลียว (Tapping) หรือ ดอกต๊าป เป็นอุปกรณ์ที่ใช้สำหรับการสร้างเกลียวให้กับชิ้นงานด้วยกระบวนการต๊าป โดยการตัดเกลียวในภายในรูของชิ้นงาน ซึ่งจัดอยู่ในกลุ่มของเครื่องมือตัด ทำจากเหล็กกล้า หรือคาร์ไบด์นอกจากนี้ยังใช้ในการแปรรูปโลหะต่างๆ การสร้างเกลียวในชิ้นงานนั้นสามารถทำได้ทั้งการต๊าปเกลียวด้วยมือ และการต๊าปเกลียวด้วยเครื่องจักร ซึ่งเกลียวที่เกิดจากการต๊าปนั้นมีทั้งเกลียวใน และเกลียวนอก
รูปแบบและวิธีการเลือกดอกต๊าปเกลียว
1. ดอกต๊าปร่องตรง (Straight Flute Tap)
ดอกต๊าปเกลียวชนิดนี้ นิยมใช้กันอย่างแพร่หลาย และเป็นแบบมาตรฐานในการสร้างเกลียวให้กับชิ้นงาน ลักษณะของดอกต๊าปเกลียวชนิดนี้จะมีสองด้าน ด้านยาวใช้สำหรับเจาะรูทะลุ ส่วนด้านสั้นใช้สำหรับเจาะรูตัน ในส่วนนี้จะมีข้อเสียคือจะมีเศษติดอยู่ในร่องเกลียว ทำให้ต้องเป่าเอาเศษฝุ่นออก ดอกต๊าปเกลียวนี้ทำจากวัสดุที่มีความแข็งแรงสูง เช่น เหล็กกล้าความเร็วสูง และซีเมนต์คาร์ไบด์ มักจะเห็นดอกต๊าปชนิดนี้ในการผลิตขนาดเล็ก
2. ดอกต๊าปร่องเกลียว (Spiral Flute Tap)
ดอกต๊าปเกลียวชนิดนี้มีการออกแบบให้ระหว่างแต่ละเกลียวตัดมีร่องระบายเศษ เพื่อที่ในขั้นตอนในการทำการต๊าปเศษของวัสดุจะถูกดันกลับออกมาตามร่อง ช่วยยืดอายุการใช้งานให้นานขึ้น นอกจากนี้ดอกต๊าปเกลียวมีองศาที่ต่างกันเพื่อให้เหมาะสมกับความเร็วรอบในการใช้งาน ซึ่งจะแบ่งเป็น ความเร็วต่ำมุมเกลียวจะอยู่ที่ 18-30 องศา และความเร็วสูงมุมเกลียวจะอยู่ที่ 45-52 องศา แต่ละมุมก็จะเหมาะกับวัสดุที่แตกต่างกันไป เช่น
มุมเกลียวจะอยู่ที่ 45 องศาหรือมากกว่า : เหมาะกับวัสดุที่มีความอ่อนตัว เช่น อลูมิเนียม หรือทองแดง
มุมเกลียวที่ 25-35 องศา : เหมาะกับโลหะผสม ที่มีความเปราะแตกง่าย
มุมเกลียวที่ 05-20 องศา : เหมาะกับวัสดุที่แข็งมากหรือเหนียวมาก เช่น สแตนเลสบางชนิด ไทเทเนียม หรือ โลหะผสมนิกเกิล
3. ดอกต๊าปปลายร่องเฉียง (Spiral Point Tap)
ดอกต๊าปชนิดนี้มีลักษณะคล้ายกับดอกต๊าปเกลียวร่องตรง แต่มีความพิเศษที่ส่วนปลายของดอกจะมีร่องที่ช่วยในการดันเศษวัสดุไปด้านหน้าทำให้เศษไม่ติดอยู่ในรูที่ทำการต๊าป เหมาะสำหรับการทำเกลียวแบบรูทะลุหรืองานที่ต้องการความเร็วในการต๊าปสูง
4. ดอกต๊าปมือ (Hand Tap)
เป็นดอกต๊าปเกลียวที่นิยมใช้กันพื้นฐาน เหมาะกับการทำเกลียวด้วยตัวเอง หรือด้วยมือ ผลิตจากเหล็กกล้าผสมคาร์บอน หรือเหล็กกล้าความเร็วรอบสูง มีความแข็งมากเหมาะกับการใช้ทำเกลียวกับวัสดุที่มีความแข็ง มีอยู่ด้วยกัน 3 ชนิด คือ
ตัวเรียว (Taper Tap) : สำหรับใช้ในการตัดเกลียวในวัสดุที่มีความแข็งมาก เช่น Alloy และชิ้นงานที่ต้องการเกลียวขนาดเล็กซึ่งมีโอกาสสูงที่จะแตกหัก
ตัวตาม (Plug Tap) : ลักษณะดอกต๊าปเกลียวจะคล้ายกับ ตัวเรียว (Taper Tap) แต่จะมีความยาวของช่วงที่เรียวน้อยกว่า เหมาะกับงานที่เป็นรูเจาะทะลุ หรือรูตัด
ตัวสุดท้าย (Bottoming Tap) : ลักษณะดอกต๊าปเกลียวนี้คือจะมีปลายเรียวเล็กน้อยเท่านั้น เพื่อช่วยให้เข้าไปในชิ้นงานตอนเริ่มต้นต๊าปเกลียวเท่านั้น เหมาะสำหรับรูที่ผ่านการต๊าปชนิดอื่นนำร่องมาก่อน ใช้ในการสร้างรูทะลุ และไม่ทะลุ
5. ดอกต๊าปรีดเกลียว (Forming Tap)
ดอกต๊าปเกลียวชนิดนี้ ถูกออกแบบมาให้มีความแตกต่างจากชนิดอื่น คือ จะสร้างเกลียวด้วยการรีด หรืออัดขึ้นรูปวัสดุภายในรู ในกระบวนการทำงานของดอกต๊าปชนิดนี้นั้นจะไม่มีเศษเกิดขึ้น เพราะเศษจะถูกอัดเข้าไปในเนื้อชิ้นงาน เหมาะกับการสร้างเกลียวให้กับวัสดุประเภทที่ไม่มีความแข็งมาก จึงเหมาะกับวัสดุ เช่น เหล็กคาร์บอนต่ำ หรืออลูมิเนียม
ขนาดของต๊าปเกลียว
การเตรียมชิ้นงานด้วยการต๊าปนั้นอาจจะมีข้อผิดพลาด ถ้าหากเตรียมรูที่ใหญ่เกินไปอาจทำให้เกลียวที่ได้มีฟันเกลียวที่ตื้น ส่งผลให้เกลียวที่ได้ไม่มีความแข็งแรง หรือหากเล็กเกินไป จะต้องใช้แรงบิดมากขึ้น เพื่อทำการต๊าปเกลียว ซึ่งอาจทำให้ดอกต๊าปเกลียวหักได้ ซึ่งจะหาขนาดของรูเจาะเกลียวแต่ละชนิดมีทั้งดูจากตารางของแคตตาล็อคสินค้าเอง หรือคำนวณโดยใช้สูตร ดังนี้
การคำนวณรูเจาะสำหรับ เกลียวเมตริก (Metric)
ขนาดของรูเจาะทำเกลียว = เส้นผ่านศูนย์กลางภายนอกของเกลียว – ระยะพิตซ์ (pitch)
การคำนวณรูเจาะสำหรับ เกลียวอเมริกัน (Unified National Coarse (UNC))
ขนาดของรูเจาะทำเกลียว = เส้นผ่านศูนย์กลางภายนอกของเกลียว – ระยะพิตซ์ (pitch) โดยระยะพิตซ์ (pitch) = (1/จำนวนเกลียวต่อนิ้ว)
การคำนวณรูเจาะสำหรับ เกลียวอังกฤษ British Standard Whitworth (BSW)
ขนาดของรูเจาะทำเกลียว = เส้นผ่านศูนย์กลางภายนอกของเกลียว – (2 x ความลึกของเกลียว) + (ระยะเผื่อ) โดยระยะเผื่อสามารถหาได้จาก 2 x ¼ x ความลึกเกลียว
Carbide, HSSe, AISI M42, JIS SKH59 DIN 1.3343,SKH-9
taps, spiral taps Drill thread tap Spiral tap, hand tap, tap for solid tap, hand tap, machine tap, hi-speak tap, 3 taps, tap set, machine tap, tap HSS. ទុយោខ្សែដៃឆ្វេង, ម៉ាស៊ីនប៉ះដៃ, ម៉ាស៊ីនប៉ះម៉ាស៊ីន, ម៉ាស៊ីនម៉ាស៊ីន, ខ្សែស្ពាន់, ខ្សែស្ពាន់ដែលភ្ជាប់មកជាមួយខ្សែស្ពាន់ដែលសមនឹងខ្សែខាងក្នុង, ខ្សែស្រឡាយខាងក្រៅ, ខ្សែស្រឡាយអ៊ីញ, ខ្សែស្ពាន់កាត់កែង ខ្សែស្ពាន់សម្រាប់តោងសន្លាក់លង្ហិន ប្រដាប់ប៉ះសំរិទ្ធ
Paip lingkaran khas, dibuat mengikut tempahan, lingkaran luar, lingkaran besar, lingkaran aneh, pili lingkaran kiri Yang tidak terdapat di pasaran, benang khas (hanya ada lukisan atau sampel) Bahan : Karbida , HSSe, AISI M42, JIS SKH59 DIN 1.3343,SKH-9
ketik, ketik lingkaran Ketik benang gerudi Ketik lingkaran, ketik tangan, ketik untuk ketik padu, ketik tangan, ketik mesin, ketik hi-speak, 3 ketik, set ketik, ketik mesin, ketik HSS. ketuk benang sebelah kiri, ketuk tangan, ketuk mesin, ketuk mesin, ketuk berulir, ketuk berulir, sambungan loyang Pemasangan berulir tembaga Benang dalaman, benang luar, benang inci, benang tirus serong Ketuk benang untuk mengetuk sambungan loyang Ketuk Pemasangan Loyang
အထူးခရုပတ်ထိပုတ်ပါ၊ မှာကြားရန်ပြုလုပ်ထားသော၊ အပေါ်မှခရုပတ်၊ ကြီးမားသောခရုပတ်၊ ထူးဆန်းသောခရုပတ်၊ ဘယ်ဘက်ခရုပတ်ထိပုတ်ပါ ၎င်းသည် စျေးကွက်တွင်မရရှိနိုင်ပါ၊ အထူးချည်မျှင် (ပုံဆွဲသို့မဟုတ်နမူနာတစ်ခုသာရှိသည်) ပစ္စည်း : Carbide , HSSe , AISI M42 , JIS SKH59 DIN 1.3343၊SKH-9
နှိပ်ပါ၊ ခရုပတ်ခေါက်များ တူးထားသောချည်ကိုနှိပ်ပါ၊ ခရုကိုနှိပ်ပါ၊ လက်ကိုနှိပ်ပါ၊ အစိုင်အခဲကိုနှိပ်ပါ၊ လက်ကိုနှိပ်ပါ၊ စက်ကိုနှိပ်ပါ၊ Hi-speak ကိုနှိပ်ပါ၊ ၃ ချက်နှိပ်ပါ၊ သတ်မှတ်ကိုနှိပ်ပါ၊ စက်ကိုနှိပ်ပါ၊ HSS ကိုနှိပ်ပါ။ ဘယ်ဘက်အပ်ချည်၊ လက်နှိပ်၊ စက်ထိပုတ်ပါ၊ စက်ထိပုတ်ပါ၊ အပ်ချည်ကြိုးကိုနှိပ်ပါ၊ ကြေးဝါအဆစ် ကြေးဝါချည်မျှင်နှင့် အံဝင်ခွင်ကျဖြစ်သော အတွင်းချည်ကြိုး၊ ပြင်ပချည်၊ လက်မချည်၊ ထောင့်စွန်းသွယ်သွယ် ကြေးဝါအဆစ်များအတွက် ချည်မျှင်ထိပုတ်ပါ
ดอกต๊าปเกลียว (Tapping) หรือที่เรียกกันสั้นๆ ว่า “ดอกต๊าป” คืออุปกรณ์สำหรับสร้างรูเกลียวในวัสดุต่างๆ เพื่อเชื่อมต่อวัสดุที่ต้องการด้วยการหมุน
การเลือกดอกต๊าปที่เหมาะสม ดอกต๊าป (Tap) เป็นเครื่องมือที่ทำหน้าที่ตัดเฉือนหรือรีดเกลียวที่รูเจาะ ชิ้นส่วนที่มีรูเกลียวจะถูกนำไปประกอบเข้าด้วยกันกับชิ้นส่วนที่มีสลักเกลียว (Bolt) หรือเกลียวนอก การทำรูเกลียวเริ่มจากการเจาะรูที่มีขนาดเล็กกว่าความยาวเส้นผ่านศูนย์กลางนอก (Outer diameter) ของขนาดเกลียวที่ต้องการ จากนั้นใช้ดอกต๊าปในการขึ้นรูปเกลียว เราจะเรียกรูที่ผ่านการทำเกลียวนี้ว่า “เกลียวใน” การต๊าปเกลียวสามารถทำได้ทั้งแบบ Manual, แบบกึ่ง Manual และแบบอัตโนมัติ
ดอกต๊าปมีหลายประเภท แต่ละประเภทจะเหมาะกับการใช้งานและวัสดุที่แตกต่างกันไป การเข้าใจดอกต๊าปแต่ละประเภท จะทำให้สามารถเลือกใช้ได้อย่างเหมาะสม ได้ขนาดรูเกลียวที่ได้มาตรฐาน ใช้เวลาในการทำงานสั้น ได้ต้นทุนในการทำเกลียวต่ำที่สุด และดอกต๊าปมีอายุการใช้งานยาวนาน
ดอกต๊าปที่ใช้งานกันอยู่ทั่วไปในปัจจุบัน สามารถแบ่งได้ 5 ประเภท ดังนี้
1. ดอกต๊าปร่องตรง (Straight Flute Tap)
ดอกต๊าปร่องตรง สามารถทำได้ทั้งเกลียวแบบรูตันและแบบรูทะลุ เหมาะกับวัสดุชิ้นงานเหล็กหล่อหรือวัสดุที่มีเศษสั้น แต่มีข้อจำกัดคือ กรณีทำเกลียวแบบรูตัน เศษจากการตัดจะอยู่ภายในรูเกลียวไม่สามารถระบายออกสู่ภายนอกได้ ในระหว่างการตัดเกลียวจึงต้องคอยเป่าไล่เศษวัสดุออกภายนอก มิฉะนั้นดอกต๊าปอาจจะหักคาติดอยู่กับชิ้นงานในขณะทำเกลียวได้
2. ดอกต๊าปร่องเลื้อย (Spiral Tap)
ดอกต๊าปร่องเลื้อย เหมาะสำหรับการทำเกลียวแบบรูตัน เนื่องจากมีร่องเลื้อยทำหน้าที่ในการระบายเศษ โดยในขณะทำเกลียวเศษของวัสดุจะถูกดันกลับออกมาตามร่องและย้อนขึ้นมาทางปากรู ดอกต๊าปชนิดนี้เหมาะสำหรับการใช้งานกับวัสดุกลุ่มเหล็กเหนียวหรือวัสดุที่มีเศษยาว
3. ดอกต๊าปปลายร่องเฉียง (Spiral Point Tap)
ดอกต๊าปปลายร่องเฉียง เหมาะกับการทำเกลียวแบบรูทะลุหรืองานที่ต้องการความเร็วในการต๊าปสูงๆ จะมีลักษณะคล้ายกับดอกต๊าปแบบร่องตรง แต่มีความพิเศษตรงที่บริเวณปลายของดอกจะมีร่องที่ช่วยในการดันเศษวัสดุไปด้านหน้าและไหลออกสู่ภายนอกที่ด้านล่างของรูเจาะ ทำให้เศษไม่ติดอยู่ในรูที่ทำการต๊าป
4. ดอกต๊าปมือ (Hand Tap)
ดอกต๊าปมือ เป็นดอกต๊าปพื้นฐานที่นิยมใช้งานกัน สำหรับการทำเกลียวแบบ Manual หรือการต๊าปเกลียวด้วยมือ ดอกต๊าปชนิดนี้จะมี 3 ดอก โดยมีการทำงานดังนี้
- ดอกแรกตัวเรียว (Taper Tap) เป็นตัวทำเกลียวตัวแรก โดยส่วนปลายเกลียวจะมีความเรียว (Chamfer length) อยู่ประมาณ 6-7 ฟัน ก่อนที่ฟันเกลียวจะเต็มรูปร่าง
- ดอกตาม (Plug Tap) เป็นดอกต๊าปตัวที่สอง เพื่อสร้างเกลียวให้มีขนาดที่ใกล้เคียงกับที่ต้องการ ดอกตามตัวนี้สามารถใช้แทนเกลียวดอกแรกได้เลยหากวัสดุที่ต้องการทำเกลียวนั้นไม่แข็งมากเกินไป ปลายเกลียวมีความเรียว (Chamfer length) อยู่ที่ 3-4 ฟัน
- ดอกสุดท้าย (Bottoming Tap) ดอกต๊าปเกลียวตัวนี้ส่วนของเกลียวแทบจะไม่มีส่วนที่เรียวเลย จึงใช้เป็นตัวสุดท้ายเพื่อทำเกลียวให้สมบูรณ์
5. ดอกต๊าปรีดเกลียว (Forming Tap)
ดอกต๊าปรีดเกลียว จะสร้างเกลียวด้วยการรีดหรืออัดขึ้นรูปวัสดุภายในรู ซึ่งจะแตกต่างจากดอกต๊าปชนิดอื่นๆที่ขึ้นรูปด้วยการตัดเฉือน ทำให้การทำเกลียวด้วยดอกต๊าปนี้ไม่มีเศษเกิดขึ้นเลย เนื่องจากเศษถูกอัดเข้าไปในเนื้อเกลียว นอกจากข้อดีในเรื่องที่ไม่มีเศษแล้ว ยังทำให้เกลียวมีความแข็งแรงขึ้นอีกด้วย ดอกต๊าปรีดเกลียวเหมาะกับการทำเกลียวในวัสดุประเภทที่ไม่แข็งมาก เช่น เหล็กคาร์บอนต่ำ หรืออลูมิเนียม
ธนะพัฒน์ เลิศรัตนศักดิ์ดา (Thanapath Lertrattanasakda)